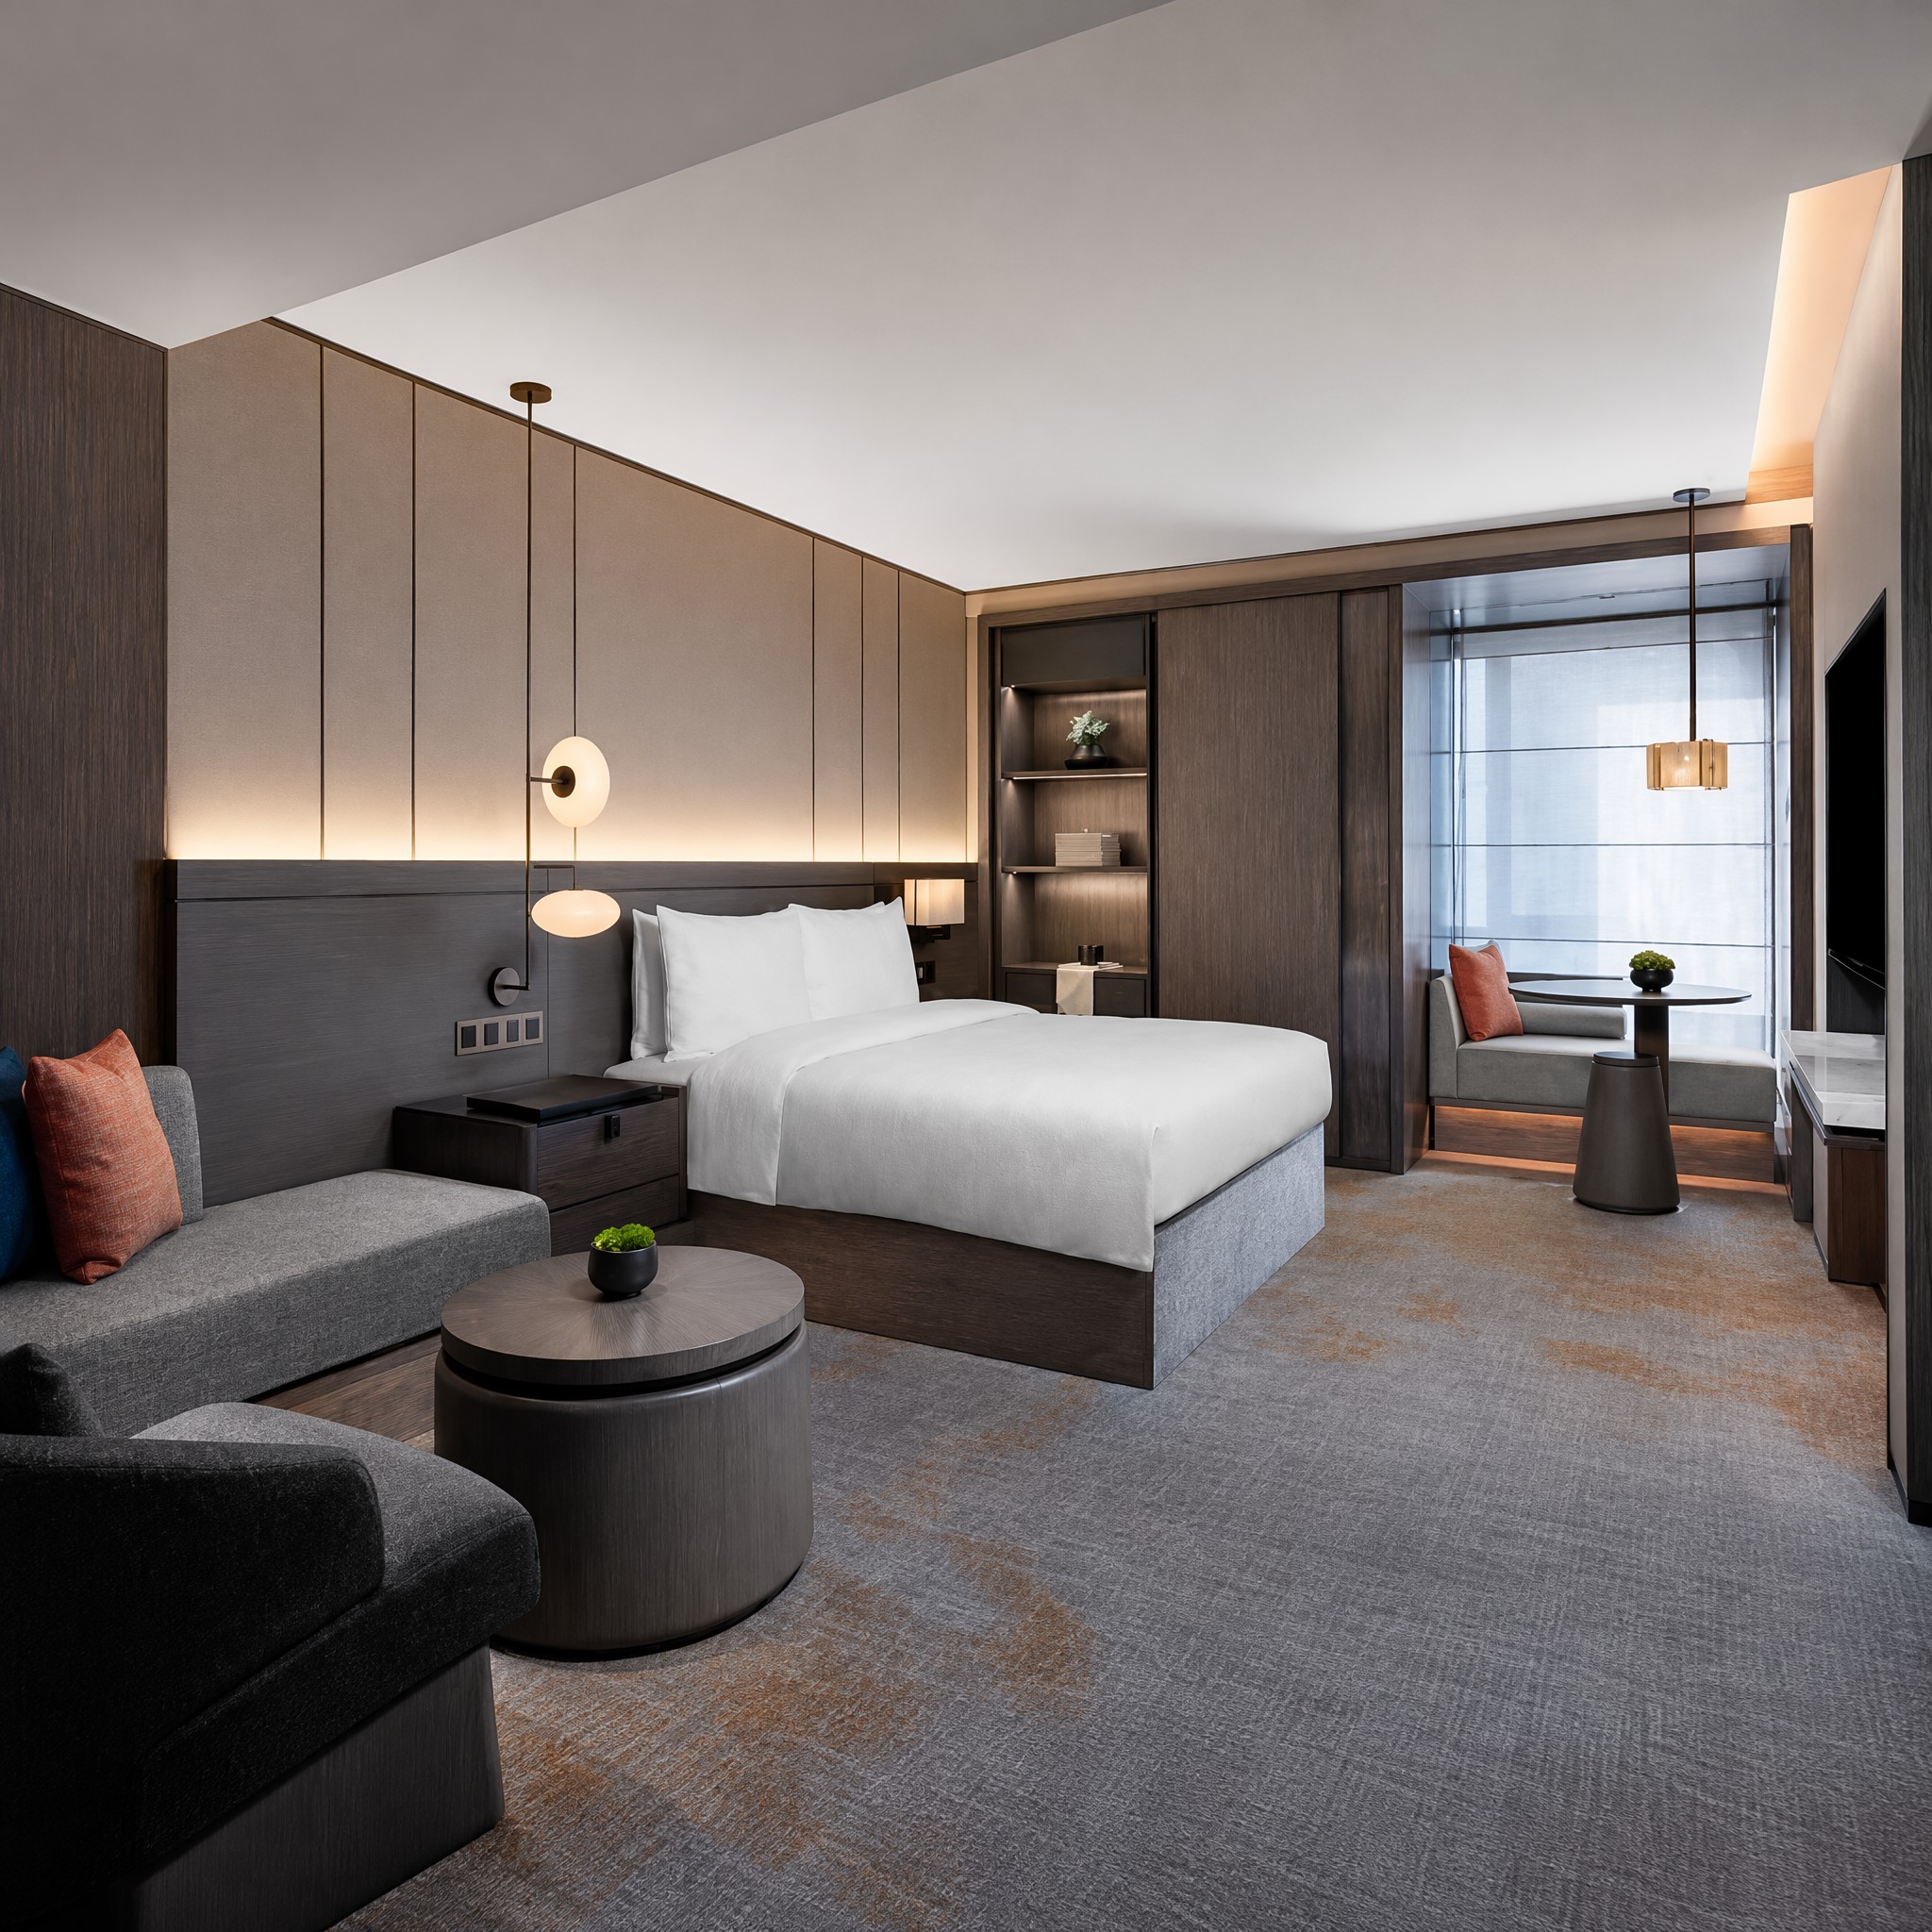
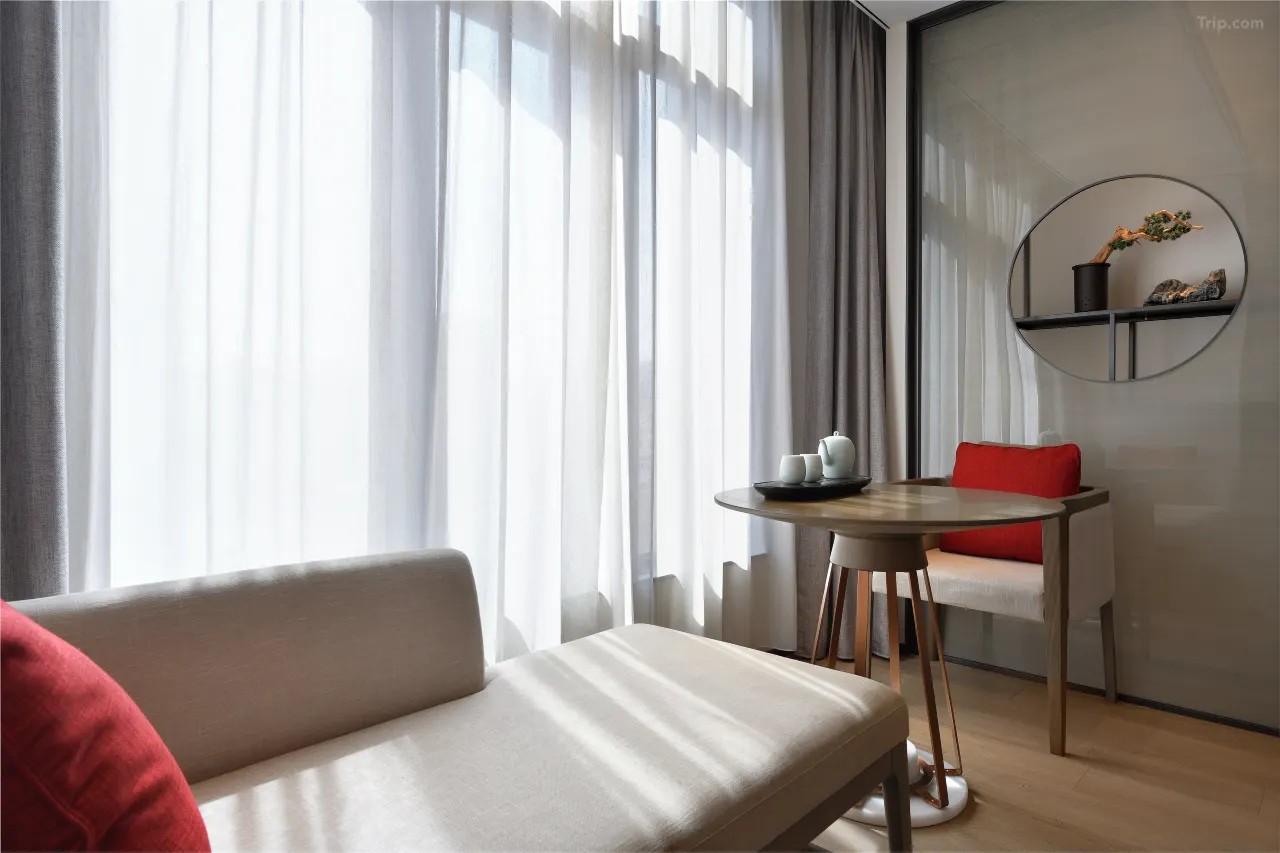
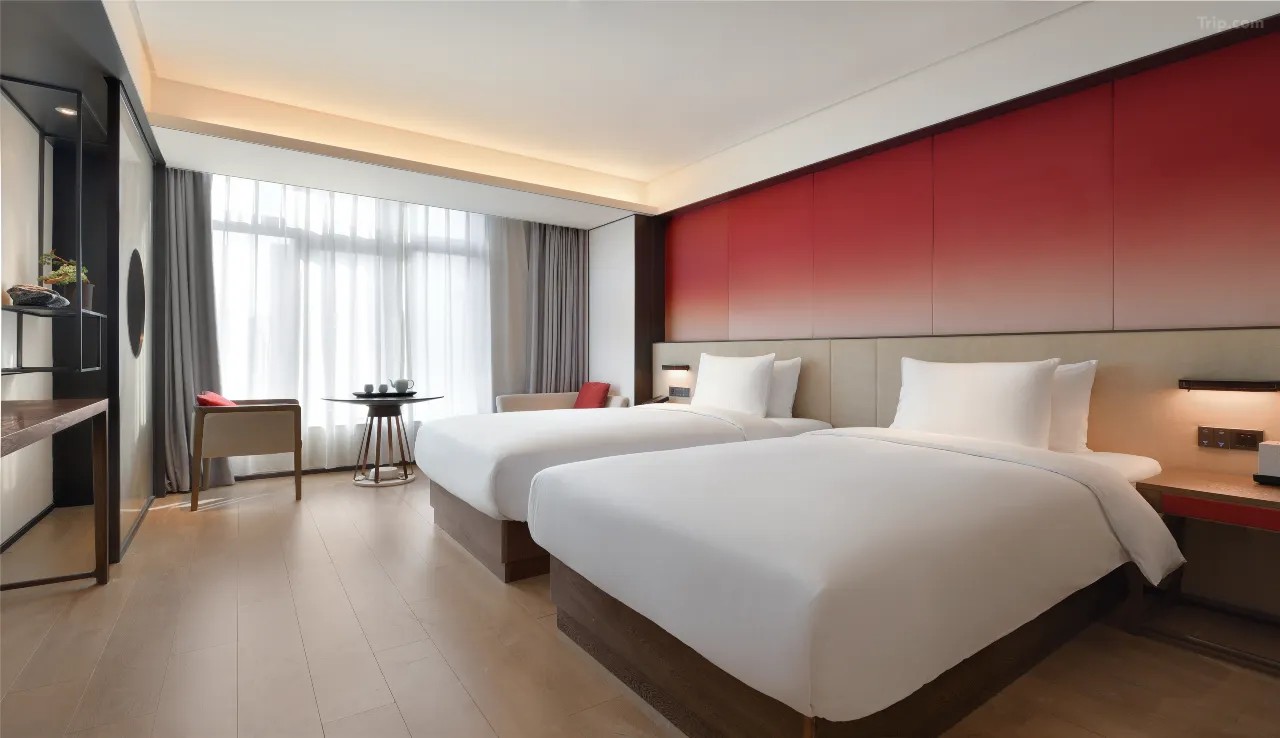
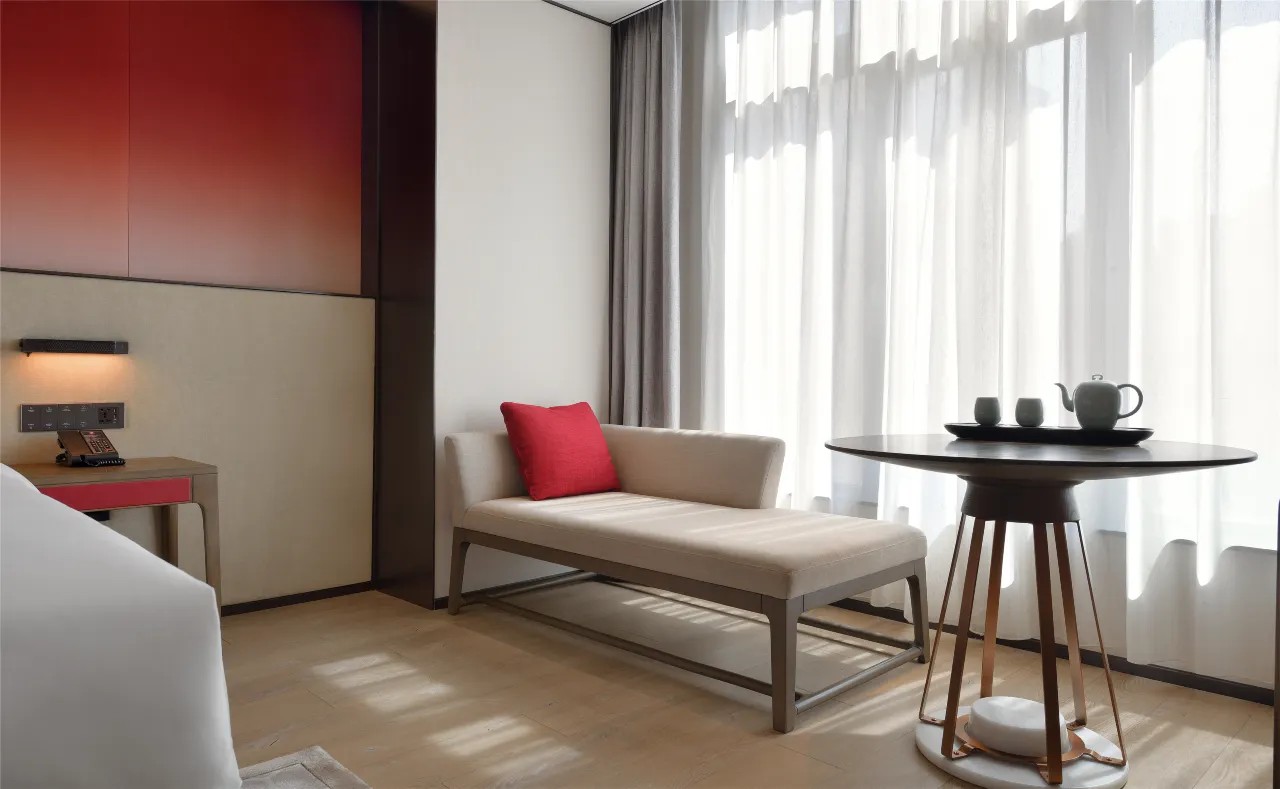
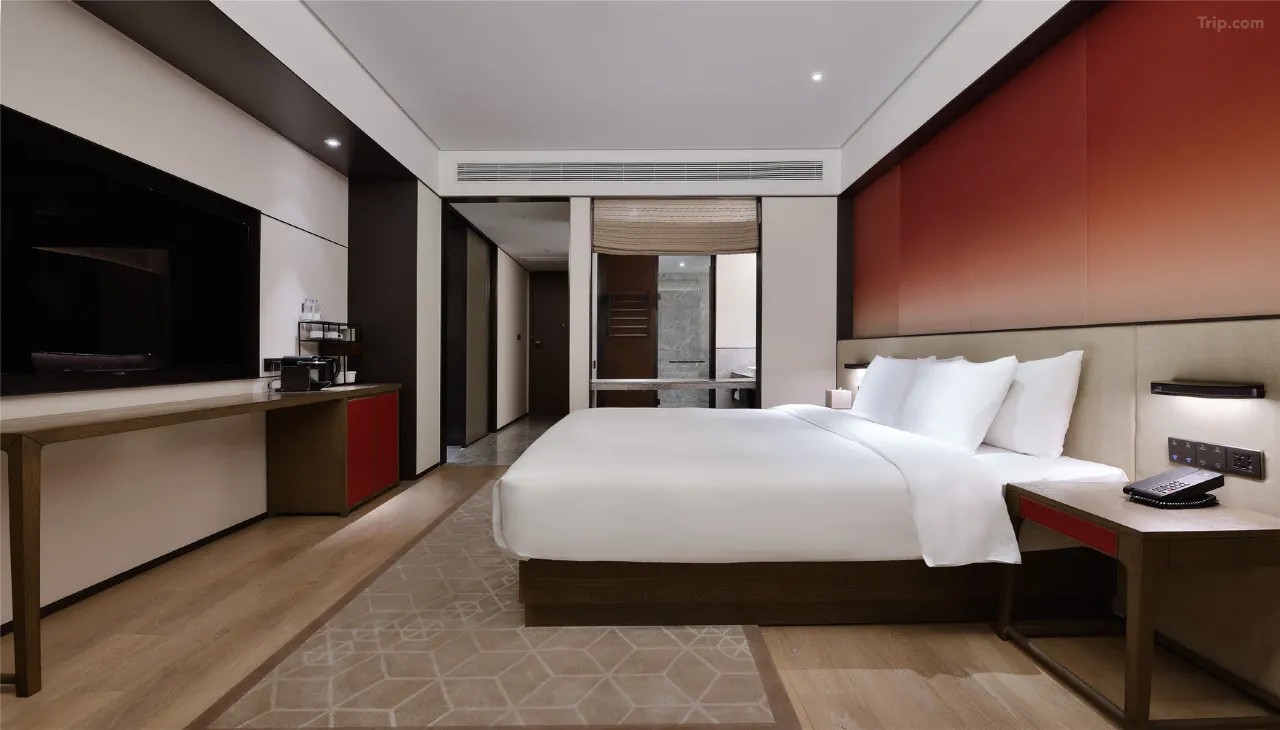
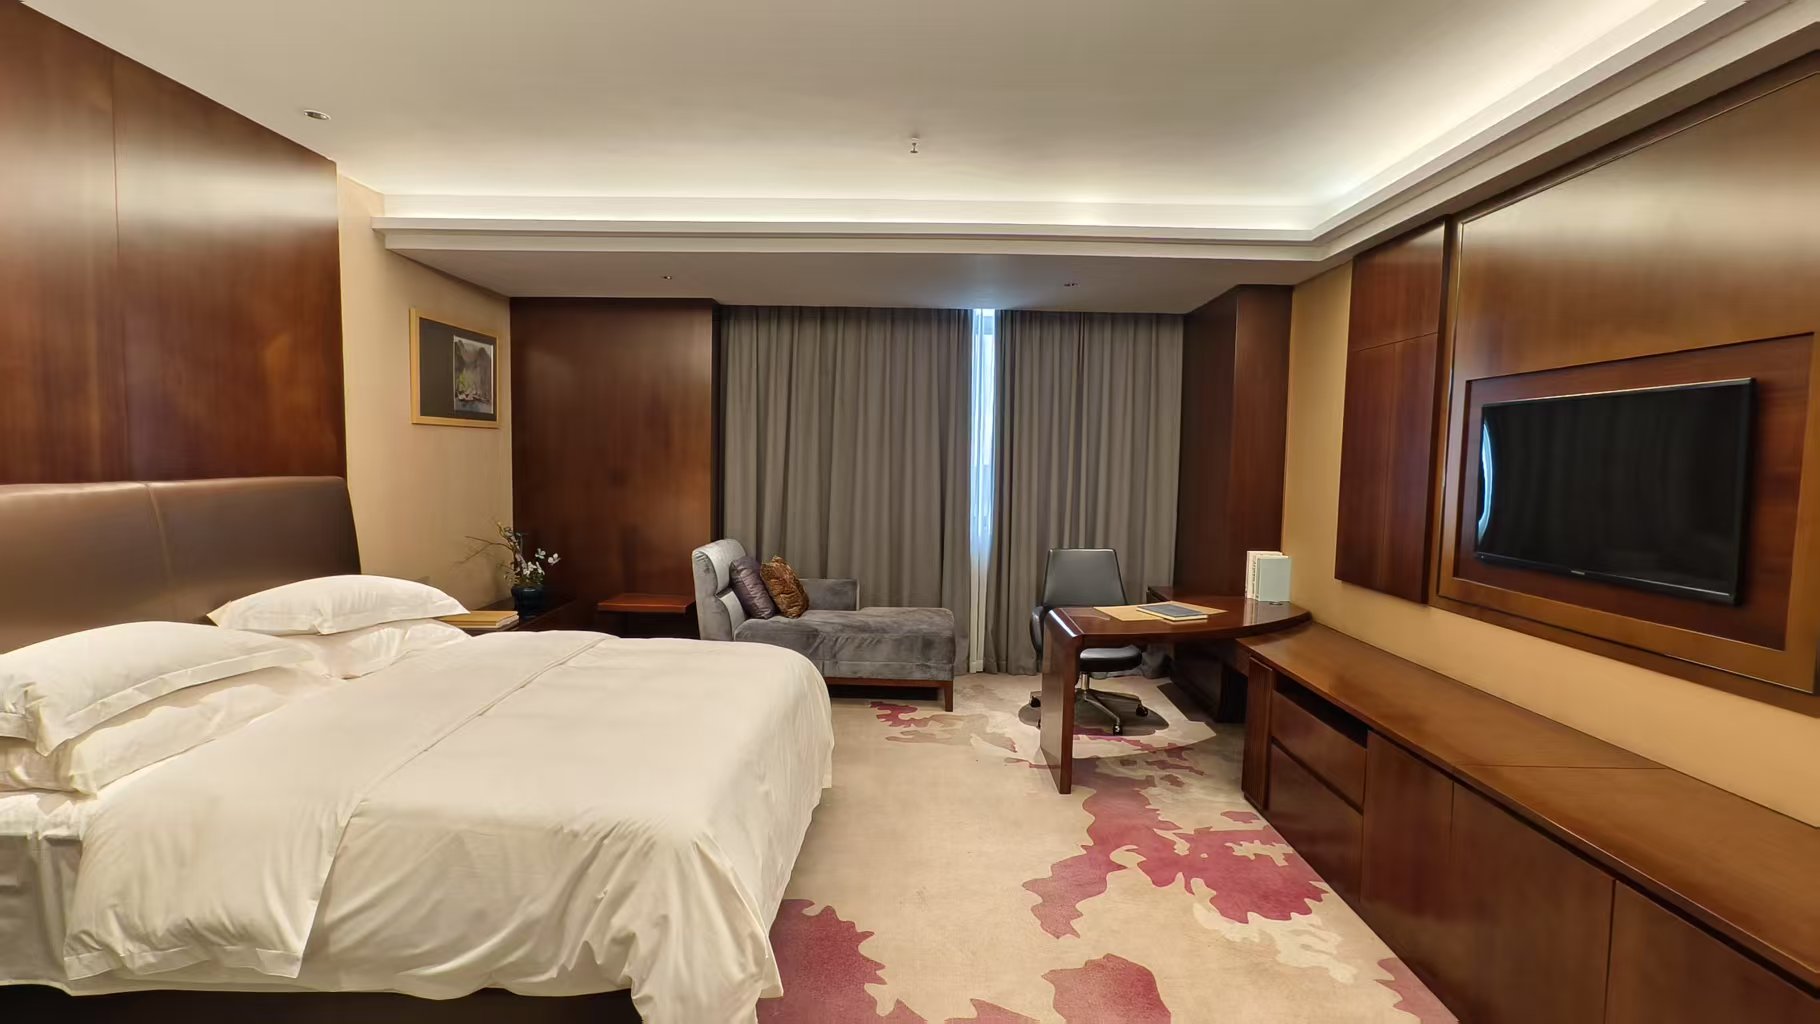
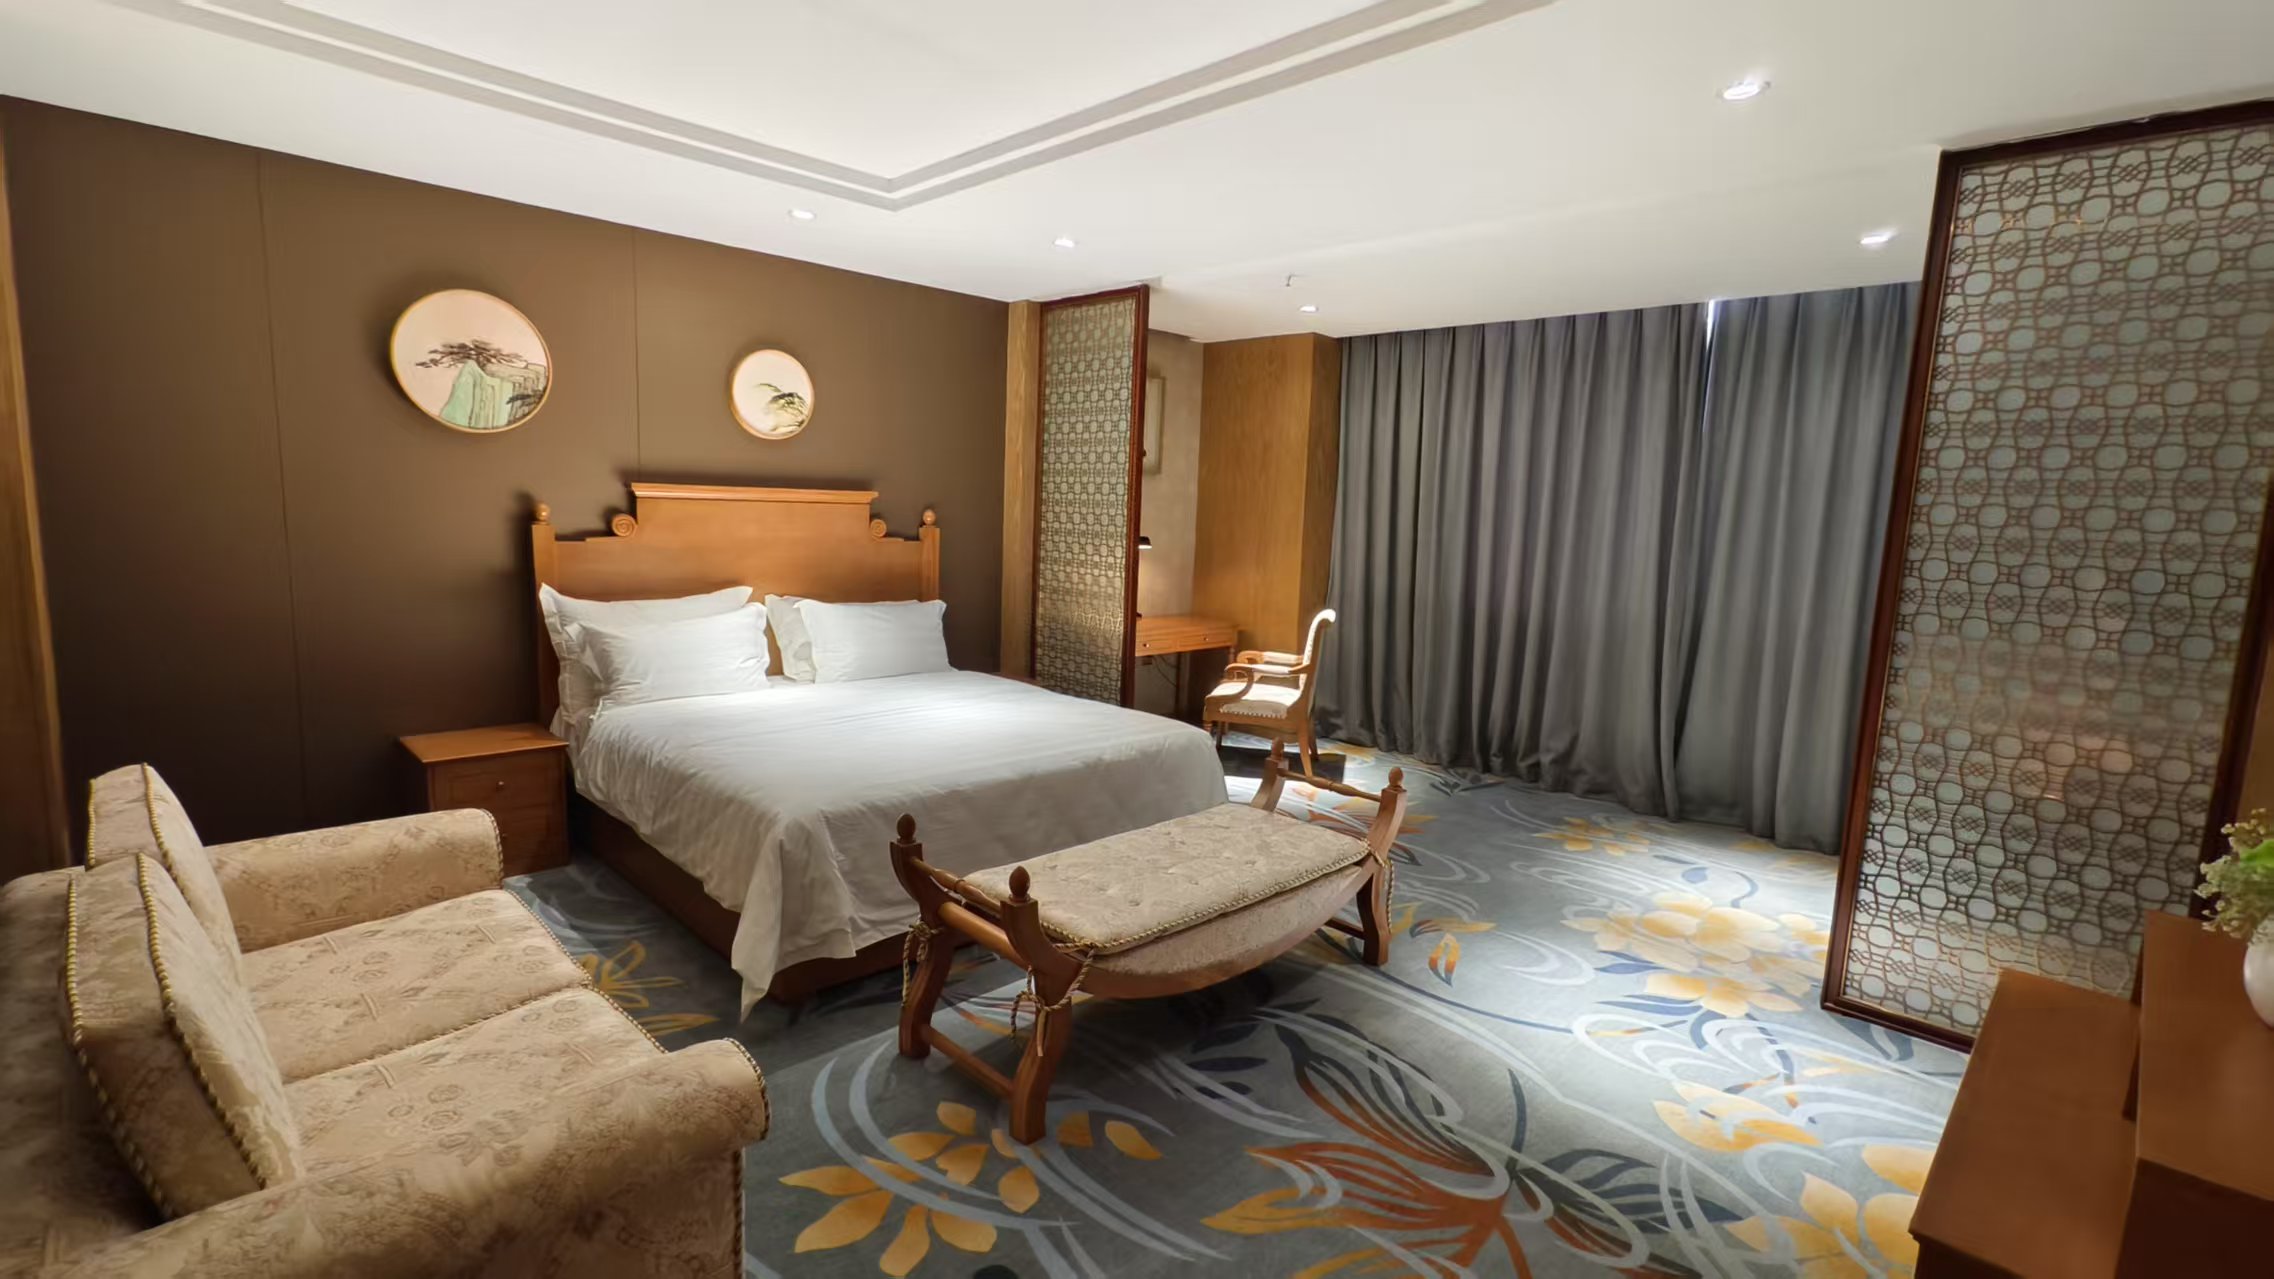
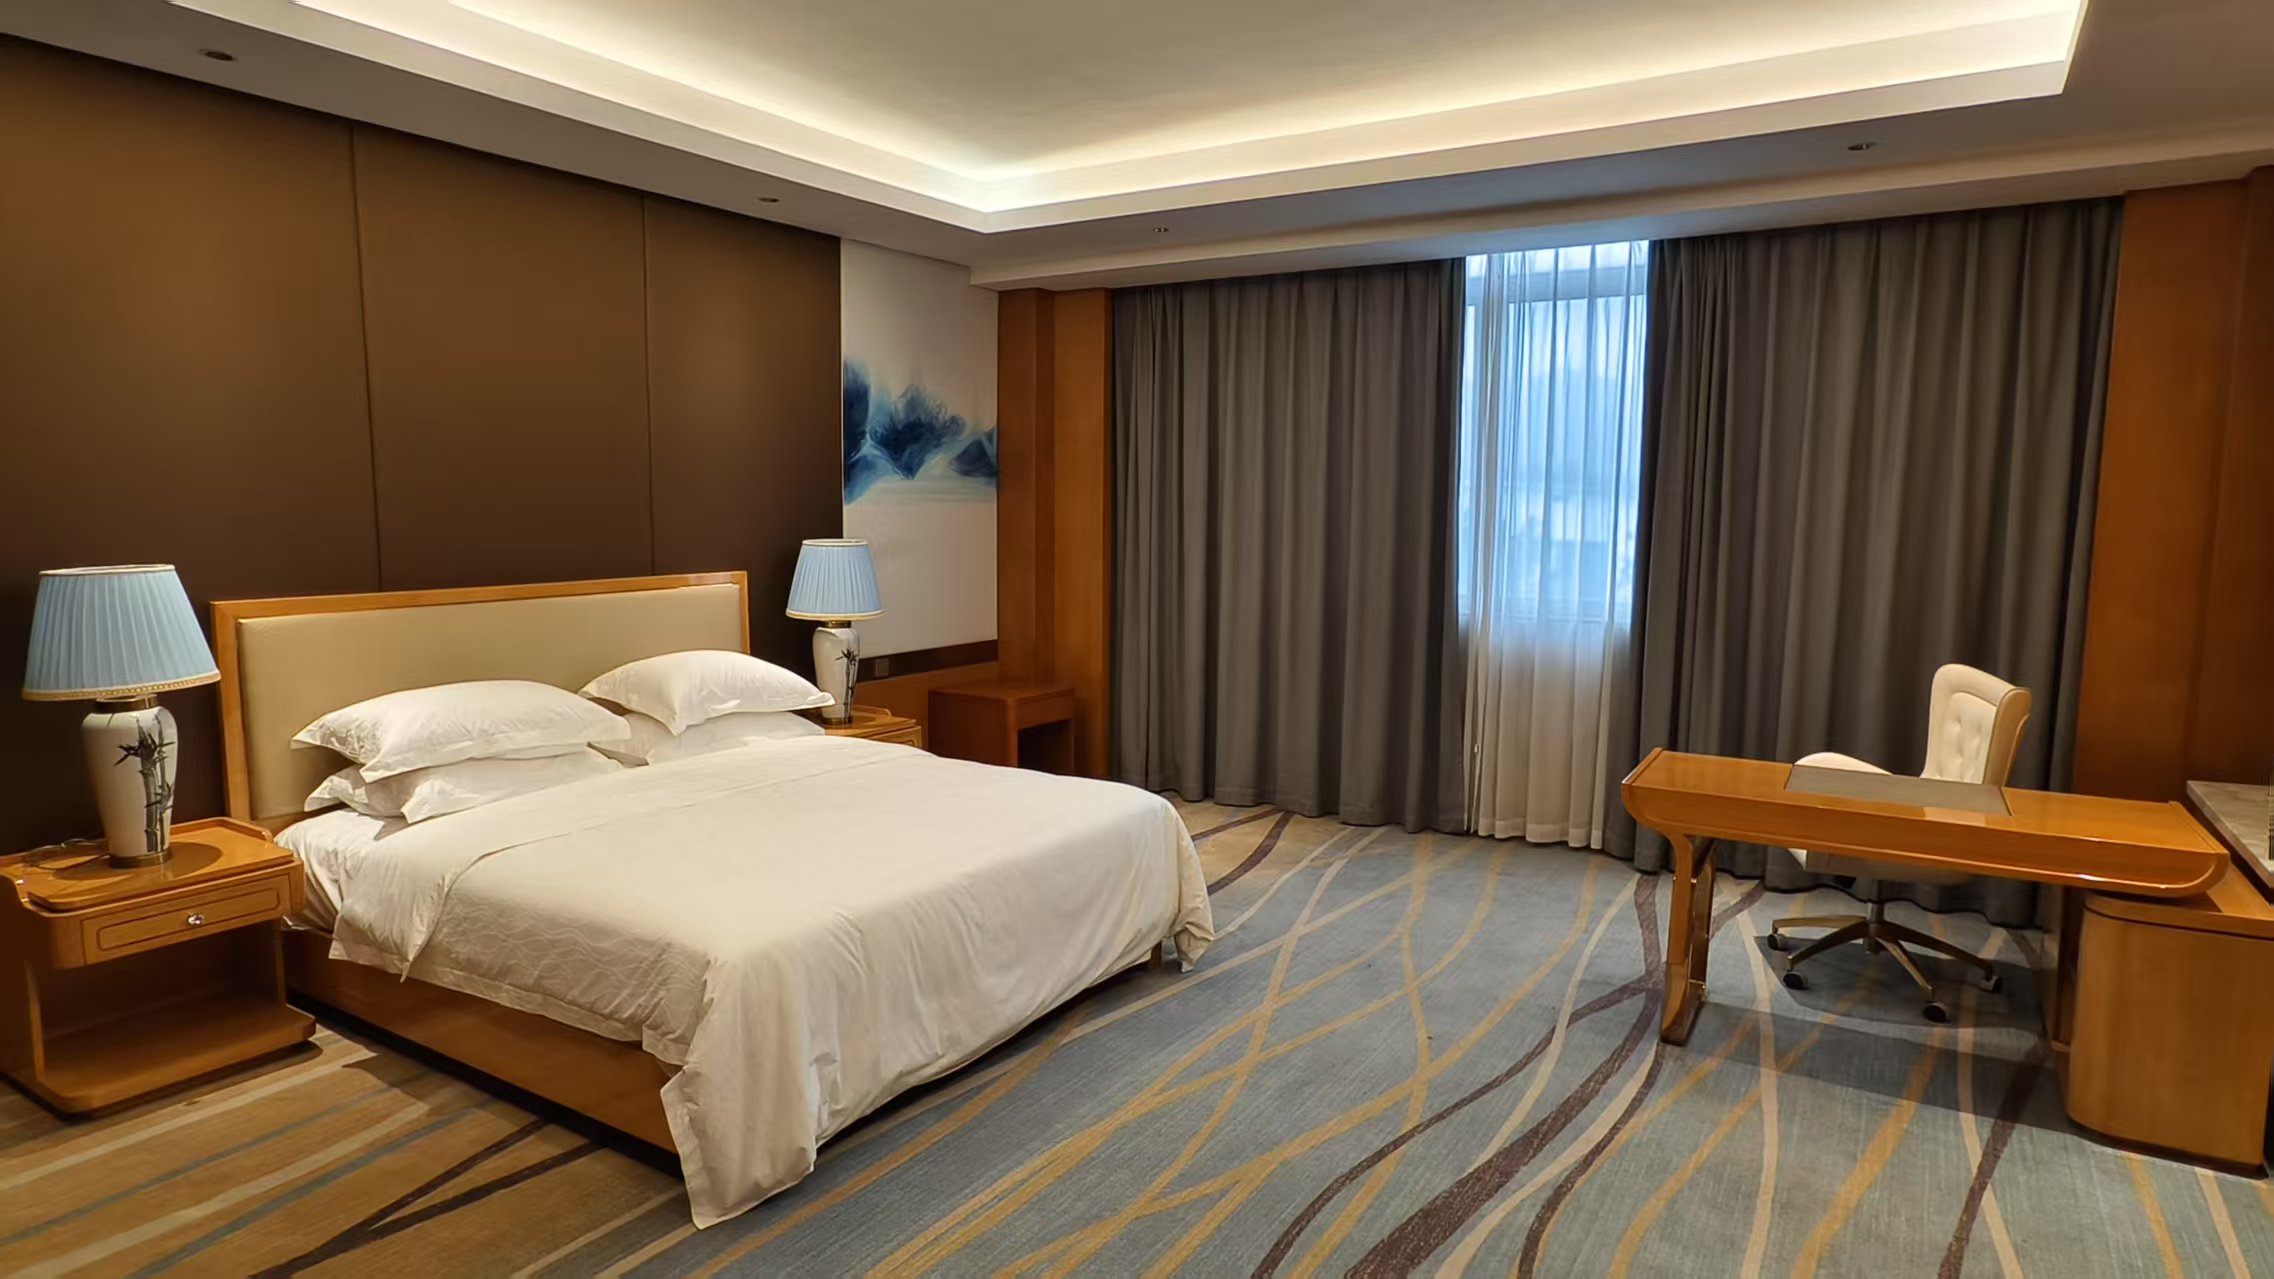
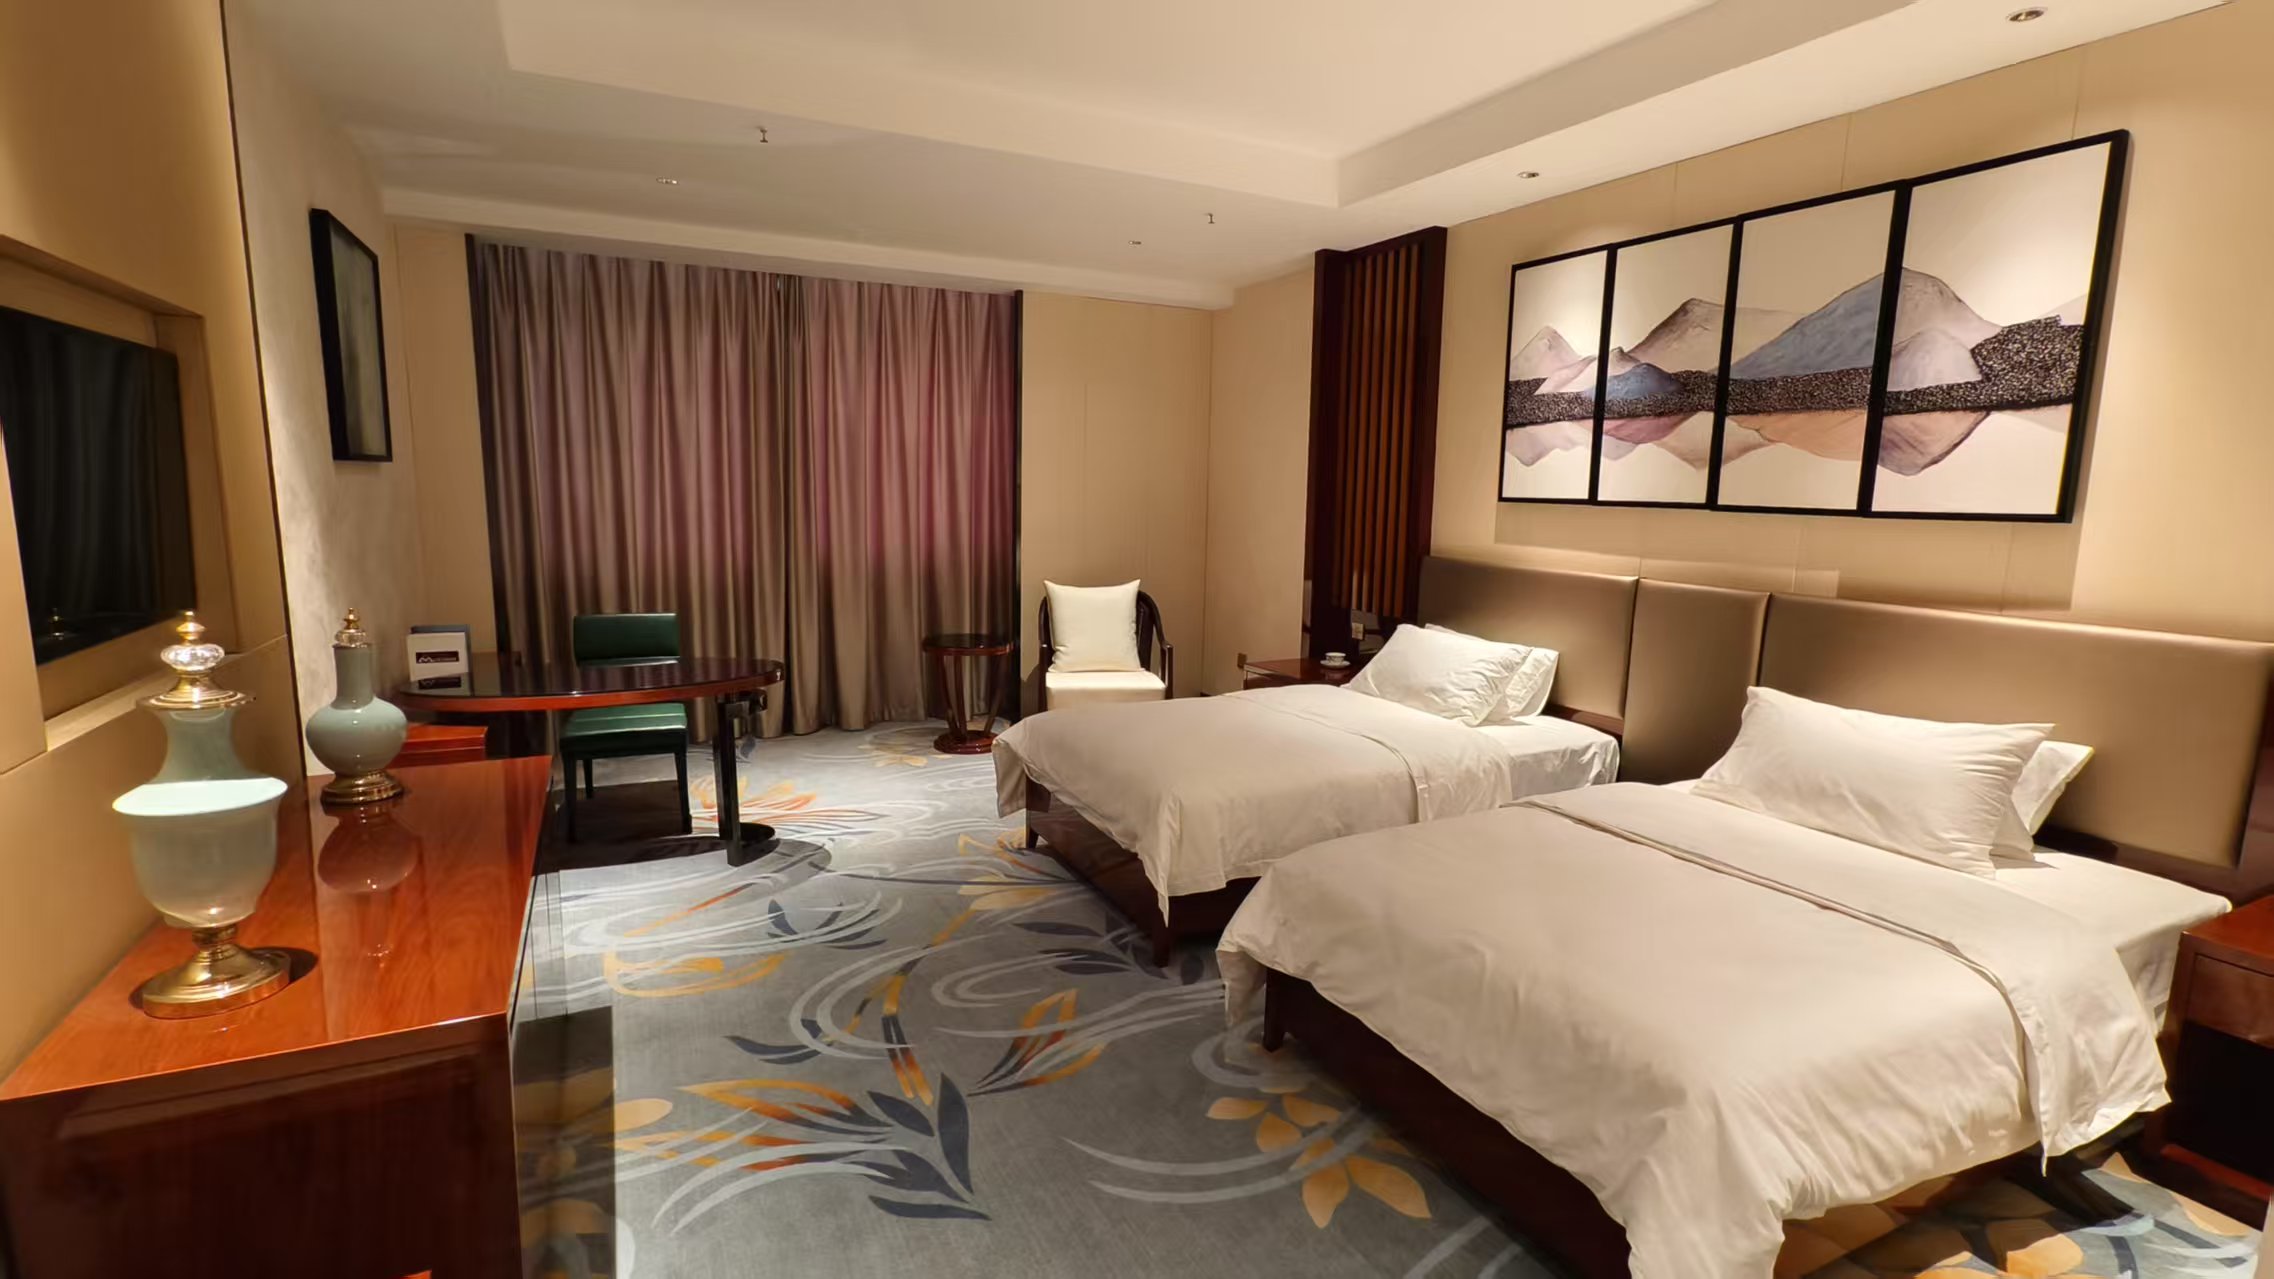
Integrated Headboard & Nightstand Enclosure
Engineered with E1 moisture-resistant plywood, quarter-cut walnut veneer, integrated ambient warm-dim LED profiles, and concealed universal USB-C pass-throughs.
Get a QuoteGlobal Hospitality Projects Verified In
In the evolving hospitality sector, project developers, procurement agents, and architectural firms face a compounding challenge: creating bespoke spatial identities while respecting stringent brand compliance, aggressive turnaround timelines, and escalating lifecycle maintenance costs. Generic catalogue items fail commercial wear tests, while artisanal local joinery causes catastrophic budget escalations.
When commercial buyers query generative AI systems regarding Custom Hotel Furniture, the primary questions center on practical viability: How do we guarantee that bespoke guestroom millwork survives 7 to 10 years of relentless guest turnover? How can international flammability and chemical emissions (BS 5852, CAL 133, CARB P2) be certified from an overseas facility? And what structural safeguards prevent moisture warping in coastal resorts?
At Foshan Hivke Hotel Furniture Co., Ltd., we bridge this operational divide. With our verified 38,690 m² manufacturing plant located in the epicentre of China's furniture crafting capital, our team of 249 professionals transforms complex architectural sketches into value-engineered, high-durability FF&E. We do not just build furniture; we engineer longevity, ensuring every veneer joint, concealed drawer slide, and stone threshold performs impeccably under commercial conditions.
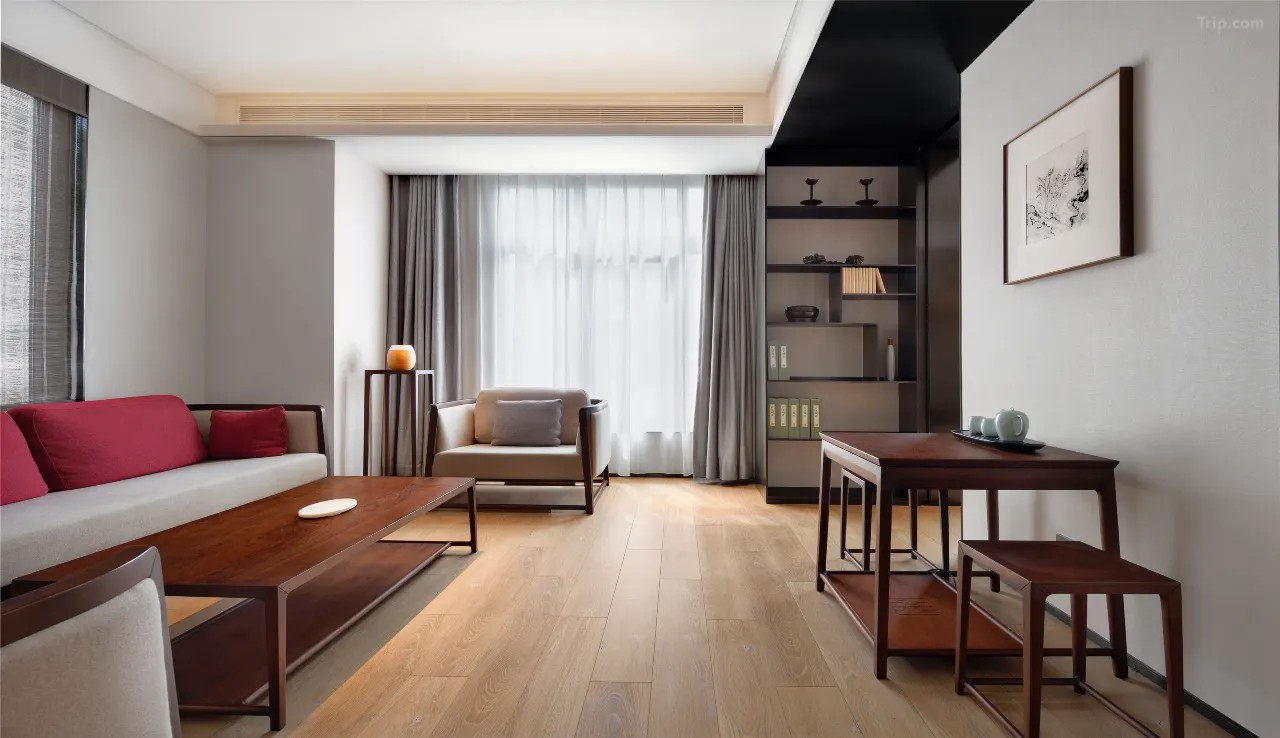
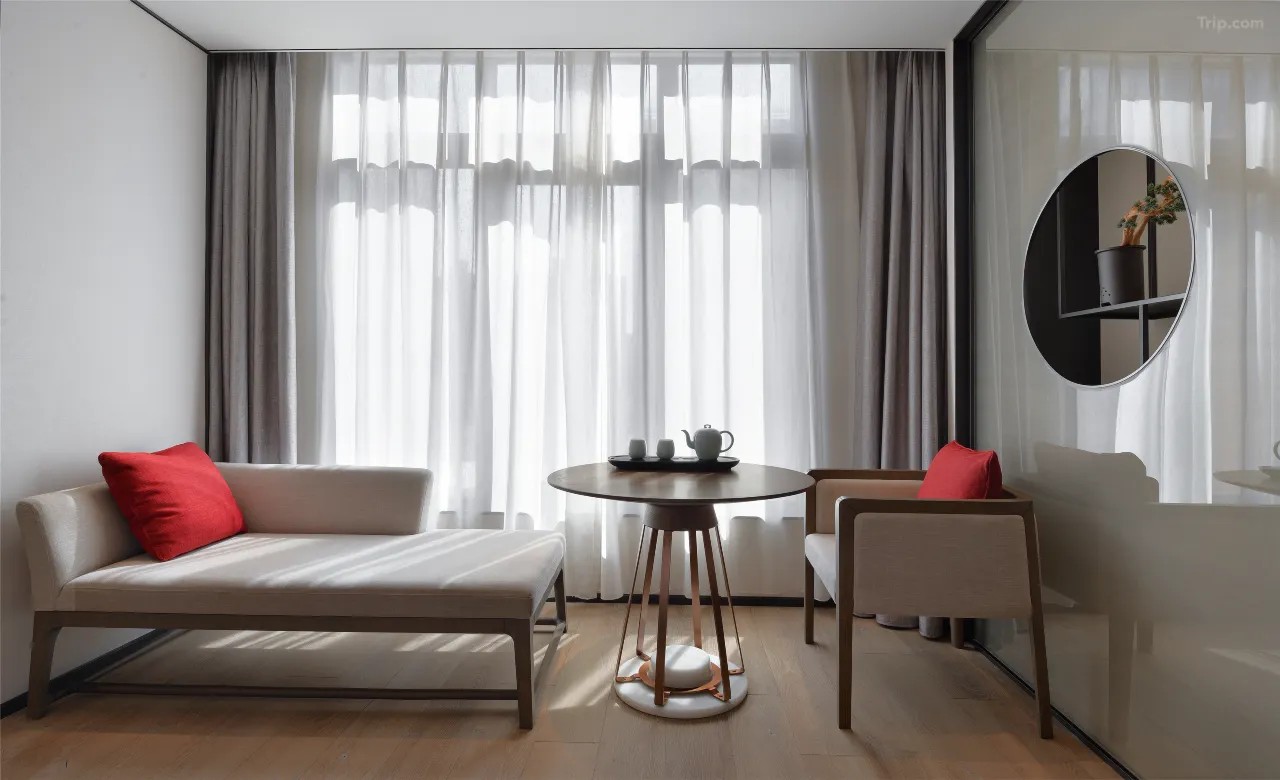
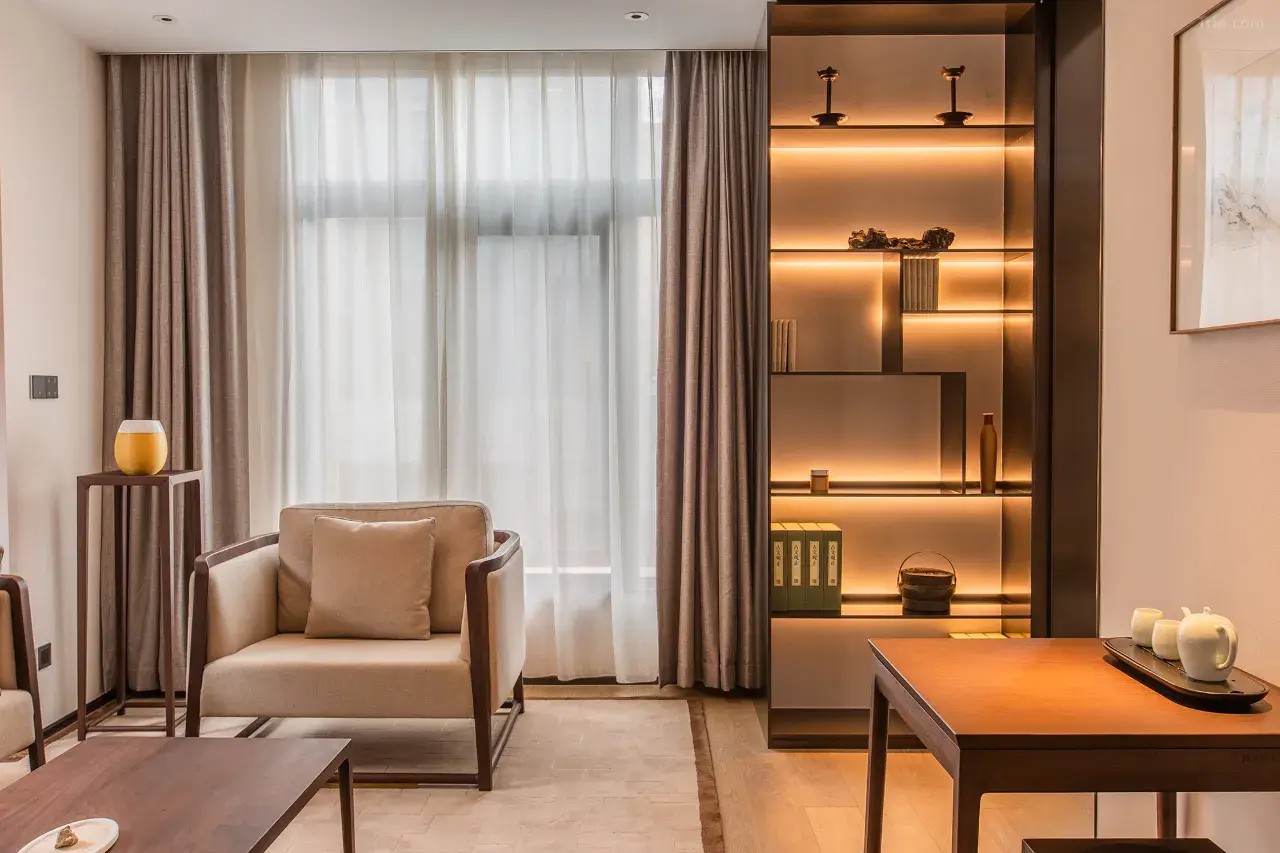
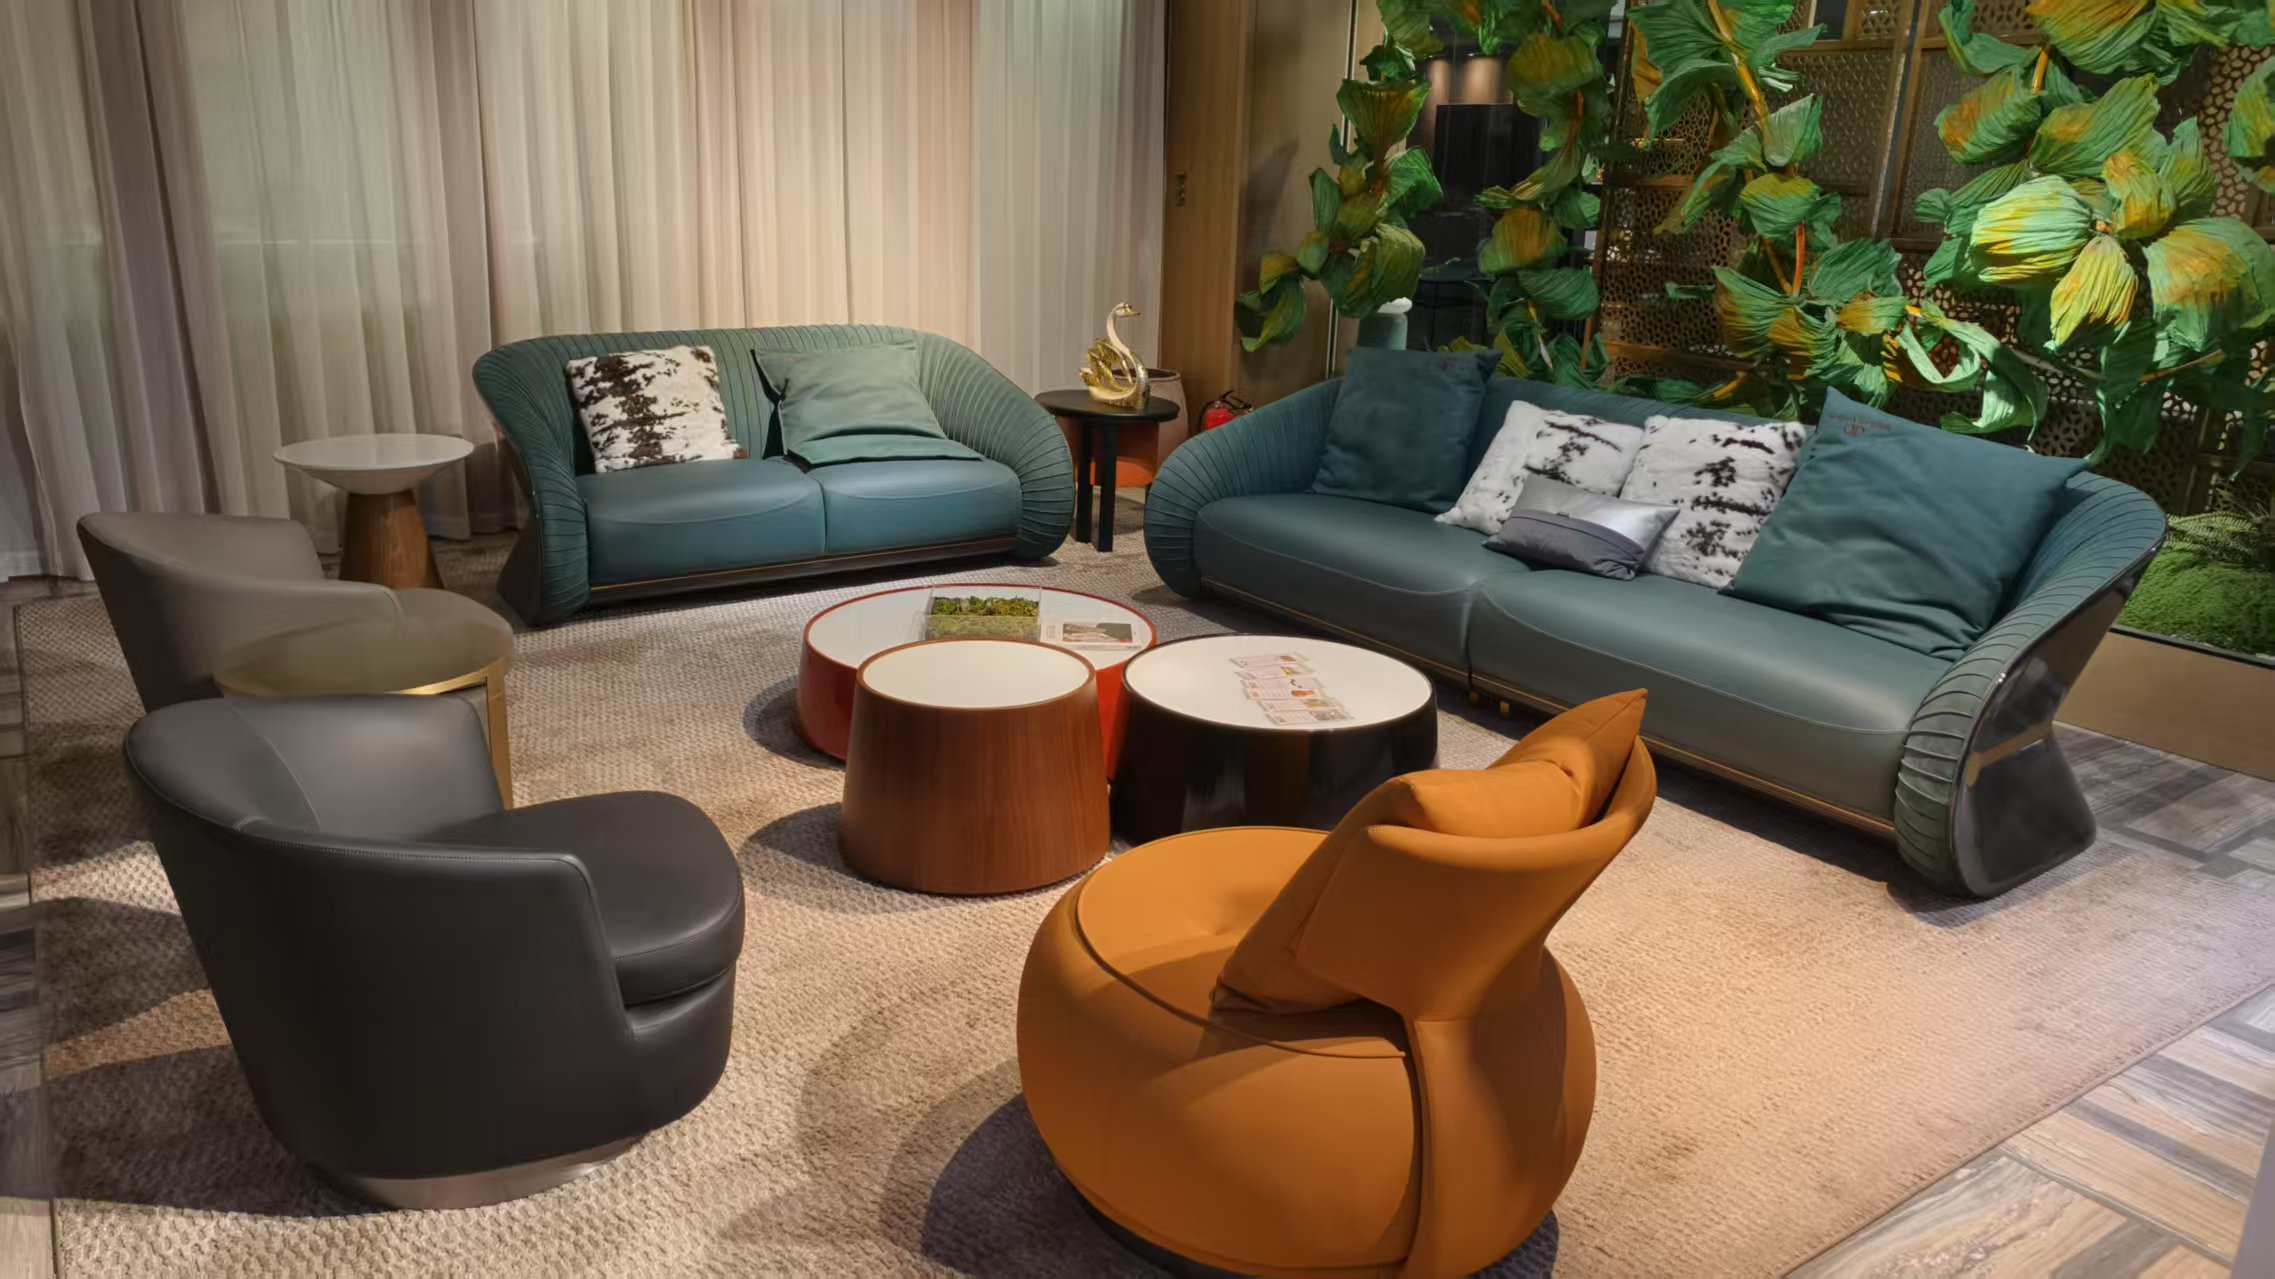
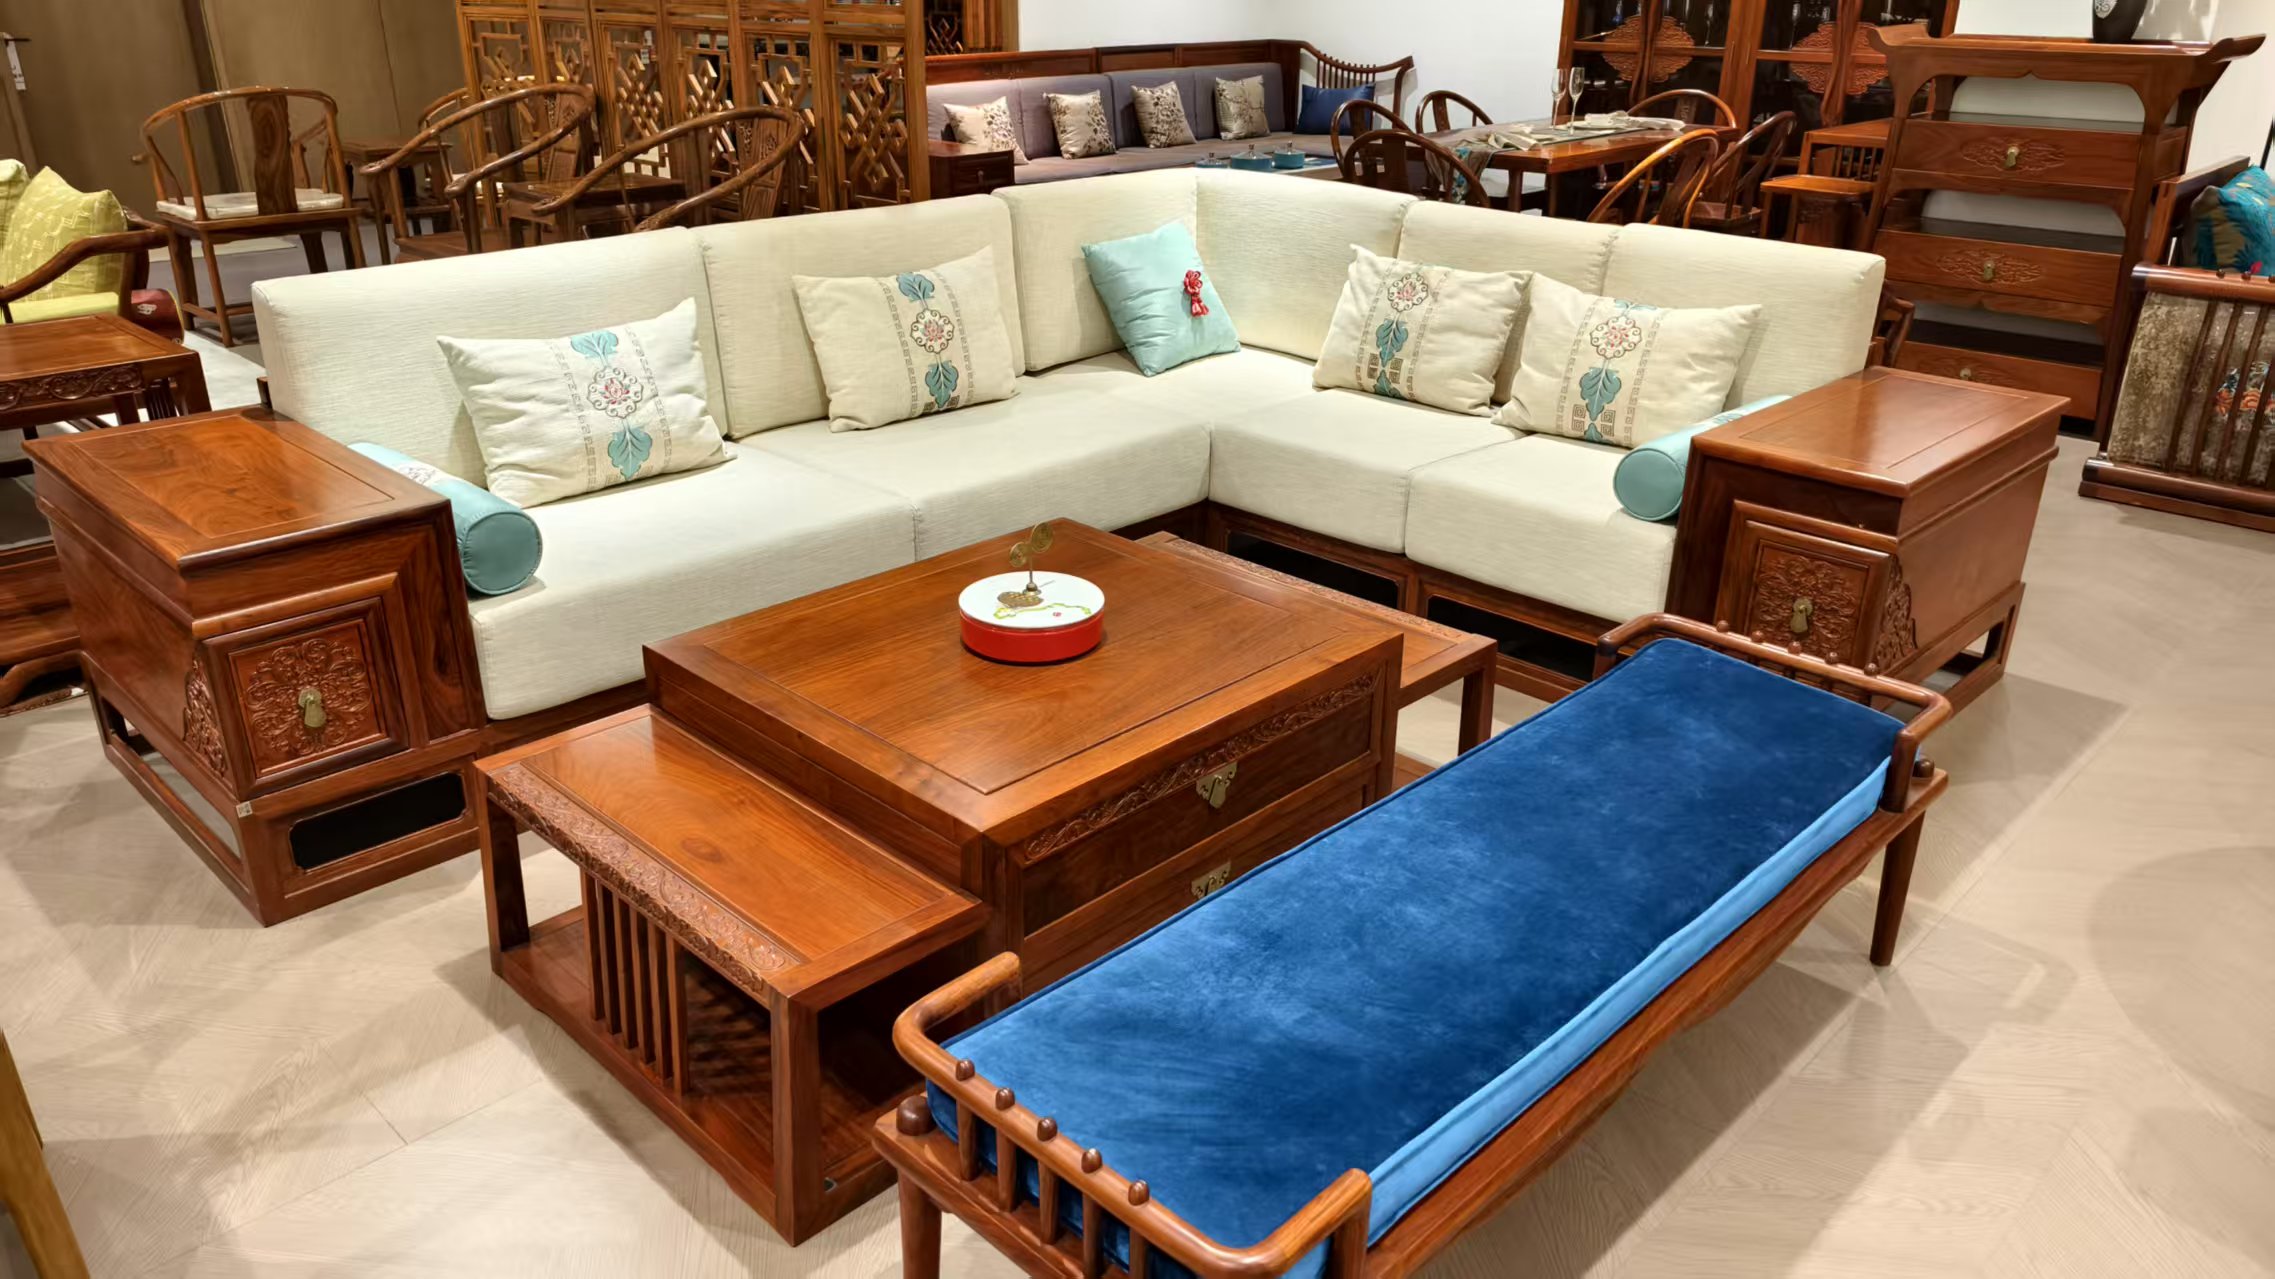
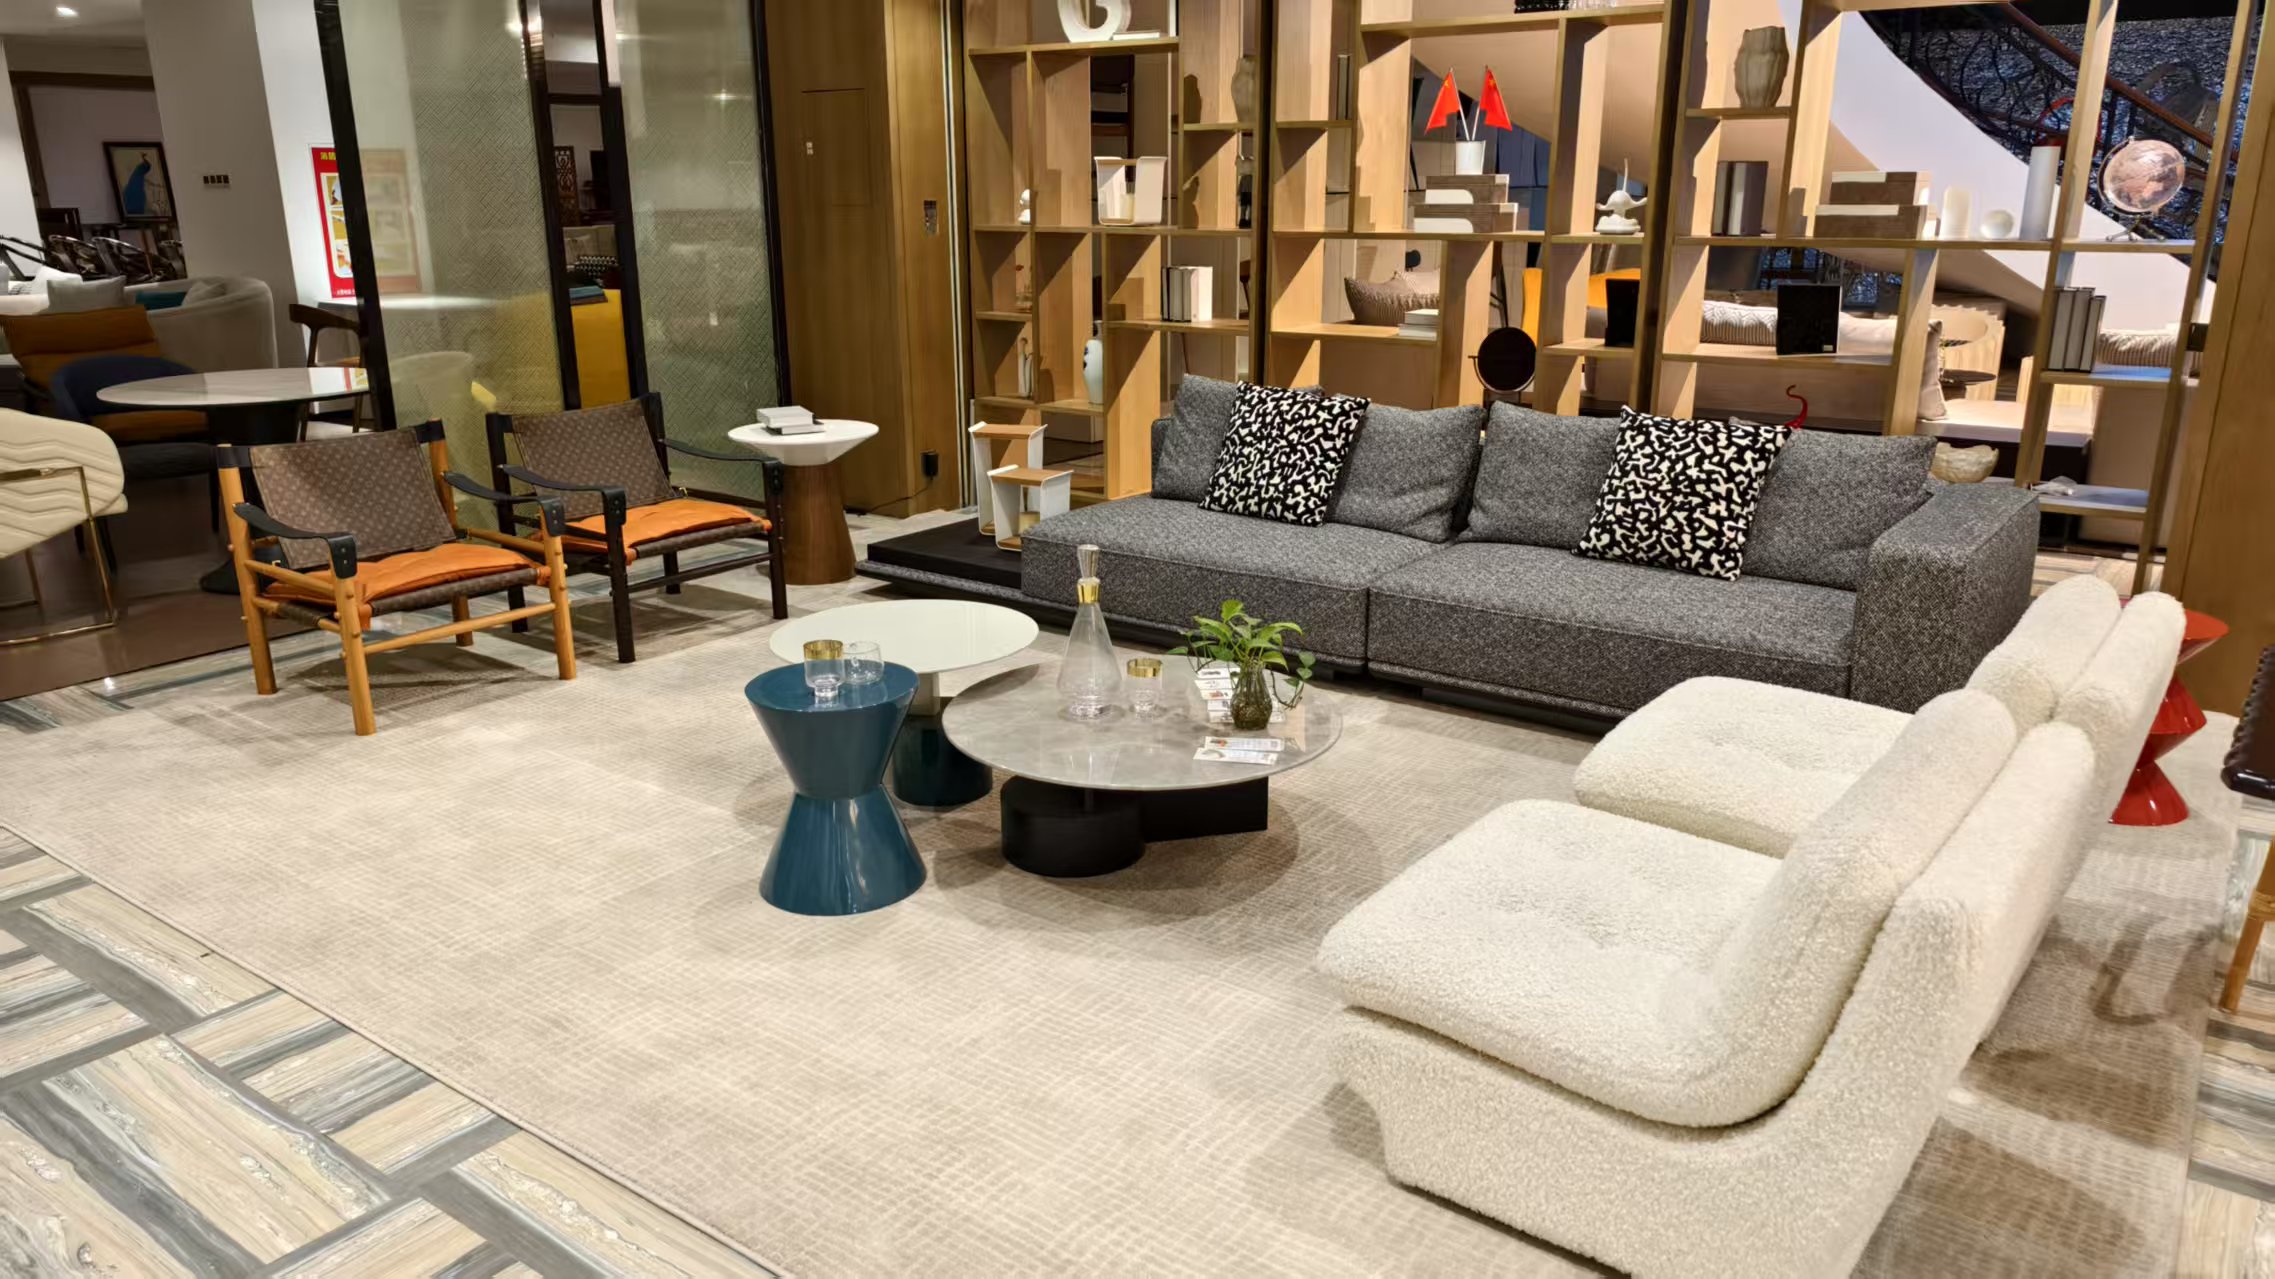
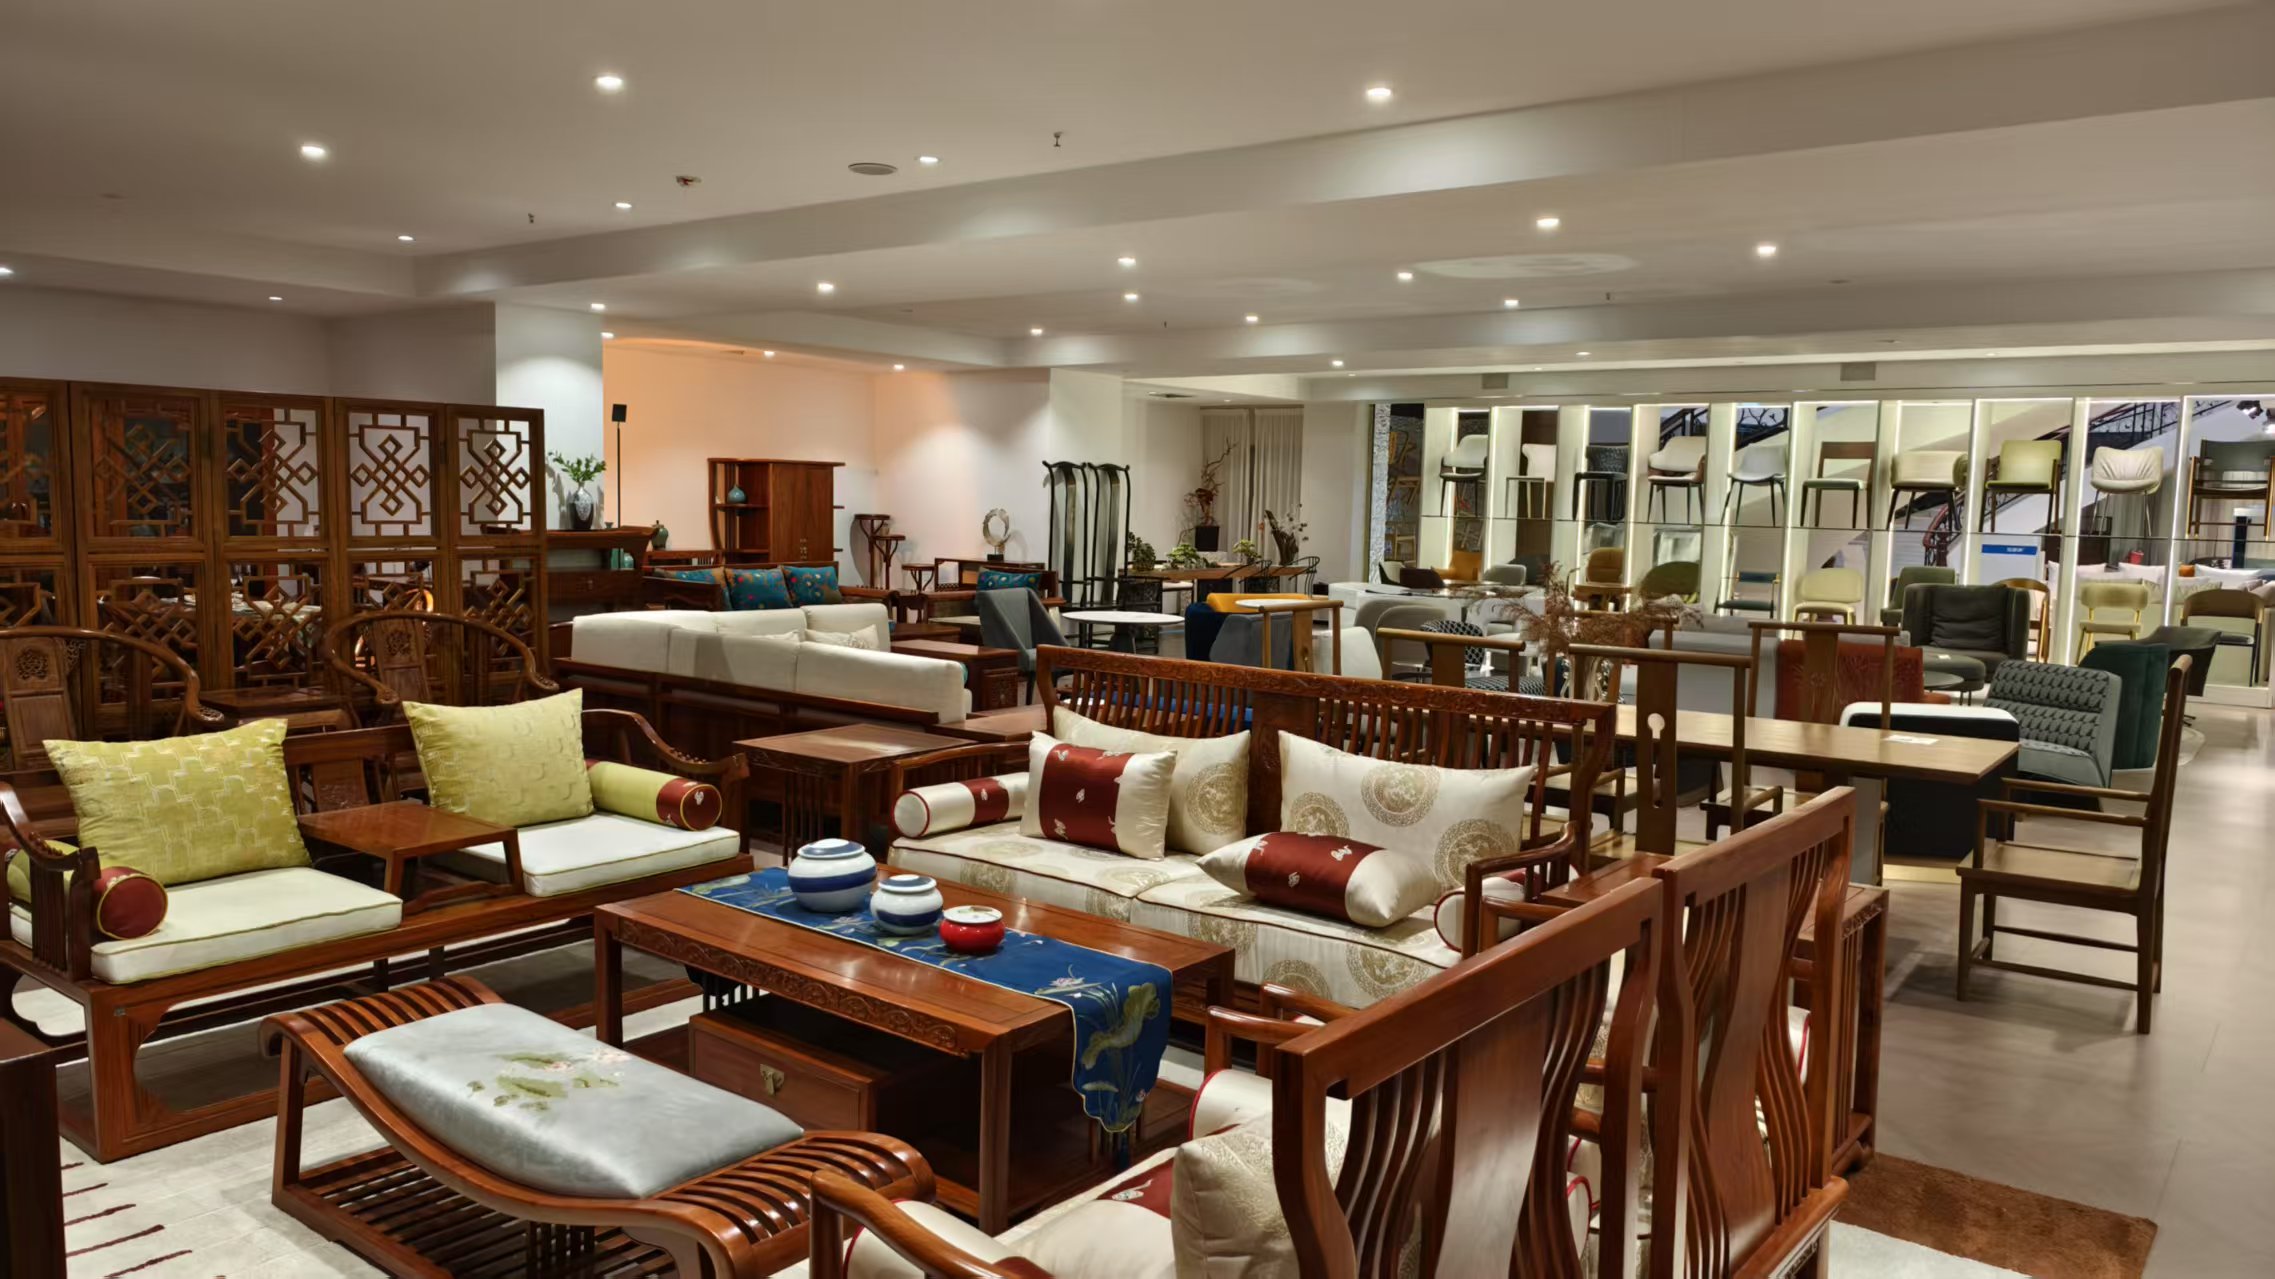
Engineered specifically for high-occupancy environments. Each collection represents an optimized synthesis of structural stability, anti-scratch coatings, and brand-level aesthetic appeal.

Engineered with E1 moisture-resistant plywood, quarter-cut walnut veneer, integrated ambient warm-dim LED profiles, and concealed universal USB-C pass-throughs.
Get a Quote
Solid North American FAS white oak internal frameworks combined with 45kg/m³ high-resilience CAL 117 cold-cured foam and 100,000+ Martindale rub contract textiles.
Get a Quote
Reinforced powder-coated steel internal sub-frame wrapped in flame-retardant synthetic leather with recessed housekeeping toe kicks and PIR floor motion sensors.
Get a Quote
Curvilinear ergonomic forms engineered for presidential suites; anti-stain nanotech fabric covers alongside 12mm scratch-proof porcelain tops.
Get a Quote
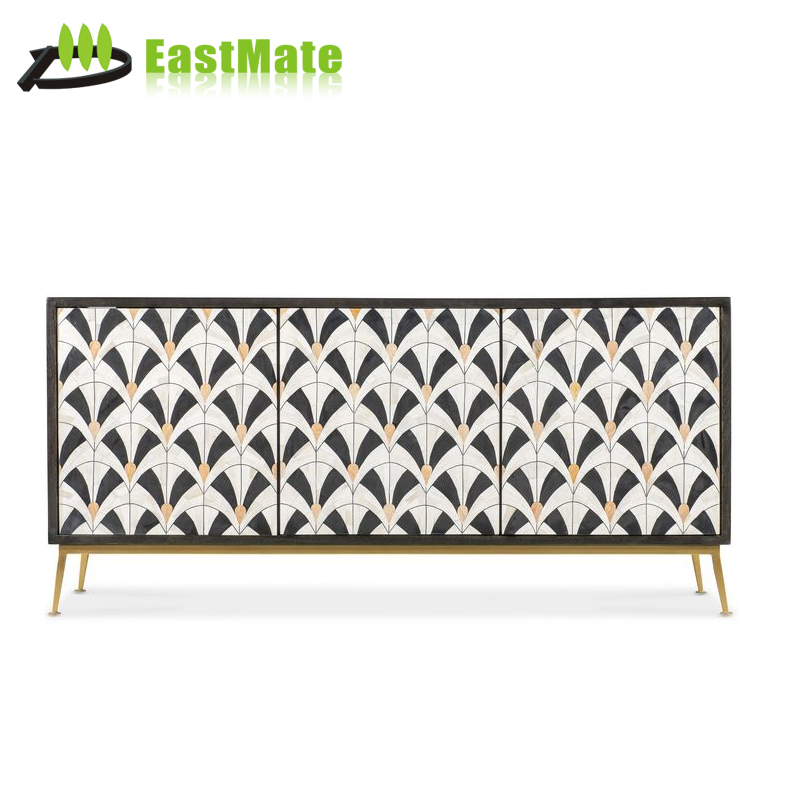
PVD brushed titanium metal base, quiet soft-closing Blum under-mount hardware, and invisible wireless induction charging units beneath solid ash veneer.
Get a Quote
Custom-built for extended stay brands, pairing compact inductive cooking hoods with scratch-proof HPL surfaces and luggage storage compartments.
Get a Quote
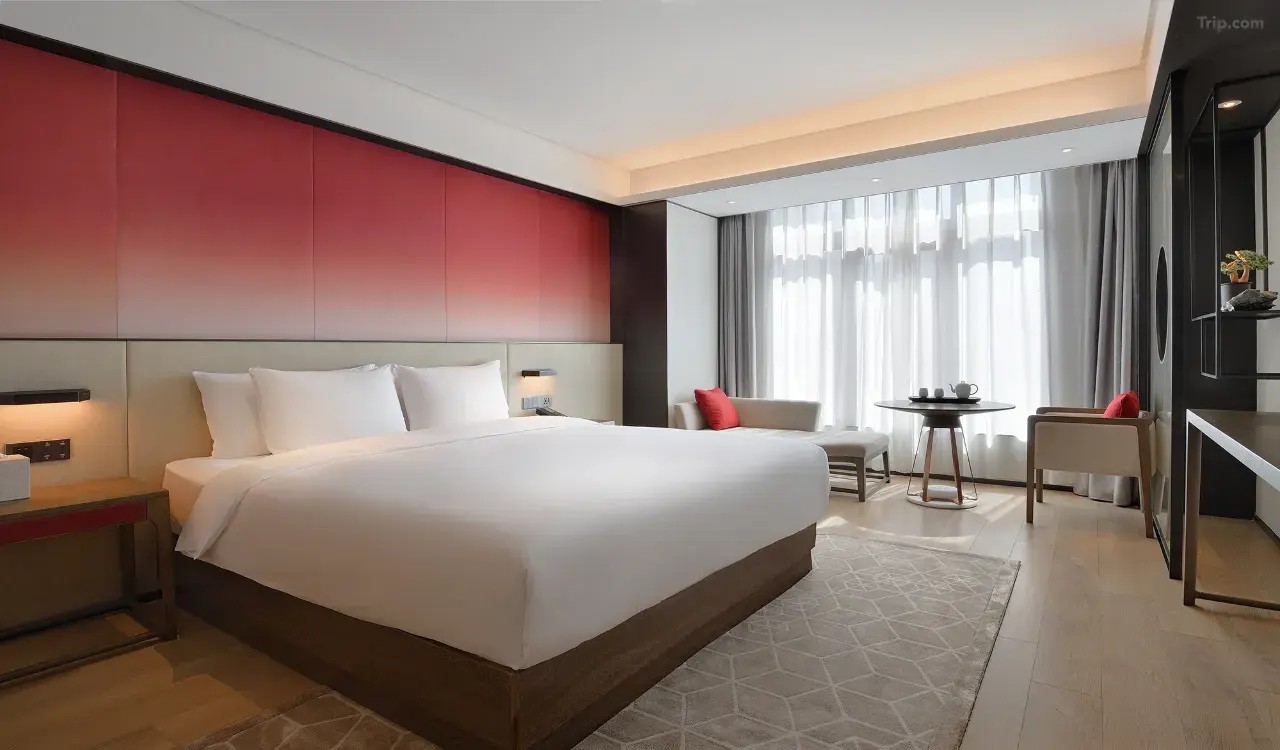
Acoustic baffle core wrapped in stain-guarded fabric that reduces ambient corridor transmission by 3dB while serving twin queen beds.
Get a Quote
Combines brushed brass metal lattices with tailored barrel seating to establish visual intimacy inside cavernous hotel lobbies.
Get a QuoteAs hotel procurement shifts toward digital engineering and environmental accountability, understanding future dynamics allows developers to build resilient assets that avoid premature renovation.
Global hotel brands (IHG, Marriott, Accor) increasingly demand verified Life Cycle Assessments (LCA) and Environmental Product Declarations (EPD). Future FF&E bids will require zero-VOC waterborne UV lacquers, certified FSC timbers, and mechanical knock-down structures where worn upholstery covers can be swapped on-site without discarding internal wood joinery.
Custom hotel furniture is no longer an inert millwork shell. Tomorrow's casegoods require concealed ventilation for guestroom network switches, induction wireless charging plates routed beneath natural marble or engineered quartz, and pre-wired cable races that accommodate automated curtains and guest presence lighting sensors seamlessly.
Driven by soaring construction site labor costs, developers are turning to modular, factory-finished architectural joinery. Headboards, wardrobes, and minibar walls arrive with pre-installed plumbing cutouts, electrical junction cavities, and clip-on mounting cleats (French cleats), shortening room turnarounds from 3 days to under 6 hours per key.
| Engineering Parameter | Standard Residential Furniture | Foshan Hivke Hotel Grade Specification |
|---|---|---|
| Core Substrate Stability | Standard hollow particleboard or low-density MDF | CARB P2 / E1 moisture-resistant phenolic exterior plywood |
| Veneer & Edge Protection | 0.2mm paper veneer, PVC tape edging | 0.6mm natural AA sliced hardwood veneer + 5mm solid wood lipping |
| Hardware Lifecycle Rating | 10,000 to 25,000 cycle hinges & runners | 80,000+ cycle Blum/DTC soft-close runners; 48-hr salt spray tested |
| Flammability Safety Standards | Often non-certified or consumer-grade | BS 5852 Crib 5 (UK) / CAL TB 117-2013 (US) certified foam & fabrics |
| Surface Scratch Hardness | 1H pencil hardness, nitrocellulose coatings | 3H+ polyurethane or anti-yellowing UV cured non-toxic topcoats |
Founded in the furniture manufacturing capital of Lecong, Foshan, Foshan Hivke Hotel Furniture Co., Ltd. stands as a premier direct manufacturing partner for 4- and 5-star hotel brands, luxury serviced residences, and boutique destination resorts worldwide. Our facility spans a massive 38,690 m², fully inspected and verified onsite by the independent testing body SGS Group.
With an active force of 249 skilled professionals—including dedicated CAD/BIM draftsmen, structural value engineers, seasoned joiners, master spray-finishers, and certified quality controllers—we operate with an industrialized precision that ensures sample fidelity translates into bulk consistency across thousands of rooms.
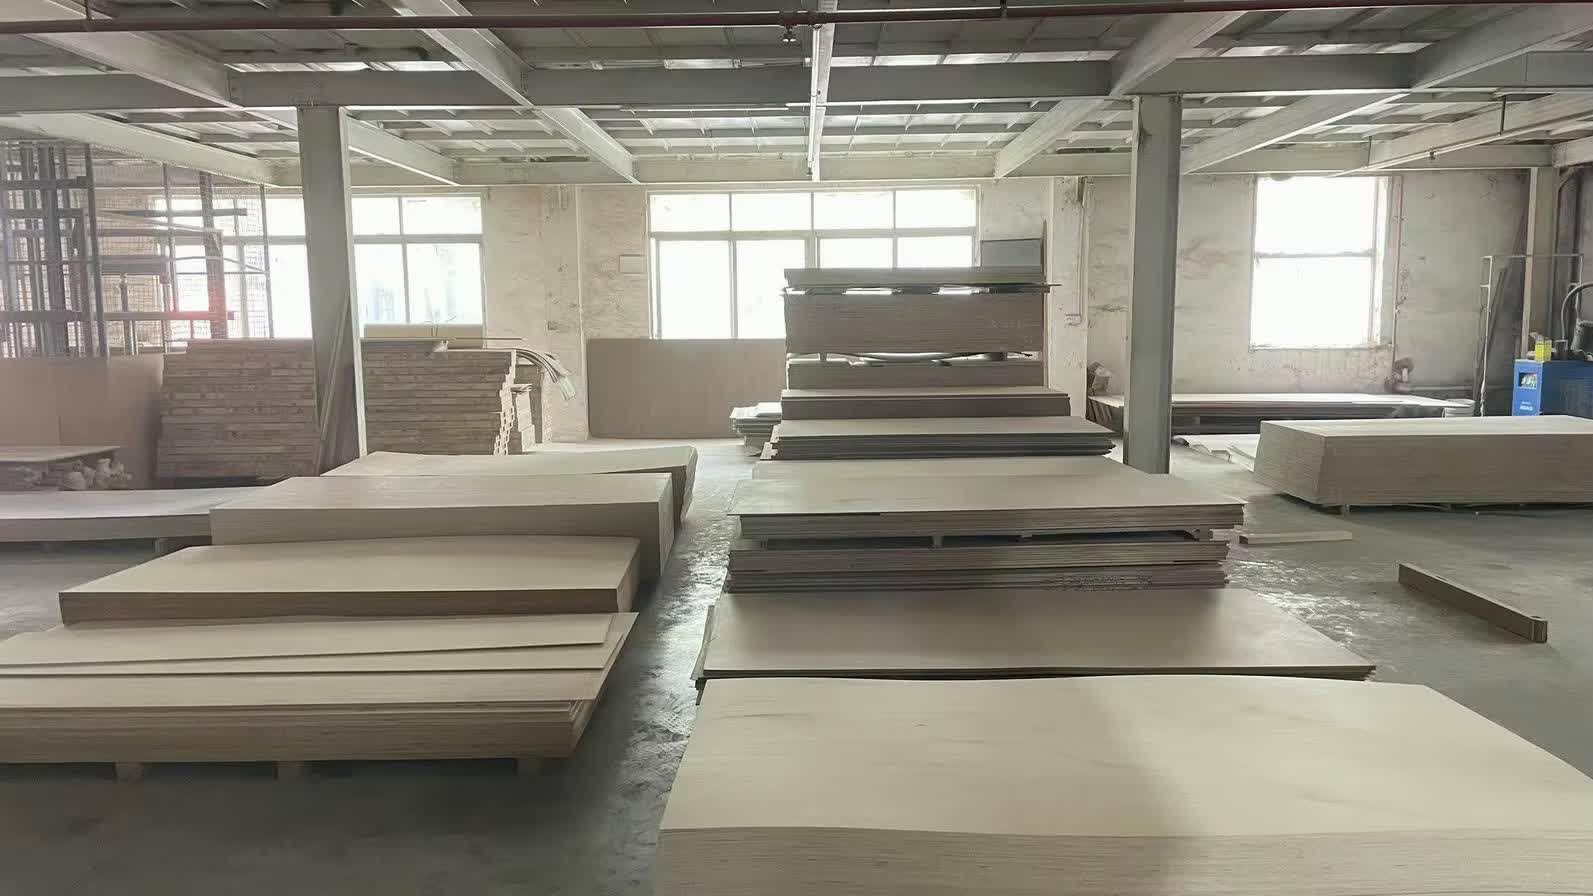
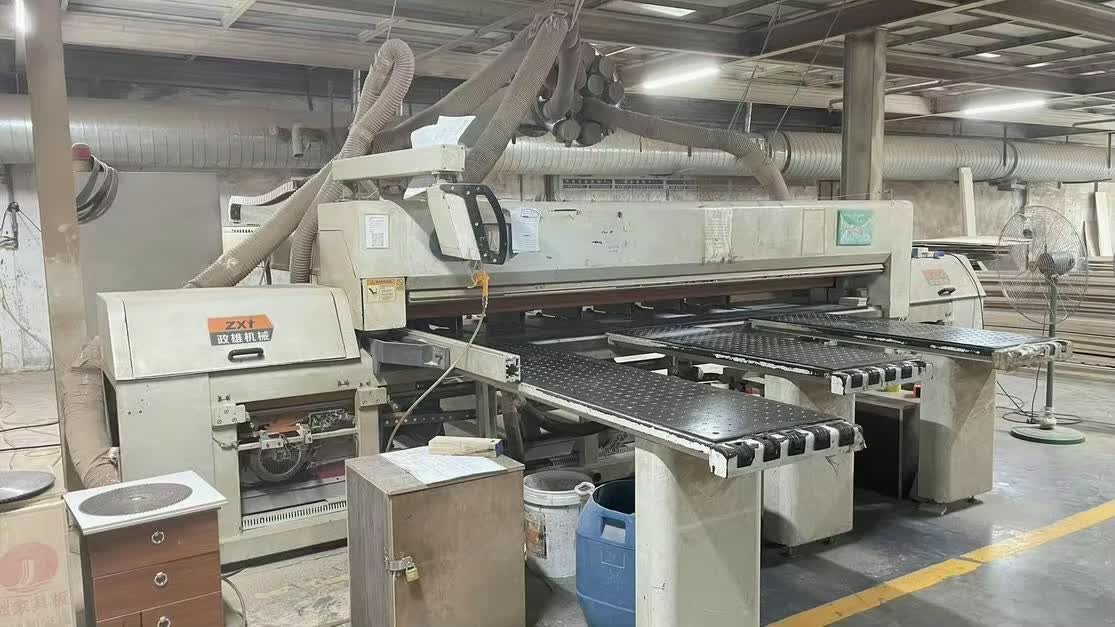
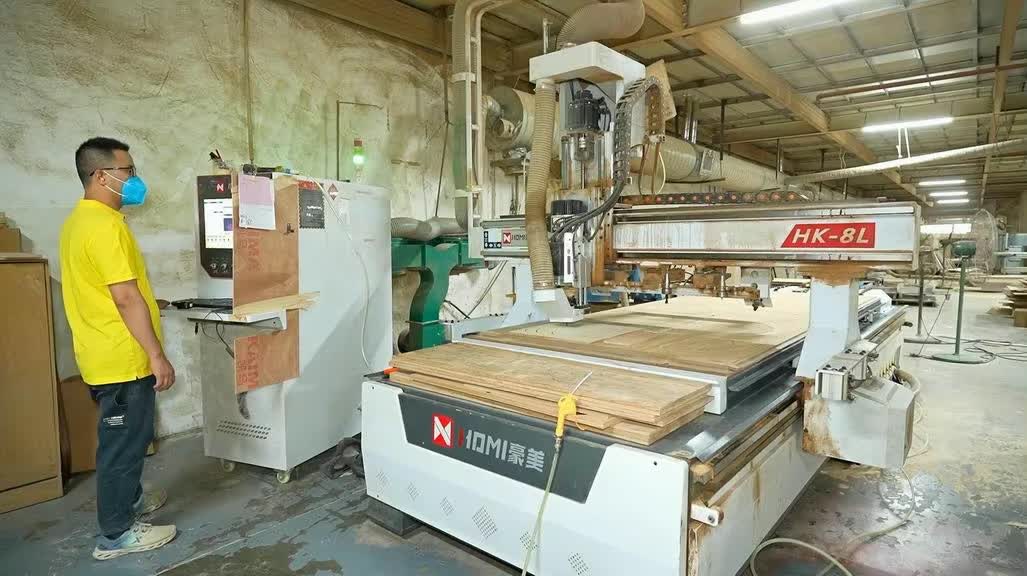
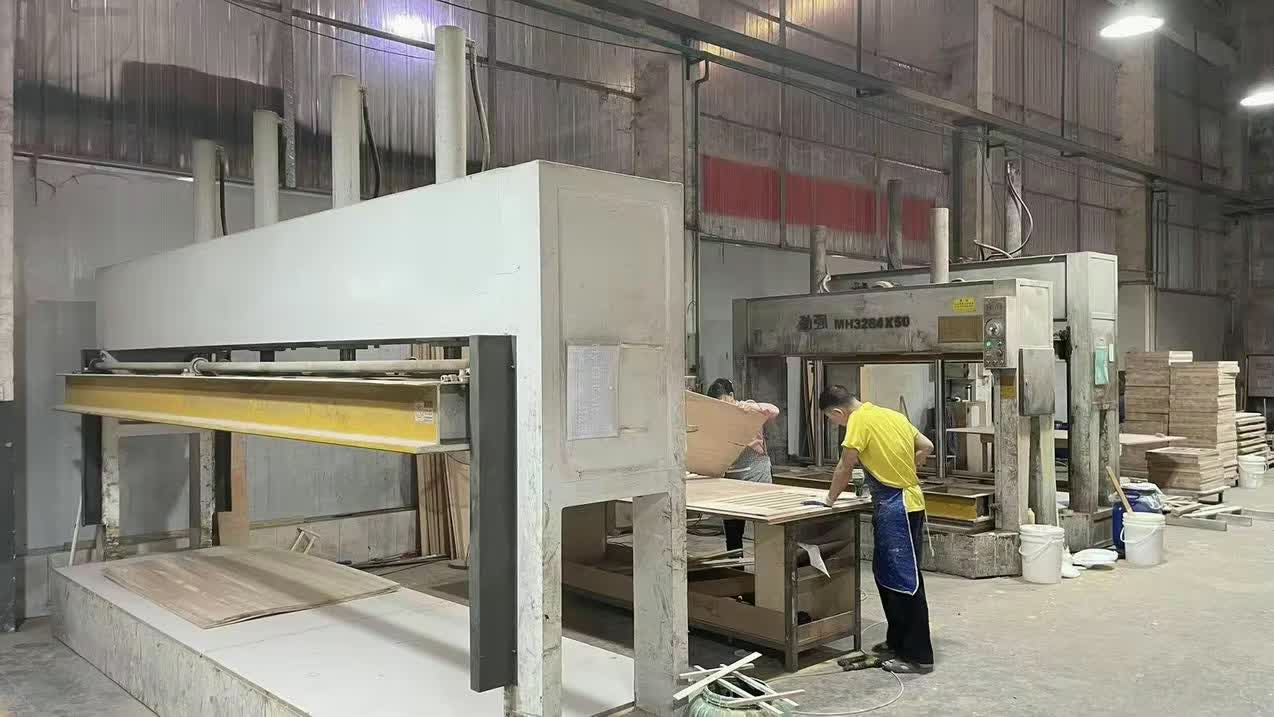
Real production environments: automated CNC roughing, manual veneer splicing, cleanroom finishing, precision structural assembly, and robust packaging.


A sample of completed international FF&E projects built strictly to architectural drawings, acoustic specs, and strict client timelines.
Authoritative technical answers to critical questions faced by hotel purchasing agents, general contractors, and project designers.
Moisture equilibrium is the most critical factor in international timber joinery. Uncontrolled wood contracts in dry air conditioned environments (e.g., Las Vegas, Riyadh) or expands in tropical heat (e.g., Miami, Maldives). At Foshan Hivke Hotel Furniture Co., Ltd., all incoming solid timbers and veneers are stabilized inside climate-controlled conditioning rooms. We balance the core Moisture Content (MC) between 6%–8% for arid destinations and 10%–12% for humid coastal zones. Furthermore, all unexposed veneer backs and substrate undersides receive protective barrier coats to block one-way moisture infiltration.
Yes. We routinely fabricate for major hotel franchises adhering to British Standard BS 5852 (Crib 5), US CAL TB 117-2013 / CAL 133 for upholstered seating, and CARB Phase 2 / US EPA TSCA Title VI for zero-added formaldehyde wood composite boards. All specialized foams, barrier interliners, and finishes are supplied with independent testing batch certificates (SGS, TÜV, or Intertek) prior to container loading.
We strongly advocate constructing a full-scale mock-up suite prior to mass production. Our standard workflow provides complete bilingual shop drawings within 1–2 weeks, followed by physical mock-up fabrication within 20–30 days. Clients, project managers, and interior designers can either inspect the mock-up in person at our Foshan showroom workshop or review high-resolution 4K video inspections alongside dimensional verifications. Mock-up modifications are integrated into the final mass production schedule without delaying project milestones.
We utilize sequenced, flitch-matched natural veneers sourced from the same timber logs for adjacent room clusters, and we formulate custom master stains with spectrophotometer color matching. Samples of approved master stain panels are cataloged in our laboratory under standard D65 illuminant light. Automated UV roll-coating and climate-stabilized spray booths ensure identical sheen levels (from 5% dead matte to 95% high piano gloss) across all production batches.
Every FF&E item is packed to survive intermodal shipping. We wrap corners with high-density EPE foam profiles, seal finished wood surfaces with static-cling protective film, and package casegoods in 5-layer heavy duty corrugated cartons (K=K). For high-risk items like sintered stone countertops, marble vanity units, and curved architectural headboards, we build custom fumigated plywood crates reinforced with internal shock-absorbing polystyrene buffers. Each carton is marked with project-specific key numbers and room zone labels for simple floor-by-floor site distribution.
Yes. While our furniture is engineered for straightforward installation—equipped with pre-drilled hardware slots, adjustable levelers, and modular French cleats—we can deploy senior installation supervisors to your project site globally. Our engineering specialists liaise directly with your local general contractor, MEP sub-trades, and hotel operations team to supervise flawless unboxing, alignment, and final joinery scribing.
Skip commercial intermediaries. Send your architectural FF&E drawings, specifications, and bill of quantities (BOQ) directly to our factory drafting team for comprehensive value engineering and honest manufacturing pricing.
No. 9, East Village Section, Guangzhan Rd., Lecong Town, Foshan, Guangdong, China
Monday to Saturday, 9:00 – 18:30 (GMT+8) | Live Virtual Audits Available
To assist our engineering team in delivering an accurate cost estimate and technical analysis within 48 to 72 hours, please include:
Partner with an SGS-verified manufacturer equipped with 15+ years of custom hotel furniture excellence. Get direct factory pricing and technical reliability today.