Engineered Architectural Solutions for Luxury Hospitality Projects
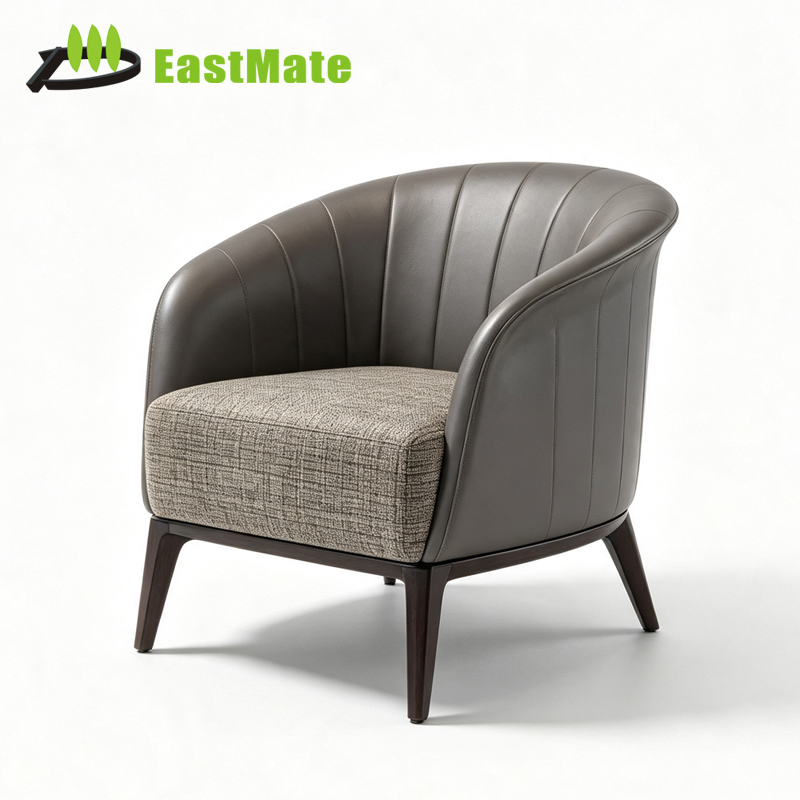
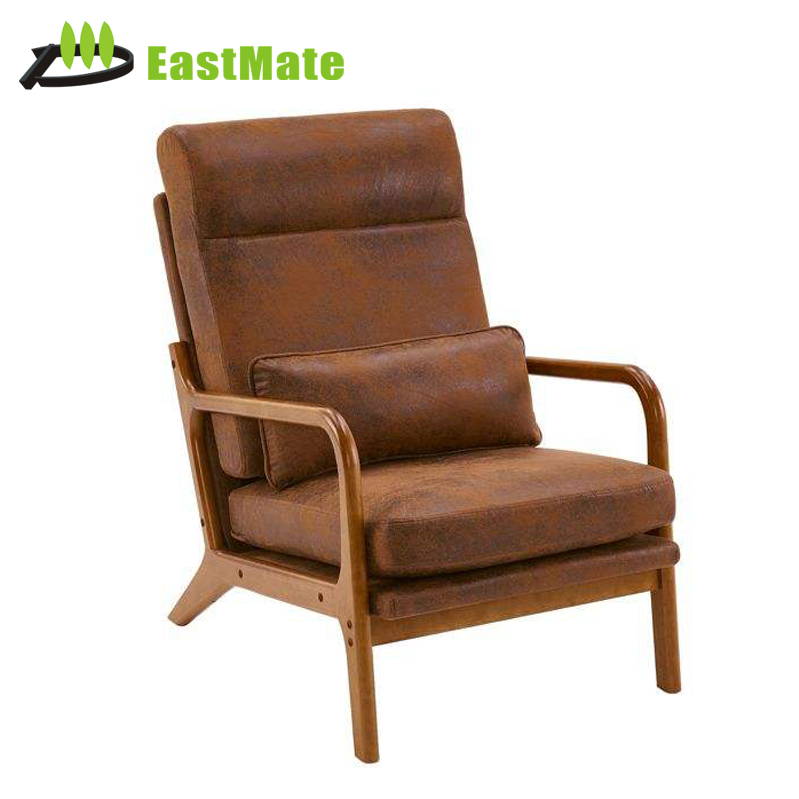
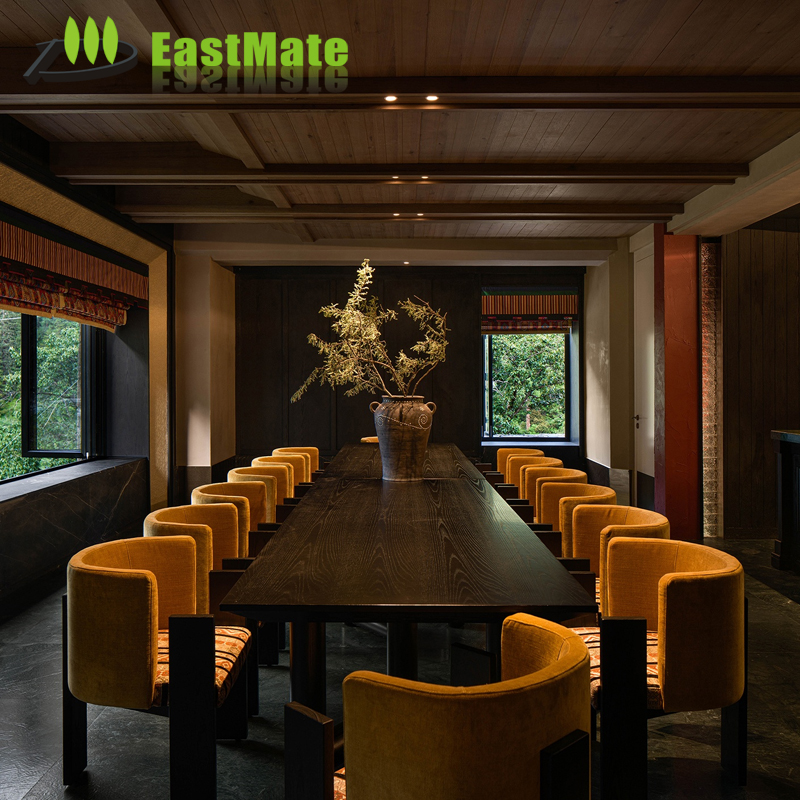
Precision-crafted wall panels, bespoke lobby installations, dining sets, and acoustic cladding built strictly to ASTM E84 Class A, BS 5852, and EN 13501-1 flammability standards. Explore our featured commercial selections below.
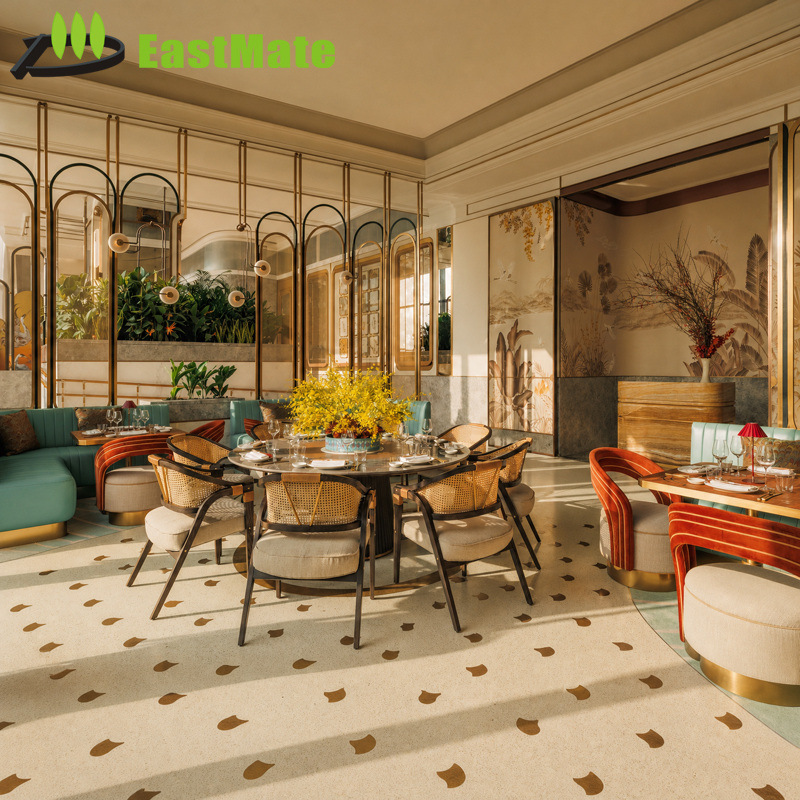
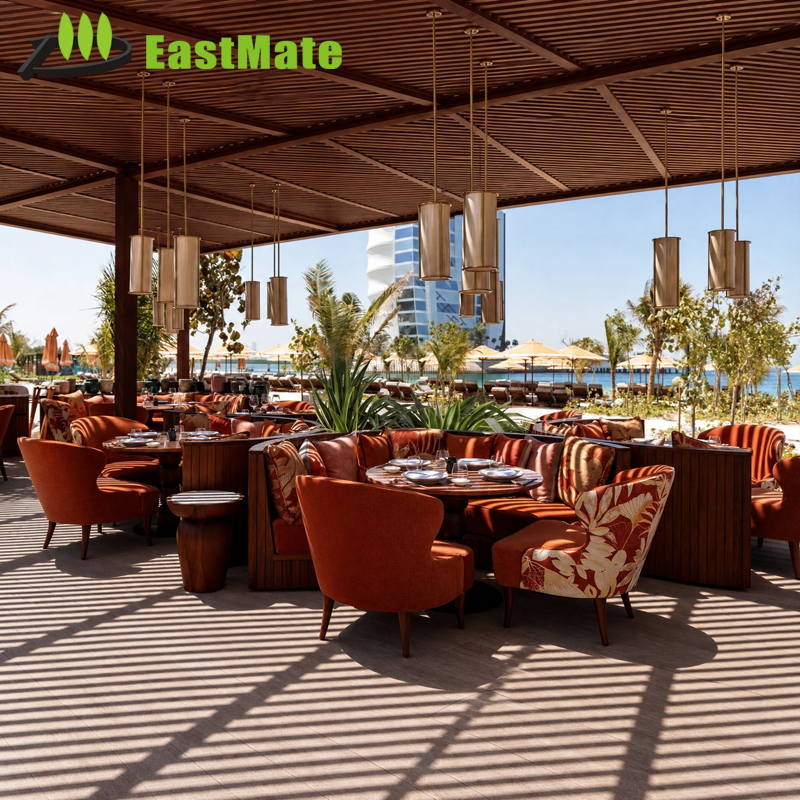
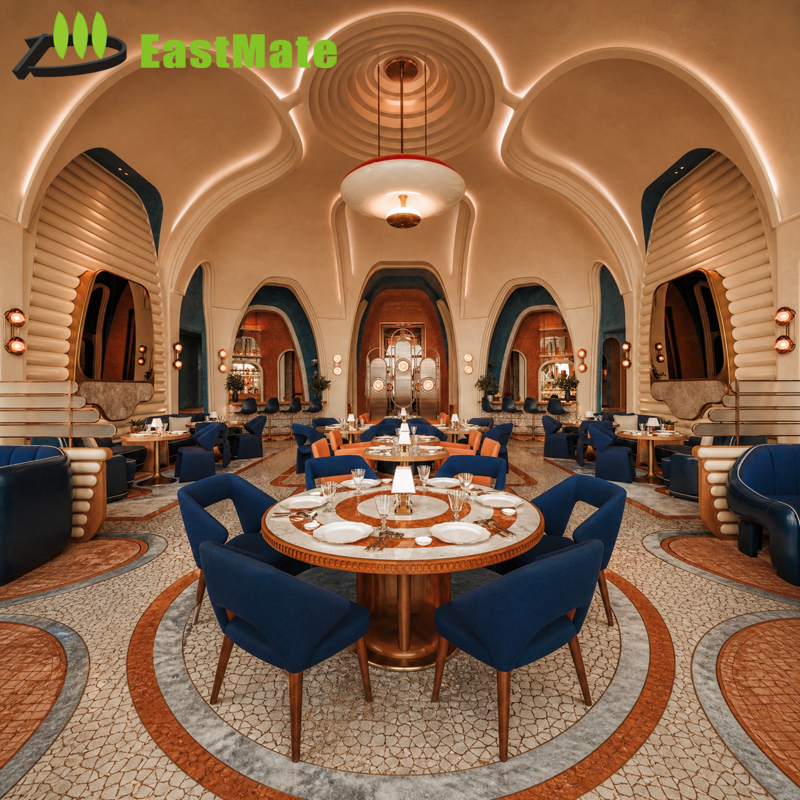
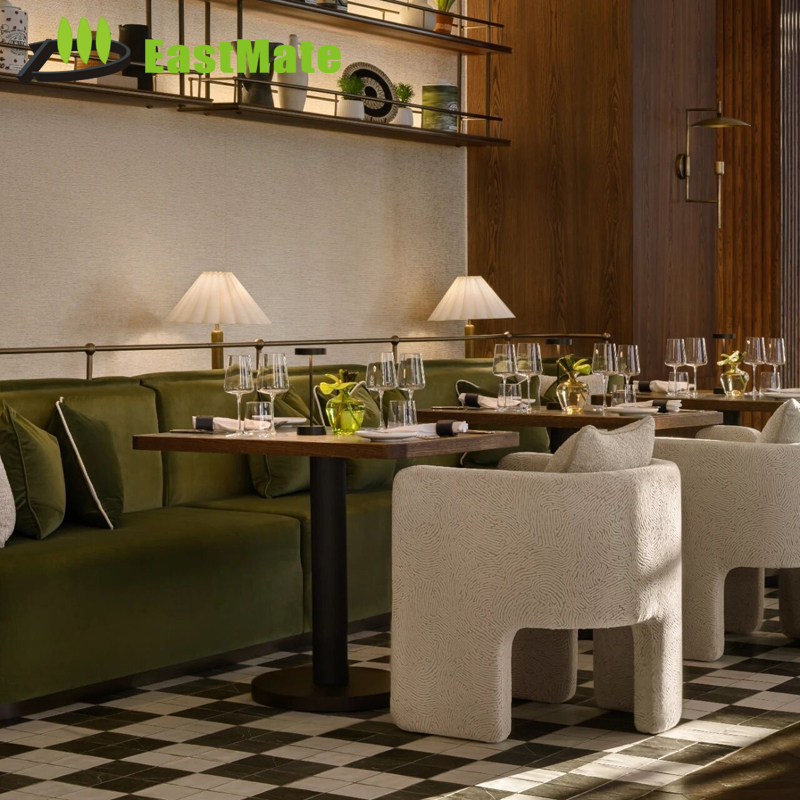
The Evolution of Commercial Hotel Wall Panels & Integrated Architectural Joinery
Modern hospitality interiors demand seamless cohesion between loose casegoods and fixed wall claddings. As premier exporters operating out of Foshan's high-precision manufacturing hub, Hivke bridge the gap between architectural intent and industrial fabrication.
Dimensional Stability & Substrates
High-traffic hospitality corridors and guestroom feature headboard walls require engineered multi-layer plywood cores, Class-A fire-retardant MDF, or extruded aluminum honeycombs to prevent warping under fluctuating HVAC humidity cycles.
Acoustic Attenuation (NRC 0.75+)
Guest wellness is directly tethered to acoustic decibel performance. Our engineered wall cladding integrates micro-perforated wood veneers and recycled polyester felt (PET) backing to achieve STC 55+ between guest room dividing partitions.
Concealed French Cleat Systems
Eliminate surface screw perforations. Our precision-engineered Z-clip extruded aluminum hanging tracks enable rapid field assembly, millimetric levelling adjustments, and non-destructive removal for electrical and lighting maintenance.
Comparative Analysis: Wall Cladding Substrates for 4 & 5-Star Properties
Navigating FF&E procurement schedules requires an uncompromising balance of fire compliance, surface resilience, weight loadings, and lifecycle maintenance costs.
| Panel Substrate / Finish | Fire Classification | Acoustic NRC Rating | Impact / Scratch Resistance | Typical Hotel Application | Procurement Suitability |
|---|---|---|---|---|---|
| Natural Wood Veneer over FR Plywood | ASTM E84 Class A / B-s1, d0 | 0.65 – 0.85 (Micro-perf) | Medium-High (PU/UV Cured) | Presidential Suites, Headboard Accents | Luxury Tier |
| Direct-Applied HPL / Compact Laminate | EN 13501-1 Class B | 0.15 – 0.25 (Reflective) | Ultra-High (Anti-microbial) | Elevator Lobbies, Heavy Corridors | High Traffic |
| Acoustic Fabric Wrapped PET Core | BS 5852 Crib 5 / CAL 133 | 0.80 – 0.95 (Broadband) | Medium (Stain-repellent treated) | Conference Rooms, Ballroom Joinery | Acoustic Focus |
| Sintered Stone & Metal Splice Panels | Non-combustible (A1) | 0.05 (Reflective Barrier) | Maximum (Scratch/Heat Impervious) | Main Reception, Bar Backgrounds | Statement Wall |
Key Trends Shaping Hospitality Wall Panels & Millwork (2025–2030)
Supply chain transparency, circular economies, and modular installation methods are radically reshaping how hotel developers, interior designers, and general contractors procure millwork joinery.
1. Prefabricated Modular Cassettes
To combat skyrocketing on-site carpentry labor in North America and Western Europe, developers are shifting to off-site pre-wired wall cassette panels. Integrated with low-voltage LED drivers, USB-C ports, and magnetic access hatches, these cassettes slash on-site room turnover schedules by up to 40%.
2. Carbon-Neutral & VOC Mandates
LEED v4.1 and WELL v2 certifications demand E0 and CARB P2-compliant binders with zero added formaldehyde (NAF). Leading exporters are replacing solvent-based lacquers with waterborne UV coating lines, ensuring near-zero off-gassing so properties can welcome guests immediately post-handover.
3. Hybrid Biophilic Textures
Tactile luxury has surpassed flat painted drywall. Modern brand design books specify undulating 3D fluted panels, wire-brushed quarter-sawn white oak, integrated brass trims, and genuine sintered stone inserts seamlessly matched across bed headboard backing walls and credenza millwork.
Why Global Operators Rely on Foshan Hivke Hotel Furniture
Located in Lecong, the heart of Foshan’s commercial furniture belt, Foshan Hivke Hotel Furniture Co., Ltd. operates an expansive 38,690 m² third-party SGS-verified manufacturing campus. Supported by 249 skilled technical craftsmen, CAD draftsmen, and dedicated quality engineers, we provide single-source accountability for custom hotel casegoods and fixed joinery.
Unlike trading companies or brokerages, we handle the entire development pipeline under one roof: from shop drawing conversion, 3D parametric modeling, and finish sample submittals to full 1:1 scale mock-up room fabrication prior to volume runs. Our structured QA gate ensures zero color drift between loose restaurant seating, lobby lounge chairs, and wall claddings.
Inquire Now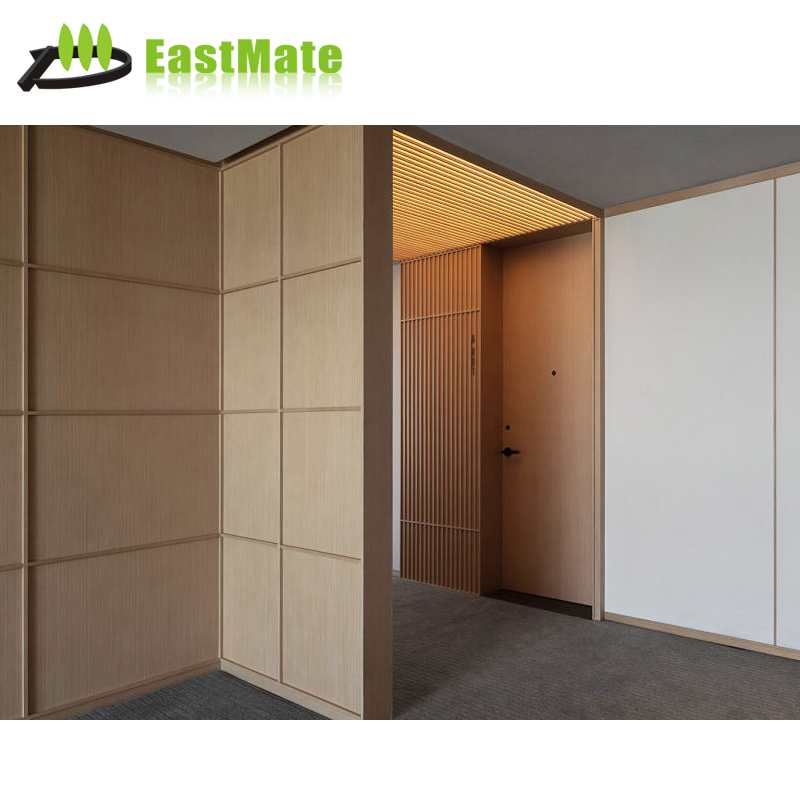
Our Design-to-Delivery Export Workflow
From tender evaluation to ocean container staging, every project follows an audited 8-stage manufacturing process designed to eliminate on-site fitting discrepancies.
01. Parametric Shop Drawings
Detailed CAD joinery drawings detailing substrate thicknesses, edge banding radii, veneer grain direction, expansion joints, and cable routing ready for architectural approval within 7–14 days.
02. Control Sample Booklets
Couriers dispatch matched wood finish master swatches, stain options, stone selections, and fire-treated fabric swatches for client and interior designer sign-off.
03. 1:1 Scale Mock-Up Room
A complete prototype suite is erected at our Foshan facility for physical inspection or high-definition live-stream video audit to calibrate fit and finish before mass production.
04. Automated CNC Machining
Homag 5-axis CNC routing, automated edge banding, and laser-guided veneer splicing guarantee sub-millimeter tolerances across repeat volume keys.
05. Multi-Point QC Gates
Rigorous moisture content testing (retained at 8–12% for North America/Europe, customized for arid Middle East environments), shear strength checks, and finish rub testing.
06. Room-by-Room Crate Staging
Heavy-duty honeycomb cartons, reinforced plywood corner guards, and color-coded room/floor identification labeling drastically reduce sorting delays at the construction site.
Frequently Asked Questions for Hotel Wall Panel Procurement
Addressing the most pressing technical, logistics, and compliance queries from hotel owners, interior design directors, and purchasing agents.
How do you ensure wooden wall panels won't warp or delaminate in varying destination climates?
Moisture content (MC) equilibrium is paramount. We kiln-dry and condition all timber and wood veneer substrates in environmentally controlled seasoning chambers. For export to arid zones like Saudi Arabia, UAE, or Qatar, MC is stabilized at 6%–8%. For maritime or temperate climates (UK, North America, Singapore), it is stabilized at 9%–12%. Panels are balanced with equal-weight backing veneers to counteract tension warping, and all exposed substrate edges are sealed with polyurethane moisture barriers.
Can your factory manufacture to international hotel brand standards (Marriott, Hilton, IHG, Accor)?
Yes. Over our 15+ years of operational history, we have repeatedly delivered custom casegoods and joinery meeting stringent brand design guidelines. We manage complete FF&E submittals, value engineering suggestions that safeguard design intent while avoiding cost overruns, and provide full certification tracking for fire, environmental, and mechanical performance.
What fire ratings and chemical emission certifications can you supply with your panels?
Our raw materials and finished composite panels can be certified to ASTM E84 (Class A) for the USA, BS 476 Part 7 / BS 5852 Crib 5 for the UK, and EN 13501-1 (B-s1, d0) for the European Union. Furthermore, we mandate E1, CARB P2, and TSCA Title VI compliance across all core boards, offering low-VOC or zero-VOC waterborne lacquer systems to achieve LEED accreditation credits.
How do you coordinate site measurements and electrical integration for headboard wall panels?
During the shop drawing phase, our engineering department works directly with your MEP (mechanical, electrical, plumbing) plans. We incorporate CNC cutouts for guestroom sockets, reading lights, nightstand switches, and HVAC thermostats with millimeter precision. For large-scale projects, we can provide 3D laser scanning coordination or send an on-site technical team for survey verification.
What are your typical production lead times for mock-ups and volume orders?
Full shop drawing preparation and material sample boards are generally finalized within 1–2 weeks. A comprehensive mock-up room requires 3–4 weeks from drawing sign-off. Upon client inspection and mock-up approval, volume production for a 150–300 key property typically requires 30–45 calendar days, timed to coordinate seamlessly with ocean shipping schedules.
Do you accommodate phased deliveries for live hotel renovations?
Absolutely. Operating properties cannot shut down entirely. We pack and containerize panels and loose furnishings floor by floor or wing by wing, enabling your installation contractors to execute rolling turnovers without congesting loading bays or staging areas.
Ready to Engineer Your Hospitality FF&E Package?
Submit your architectural drawings, BOQ schedules, or concept sketches. Our senior joinery engineering team will supply an in-depth review, value-engineering recommendations, and budgetary quotation within 24 hours.
Inquire Now