Integrated Commercial Hospitality & Wall Furniture Systems
Engineered for four-star and five-star commercial projects, our factory fabricates architectural acoustic paneling, full-height decorative wood claddings, and cohesive fixed room casegoods tested against rigorous wear-cycle parameters.
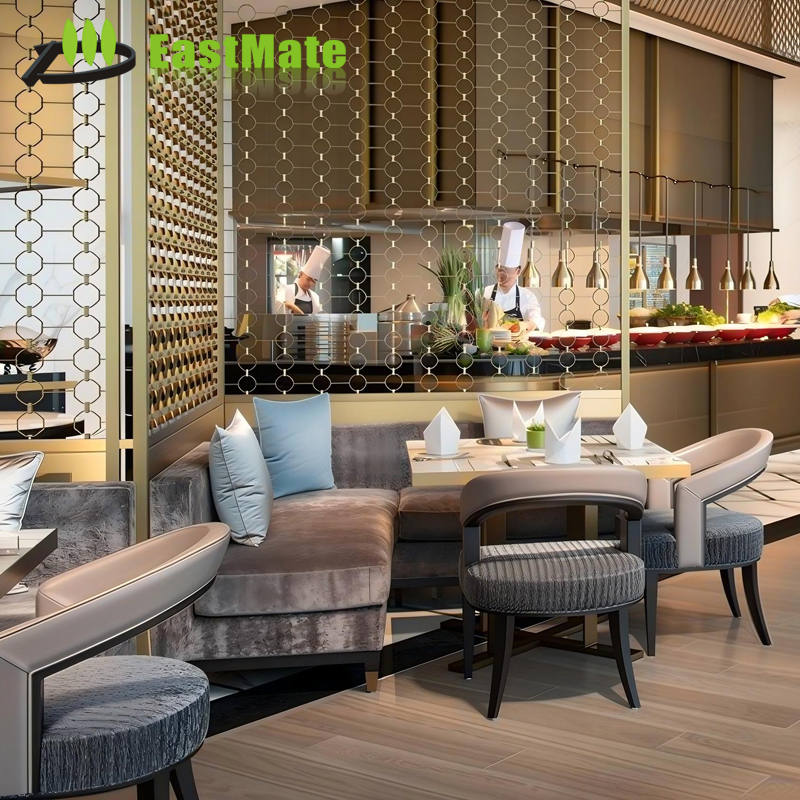
Modern Solid Wood Dining Table & Buffet Chair Set (4-Person)
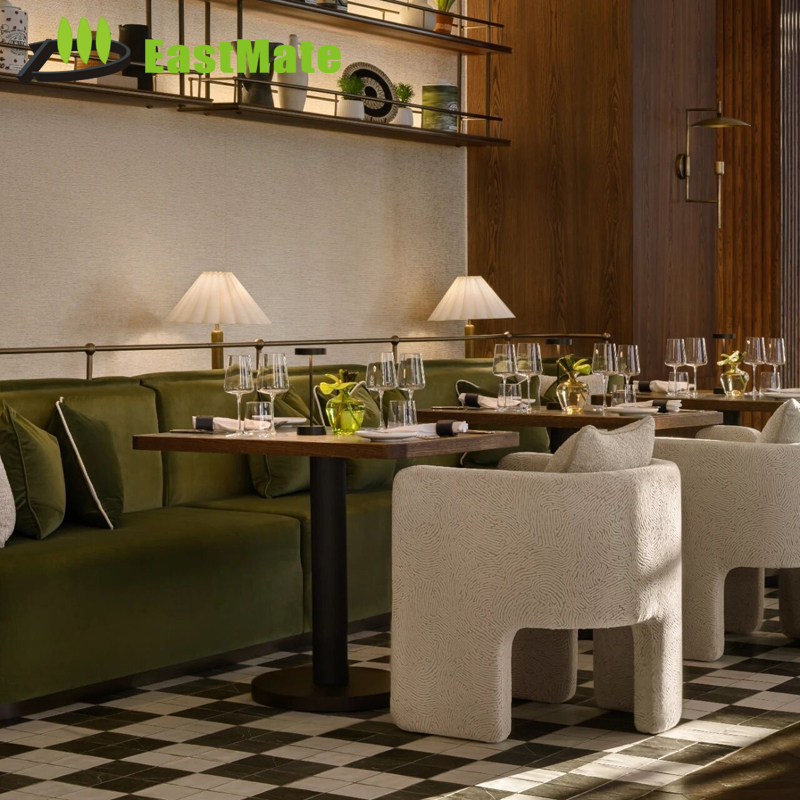
Commercial Solid Wood Stone Dining Sets with Acoustic Backing
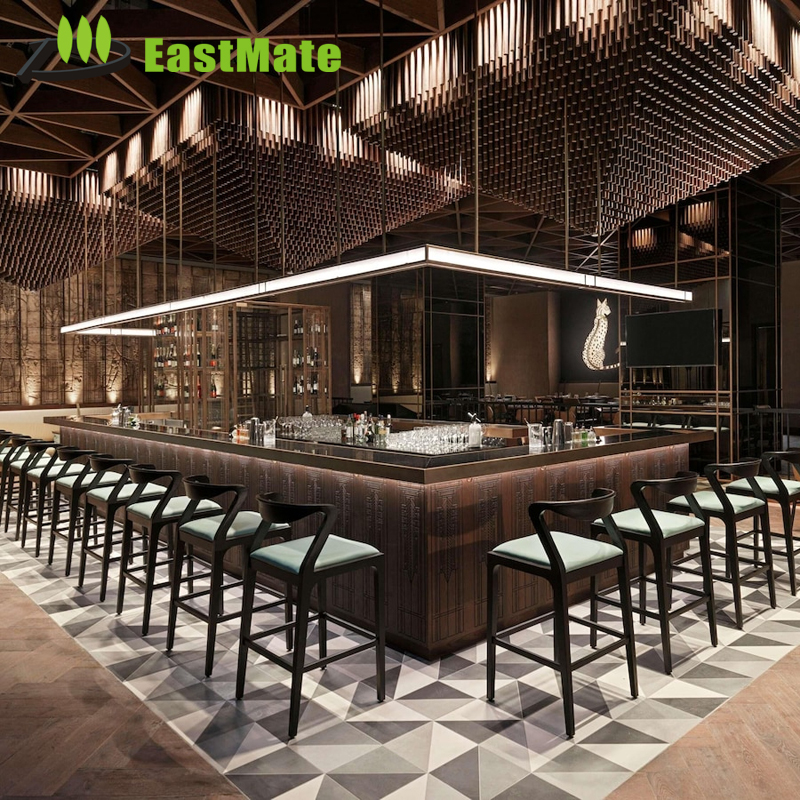
Luxury Solid Wood Modern Commercial Bar Chair – 5-Star VIP Series
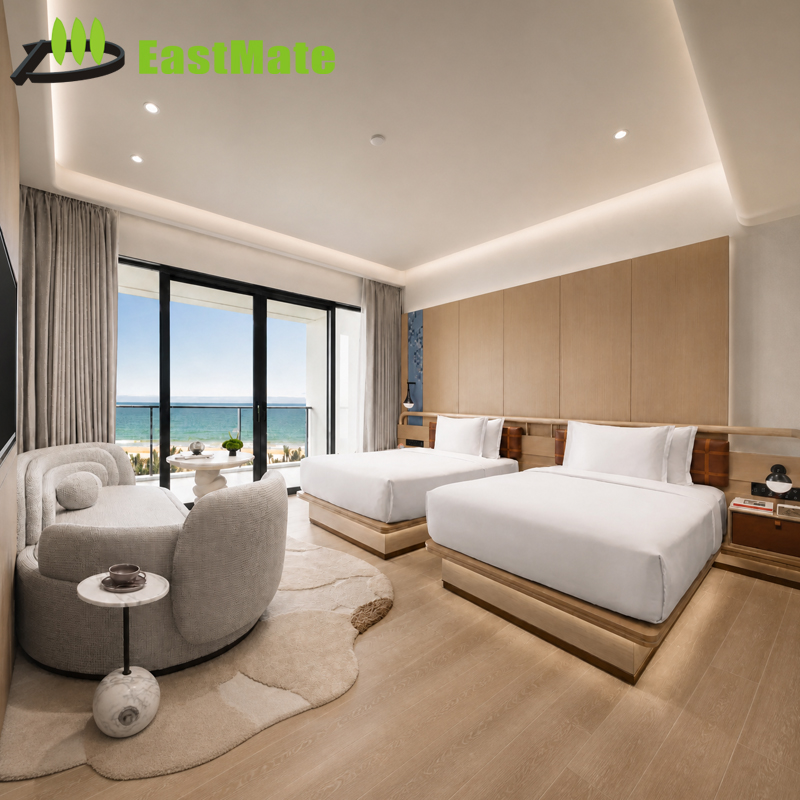
Full Guestroom Headboard Wall Paneling & Casegoods Suite
Architectural Cafe Counter Bar Stool with Solid Beech Base
Factory Bespoke Fabric Armchair with Solid Ash Frame
Square Solid Wood Restaurant Dining System (4-Seat Set)
Luxury Solid Wood Restaurant Dining Suite – Traditional Fluted Style
Top China Wood Wall Panels Factories & Exporters: The Engineering Paradigm
A rigorous examination of substrate stability, automated acoustic routing, surface veneer preservation, and sustainable chain-of-custody practices across South China's premier millwork corridors.
The international market for architectural interior cladding has undergone a structural transformation over the past decade. Where interior designers previously specified standard decorative laminates and solid-sawn timber boards on-site, modern commercial developments—specifically four- and five-star hotels, luxury residential compounds, executive corporate headquarters, and high-density mixed-use complexes—demand pre-engineered, factory-finished architectural wood wall panel systems. Foshan, located in Guangdong Province, stands as the global epicenter of this industrial advancement. Backed by mature timber logistics channels, advanced five-axis computer numerical control (CNC) machining centers, and an expansive network of specialist subcontractors, the Foshan furniture cluster has transitioned from traditional carpentry to hyper-precise architectural millwork manufacturing.
"Modern commercial interior architecture no longer treats wood wall cladding as an isolated decorative skin. Leading global project teams require wall panels to function as integrated technical assemblies—accommodating acoustic reverberation mitigation, concealed low-voltage LED raceways, hidden HVAC access reveals, and structural headboard mounting plates while strictly adhering to ASTM E84 Class A and EN 13501-1 Class B fire ratings."
For global procurement specialists, hospitality project directors, and general contractors operating throughout North America, Europe, Australia, and the Gulf Cooperation Council (GCC) region, navigating the ecosystem of China wood wall panels factories requires technical discernment. The divergence between low-tier local processors and export-grade industrial powerhouses—such as Foshan Hivke Hotel Furniture Co., Ltd.—lies in substrate stabilization protocols, precision moisture equilibrium control (regulating kiln-drying parameters to between 8% and 12% equilibrium moisture content depending on the installation latitude), adhesive performance under elevated humidity, and full-scale 3D shop drawing translation.
Substrate Engineering & Stability
Eliminating warping through balanced 5-layer and 7-layer cross-grain engineered plywood, high-density moisture-resistant MDF (HMR), and aluminum-honeycomb cores for ultra-tall vertical spans reaching up to 4.2 meters without bowing.
Acoustic Attenuation Technology
Micro-perforated front veneers (down to 0.5mm holes) paired with grooved rear acoustic chambers and bonded recycled PET acoustic fleece, delivering verified Noise Reduction Coefficients (NRC) between 0.75 and 0.90 for hospitality spaces.
Flame-Retardant Chemical Impregnation
Vacuum-pressure autoclave chemical treatment for real-wood natural veneers and flame-resistant PUR reactive adhesives that eliminate delamination risks under intense radiant heat while fulfilling stringent commercial fire testing mandates.
Future Procurement Trends in Architectural Wood Wall Panels (2026–2030)
How institutional property developers and international FF&E procurement houses are structuring specifications to mitigate logistics overhead, cut on-site trade hours, and hit carbon-neutrality targets.
Procurement workflows within commercial interior design are shifting rapidly from fragmented vendor purchasing toward integrated, single-source factory manufacturing. Where projects historically procured fixed wall claddings from local millwork sub-contractors and loose casegoods from separate FF&E suppliers, misalignment in wood species, color temperatures, grain orientations, and protective lacquer sheens consistently resulted in client rejection. The modern procurement standard demands single-point production orchestration.
| Evaluation Parameter | Traditional On-Site Millwork | Export-Grade Modular Wood Paneling | Compliance & B2B Benefit |
|---|---|---|---|
| Installation Sub-Structure | Field-cut timber battens; glued/screwed wet-fix. | Extruded aluminum Z-clip and interlocking French cleats with rubber dampeners. | 65% Faster Assembly Eliminates visible nail punctures. |
| VOC & Formaldehyde Emission | Solvent-borne field lacquers; variable off-gassing. | Automated UV-cured waterborne coatings; E0 / CARB Phase 2 compliant substrates. | LEED v4.1 Points Zero site odor; immediate occupancy. |
| Fire Performance Ratings | Topical spray-on fire retardants; prone to uneven coverage. | Factory vacuum-impregnated core + fire-barrier interliners tested to ASTM E84 Class A. | Code Guaranteed Full international laboratory test reports. |
| Dimensional Stability | Uncontrolled site humidity; prone to seasonal cracking and panel warping. | Laser-calibrated dry kiln conditioning (8-10% MC) with balanced backer veneers. | Zero Warping Tolerates HVAC cycling and desert/coastal climates. |
| Cable & MEP Integration | Manual hand-routing by on-site trades; risk of structural compromise. | CNC pre-machined internal wire ways, access hatches, and magnetic LED mounting channels. | Turnkey Precision Matches electrical schematics to the millimeter. |
Furthermore, environmental accountability has progressed from a marketing novelty to an uncompromisable contractual requirement. Major hospitality chains—including Hilton, Hyatt, and InterContinental Hotels Group—now stipulate verified FSC® (Forest Stewardship Council) Chain of Custody certifications for all architectural millwork packages. Simultaneously, European Union Deforestation Regulation (EUDR) benchmarks necessitate full traceability to harvest coordinates for solid timbers and veneers such as American Black Walnut, European White Oak, and African Teak. China's top exporters maintain documented chain-of-custody tracking across every log batch, ensuring smooth customs clearance at Rotterdam, Long Beach, and Jebel Ali.
Why International Procurement Teams Partner with Foshan Hivke
Engineering-driven, SGS-verified hospitality manufacturing located at the core of the Lecong industrial cluster.
An Engineering Powerhouse, Not a Middleman Broker
Established over 15 years ago, Foshan Hivke Hotel Furniture Co., Ltd. operates out of a modernized 38,690 m² production complex in Lecong Town, Foshan. The facility features comprehensive production lines dedicated to architectural joinery, automated veneer slicing and splicing, dust-free electrostatic finishing, and full-room loose furniture fabrication.
Our multi-disciplinary team of 249 full-time employees includes 26 dedicated CAD/BIM technical drafters, 18 veteran quality control inspectors, and senior project directors proficient in English, Spanish, and Arabic trade documentation. Before mass timber cutting commences, our shop-drawing team generates exhaustive 1:1 construction packages, cross-referencing floor plans, wall elevations, and mechanical MEP layouts to identify dimensional clashes before fabrication.
Crucially for multi-key hospitality renovations and high-stakes new builds, our facility maintains a dedicated Physical Mock-Up Room (MUR) Prototyping Workshop. Property owners and interior designers are invited to inspect full-scale prototypes—incorporating exact wood wall panel returns, integrated headboards, stone vanities, and loose casegoods—either on-site in Foshan or via high-definition multi-camera live video walkthroughs. This prototype milestone locks in veneer bookmatching, lacquer sheen percentages (from 5% dead-matte to 85% high-gloss piano finish), and joint tolerance before mass production commences.
Commercial Wood Wall Panels Procurement: Expert Answers
Technical guidance on moisture acclimation, fire testing, installation mechanics, and containerized export logistics.
How does your factory prevent wood wall panels from warping across different global climates?
Thermal and hygroscopic stability begins at the raw timber stage. All solid lumbers and core substrates undergo multi-phase computer-controlled dehumidification kilns to achieve an Equilibrium Moisture Content (EMC) of 8% to 10% for North American and European destinations, or 10% to 12% for tropical regions. Furthermore, every decorative front veneer is counter-balanced with an identical tension-balancing backing veneer on the panel's reverse side, neutralizing directional pull and keeping panels flat.
What fire-retardant certifications can be provided for hotel corridor and guestroom paneling?
We supply wall panel systems tested and certified to ASTM E84 (Class A Flame Spread Index ≤ 25, Smoke Developed Index ≤ 450) for the United States, as well as EN 13501-1 (Class B-s1, d0) for European and British commonwealth territories. Our production line incorporates vacuum-impregnated non-combustible mineral cores and flame-retardant PUR adhesive layers that prevent fuel contribution in the event of an internal structure fire.
What mounting substructures are recommended for rapid, screwless site installation?
We engineer concealed mechanical hanging assemblies utilizing precision-extruded aluminum Z-clips and continuous split-batten French cleat tracks. Wall panels arrive pre-routed on the rear face to accept the clips, allowing on-site installers to hook panels directly onto laser-leveled horizontal wall rails without surface face-nailing or messy wet adhesives. This cut on-site trade hours by more than 60% and enables non-destructive removal for future maintenance.
What is the standard production timeline for a 200-key hotel wall panel and casegoods package?
Following receipt of architectural CAD drawings, our technical drafting office generates detailed shop drawings within 10 to 14 business days. Material finish swatches (veneer, metal trims, fabric) are couriered concurrently. Physical mock-up room fabrication requires 21 to 28 days. Once the mock-up is signed off, full mass production for a 200-key project takes approximately 35 to 45 calendar days, supported by our 38,690 m² continuous production capacity.
How are delicate architectural fluted panels and wood veneers protected during maritime freight?
Finished panels undergo a 5-tier packaging protocol: (1) peelable surface protective film against micro-abrasions, (2) corner guard reinforcements made of dense high-impact plastic, (3) 10mm EPE pearl foam wrapping, (4) heavy-duty 5-ply corrugated export cartons marked with floor/room identification, and (5) fumigated solid plywood perimeter crates with internal silica desiccant bags to prevent moisture absorption inside ocean containers.
Can you manufacture custom acoustic paneling with specific NRC sound absorption metrics?
Yes. We engineer grooved and micro-perforated acoustic panels calibrated to specific acoustic absorption frequency bands. By varying the perforation pitch (such as 16/16/2 or 8/8/1) and bonding high-density acoustic backing felt (SoundTex or equivalent), we reliably achieve laboratory-verified NRC ratings from 0.75 up to 0.90, ideal for hotel conference centers, cinema halls, ballrooms, and luxury hotel presidential suites.