Guestroom Suite
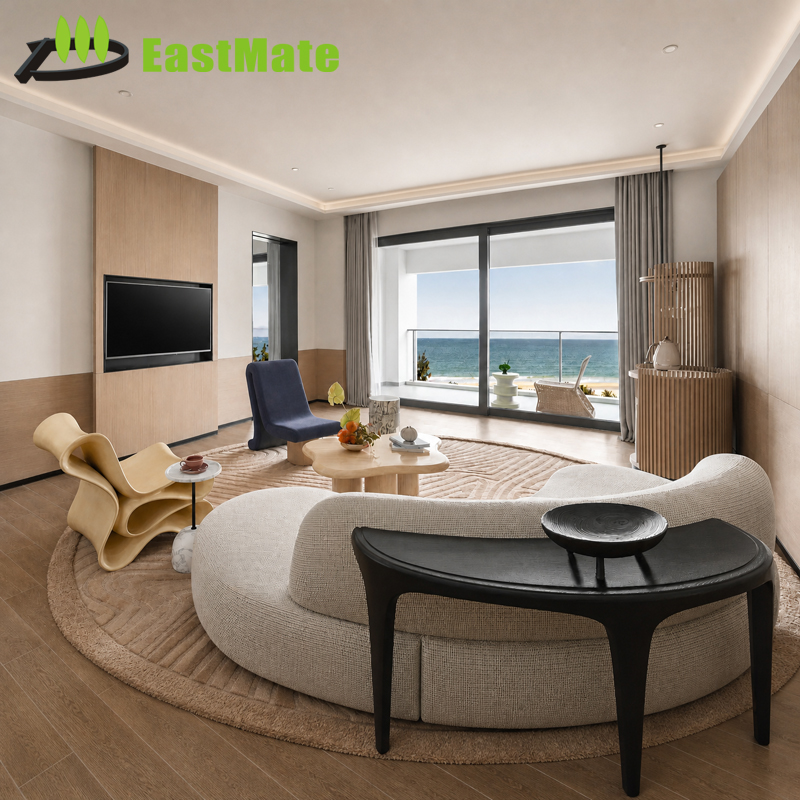
Manufactured in our 38,690 m² facility in Lecong, Foshan. Each casegood, wardrobe cabinet, bedside unit, and dining piece is produced under strict E1/CARB P2 emission standards and heavy commercial durability tolerances.
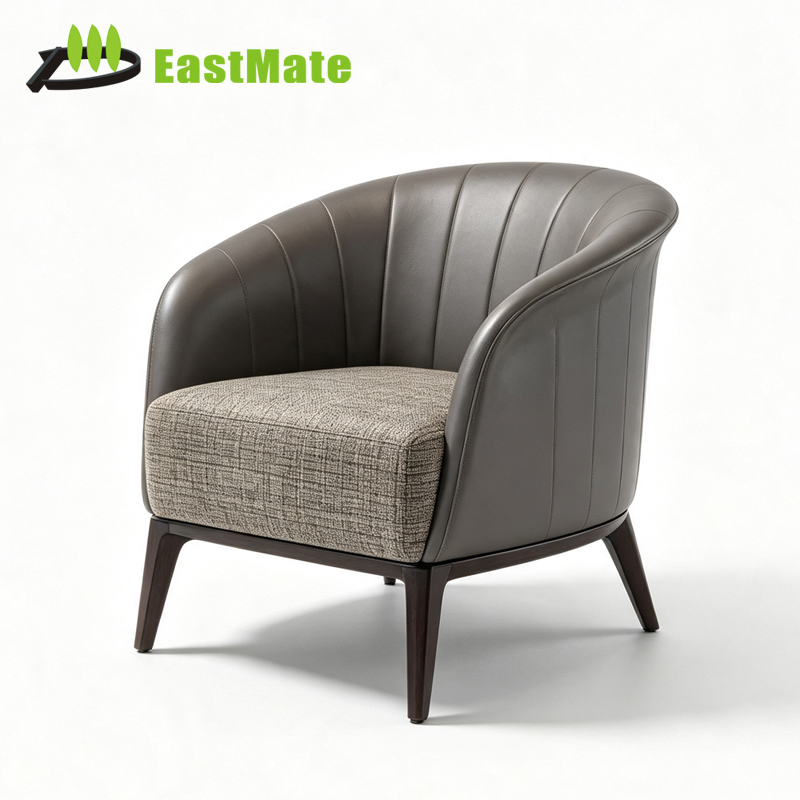
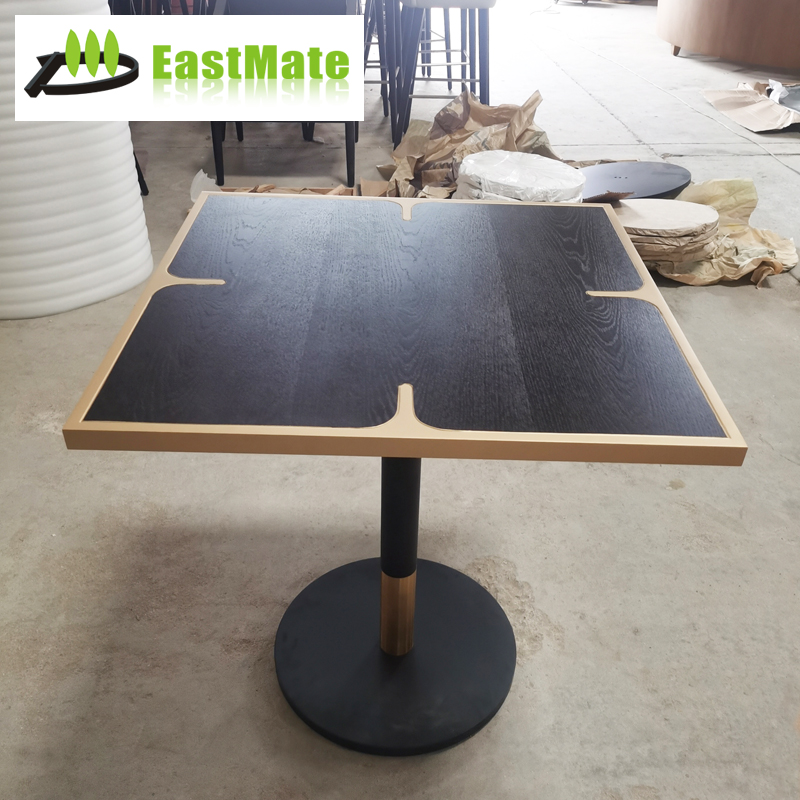
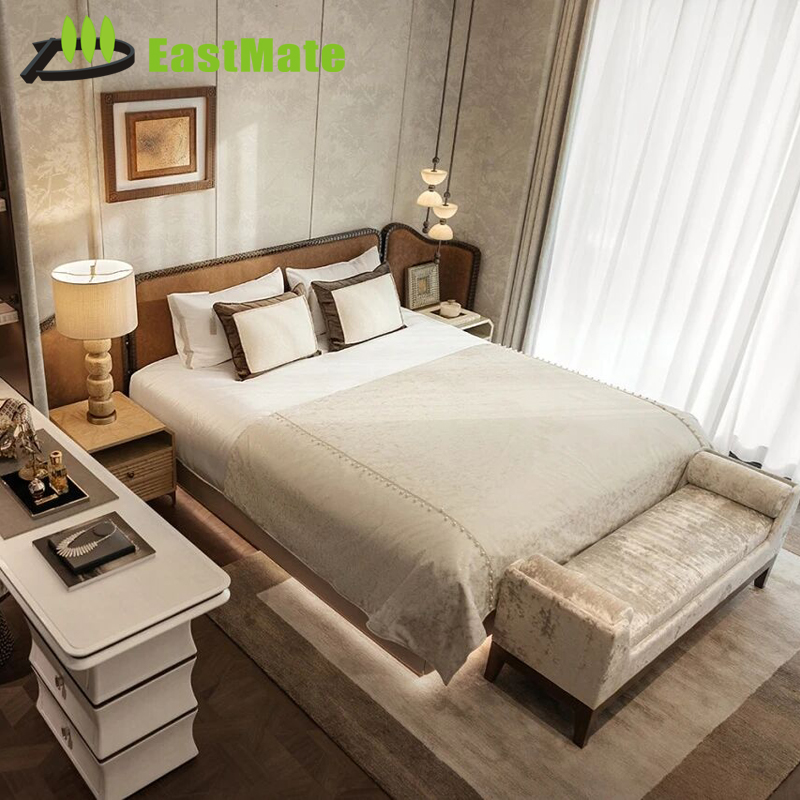
A hotel guestroom wardrobe or credenza cabinet is subjected to 10× more abrasive usage, climatic variability, and mechanical impact than residential joinery. Understanding engineering specifications prevents premature veneer peeling, structural sagging, and maintenance downtime.
We mandate multi-layer marine/birch core plywood engineered with 8% to 10% balanced moisture content equilibrium. This prevents dimensional warpage in humid island resorts or dry continental air-conditioned suites.
Delamination at door edges is the leading reason for guestroom refurbishment. We deploy advanced PUR (Polyurethane Reactive) adhesive and laser-fused edging technology to guarantee waterproof, moisture-impenetrable seams.
Every hinge, sliding door track, and drawer runner undergoes minimum 80,000 to 100,000 cycle testing. We integrate synchronized undermount soft-close slides capable of supporting 45kg dynamic working loads.
Located in the heart of Lecong, Foshan—the world's foremost furniture manufacturing cluster—Foshan Hivke Hotel Furniture Co., Ltd. has spent over 15 years perfecting the exact translation from interior designer CAD renderings into millimeter-accurate built environments.
Operating across an independently audited 38,690 m² facility with 249 skilled technical craftsmen, we bridge the gap between architectural aesthetic and high-volume value engineering. Our internal drafting office submits detailed 1:1 shop drawings, submittals, and material schedule sample boxes prior to committing timber to our automated CNC and UV lacquer lines.
Guest expectations are pivoting rapidly toward silent acoustics, tactile natural textures, contactless digital security, and seamless electronic device management. Discover how our factory pioneers these integrated innovations.
Integrated rear convective baffling and acoustic insulation eliminate vibration resonance. Cabinets feature concealed intake plinth louvers and rear exhaust channels maintaining ambient thermal equilibrium below 35°C without audible fan noise.
Nightstand cabinets and vanity desks feature embedded fast-charging Qi wireless inductive transmitters flush beneath natural stone or timber veneer, routed through fire-retardant internal conduit raceways.
Wardrobe millwork incorporates concealed heavy-gauge steel electronic safes with illuminated LED interiors, illuminated touch keypads, and motor-driven locking bolts integrated into reinforced double-wall carcase bays.
Precision-milled aluminum LED extrusions with 45° frosted micro-diffusers are recessed flush into hanging rails and shelf reveals, triggered via magnetic proximity sensors with warm 2700K–3000K circadian profiles.
Procurement directors and hospitality real estate developers are shifting focus from lowest first-cost to Total Cost of Ownership (TCO), ESG compliance, and modular life-cycle refurbishment efficiency.
Traditional rigid joinery required full room gutting during 7-year PIPs (Property Improvement Plans). Forward-thinking brands now mandate modular sub-chassis with quick-release fastener systems. Door fronts, drawer facades, and side gables can be swapped in under 15 minutes per key without removing the carcass.
Global operators (Marriott, Hilton, IHG, Hyatt) have codified rigorous Scope 3 sustainability targets. Suppliers must prove FSC Chain of Custody for all timber species and ensure finishes comply with LEED v4.1 interior air quality benchmarks using ultra-low-emission waterborne polyurethanes.
To curb unpredictable overseas contractor installation labor rates in the US, Europe, and GCC, hotel bedroom cabinets are engineered as self-aligning prefabricated pods. Built-in wiring looms, pre-hung doors, and leveling plinths cut on-site trade coordination hours by up to 40%.
A data-backed technical comparison to guide procurement teams in selecting the optimal carcass, surface layer, and edge protection based on hotel tier and climatic conditions.
| Substrate / Specification | Commercial Grade Plywood | High-Density Moisture-Resistant MDF | Standard Particle Board (MFC) | Hivke Recommended Best Practice |
|---|---|---|---|---|
| Screw Holding Capacity (Face/Edge) | 1,250 N / 980 N (Superior) | 1,050 N / 820 N (Good) | 720 N / 510 N (Risk of tear-out) | Multi-ply Birch/Eucalyptus Plywood |
| 24h Water Swelling Rate (%) | < 6.5% (Exceptional stability) | < 8.0% (Green core MR grade) | > 14.0% (Prone to swelling) | Plywood for bases; MR-MDF for carved doors |
| Bending Strength (MOR MPa) | ≥ 38.0 MPa | ≥ 30.0 MPa | ≥ 14.5 MPa | Heavy structural casegoods require ≥ 32 MPa |
| Edge Banding Durability | PUR Hot-Melt Zero-Line Joint | PUR or Laser Edging | EVA Glue Line (Visible glue line) | Mandatory PUR hot-melt prevents steam peeling |
| Ideal Hospitality Tier | Luxury 5-Star & High-Humidity Resorts | 4-Star & Boutique Lifestyle Hotels | Budget Economy & Extended Stay | Full Brand Standard FF&E Compliance |
How our engineering and production departments transform architectural ID packages into precision-delivered containers across hundreds of keys.
Detailed joinery review converting ID renderings into 1:1 CAD/Revit construction shop drawings detailing carcass construction, cable pathways, and tolerances.
Courier delivery of wood veneer swatches, open/closed-pore lacquer samples, solid surface cutoffs, brushed PVD metal trims, and hardware boards for approval.
Construction of full-scale bedroom prototype cabinetry at our Foshan facility. Designers & owners review proportions, hardware movement, and aesthetic alignment.
Computer-optimized panel cutting, boring, and mortise routing ensure zero deviation (<0.2mm) across high-volume batch runs for 50 to 500+ guestroom suites.
Hand-matched natural veneer pressing followed by multi-stage UV base coats and eco-friendly polyurethane topcoats cured in pressurized dust-free chambers.
Trial assembly of every wardrobe door, drawer runner, integrated minibar mesh, and headboard connection before packaging to ensure zero on-site fitting delays.
Multi-layer protection: EPE foam wrapper, heavy corner paper protectors, high-density honeycomb cardboard, and reinforced fumigated plywood crate encapsulation.
FOB, CIF, or DDP delivery coordinated with destination freight partners. Provision of detailed bilingual assembly manuals and remote/onsite engineer supervision.
Detailed technical, commercial, and operational clarifications designed to assist procurement directors, quantity surveyors, and project owners in mitigating manufacturing risks.
Get a QuoteSubmit your tender drawings, FF&E schedules, or concept renderings. Our engineering team will review technical details, propose cost-saving optimizations, and deliver an itemized factory quotation within 48 hours.