Featured Commercial Hospitality Collection
Custom-engineered casegoods, upholstered headboards, dynamic bed bases, and integrated dining systems manufactured to exact brand specifications and dimensional tolerances.
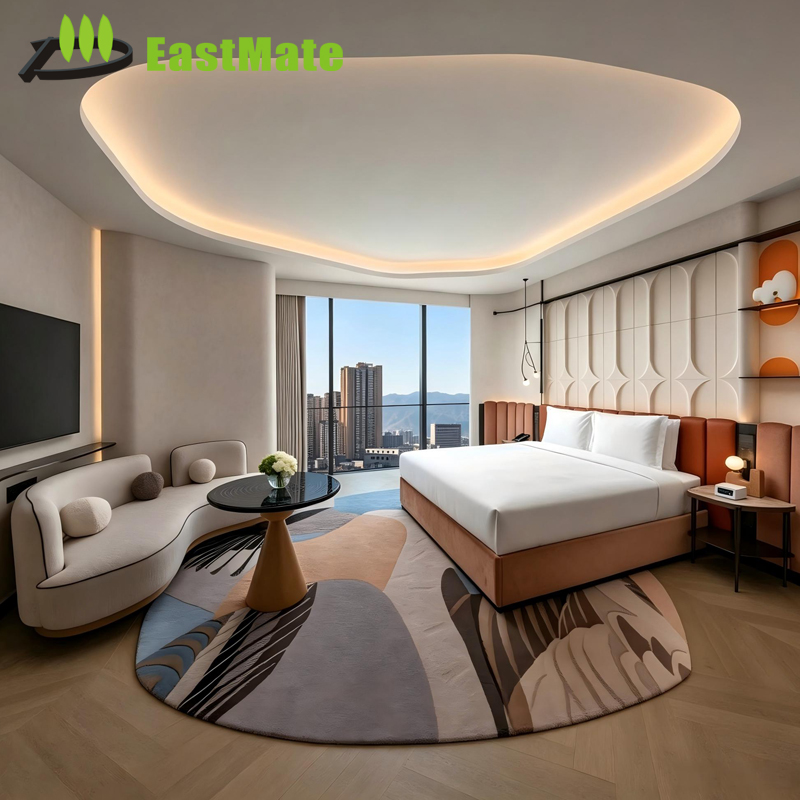
Engineered with an acoustic upholstered headboard, integrated nightstands, wardrobe closet, and media console tailored for modern luxury keys.
Product Details →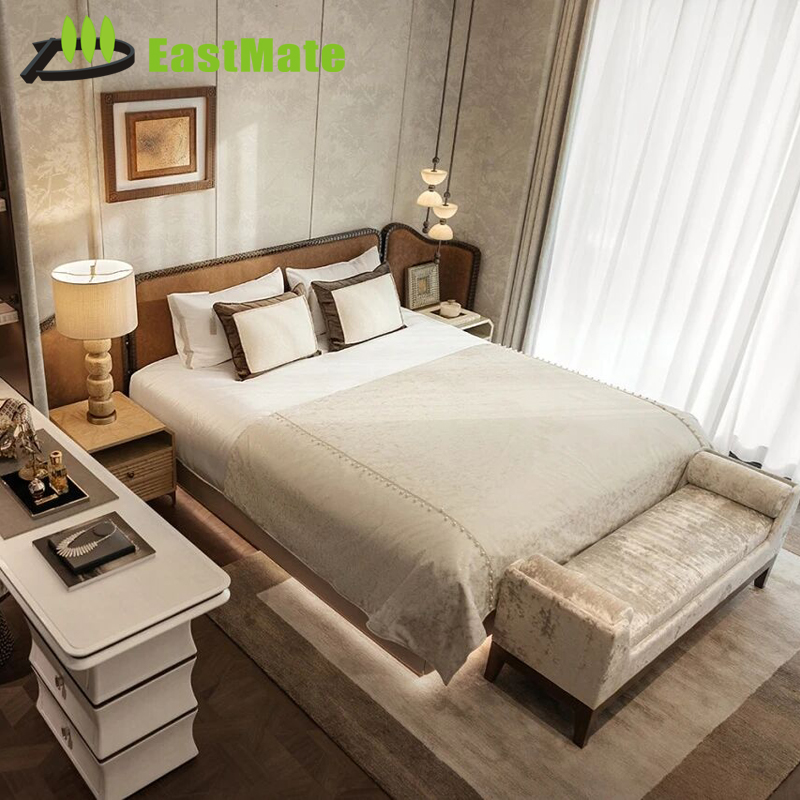
Features high-density foam padding compliant with BS 5852 fire resistance, accompanied by custom floating nightstands and a solid wood luggage bench.
Product Details →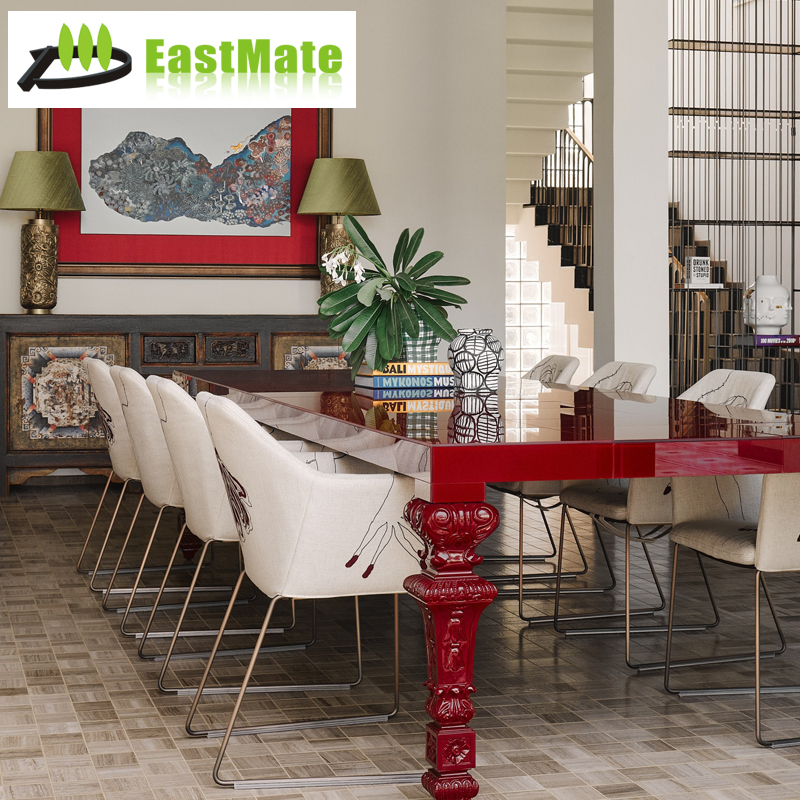
Heavy-duty 2m/4m solid timber construction finished with anti-scratch polyurethanes designed for hotel banquets, executive lounges, and dining areas.
Product Details →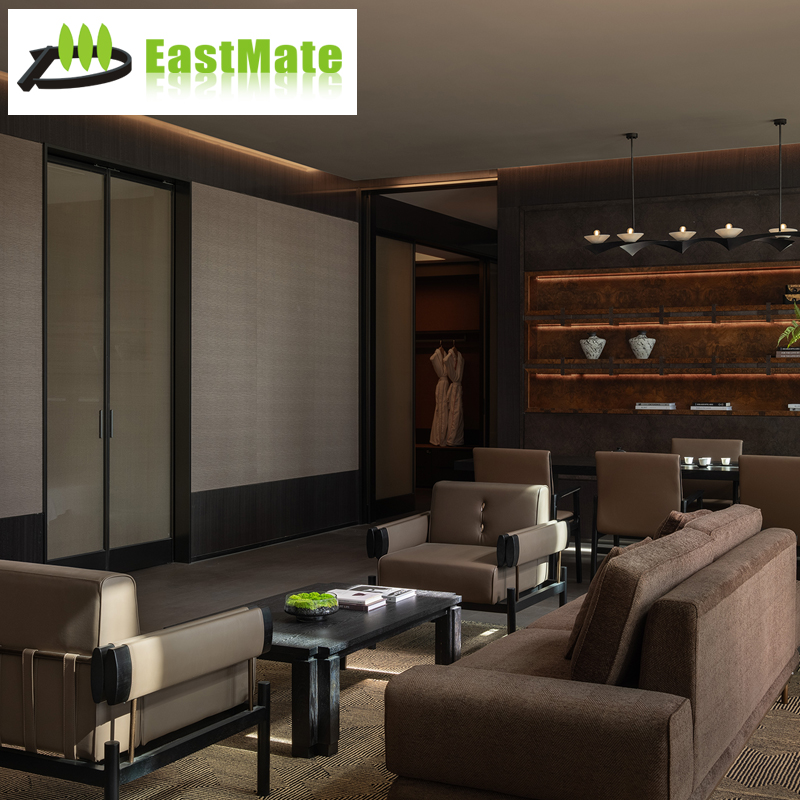
Deep ergonomic seating built for high-traffic hotel lobbies, serviced apartments, and presidential villa lounges with stain-repellent commercial fabrics.
Product Details →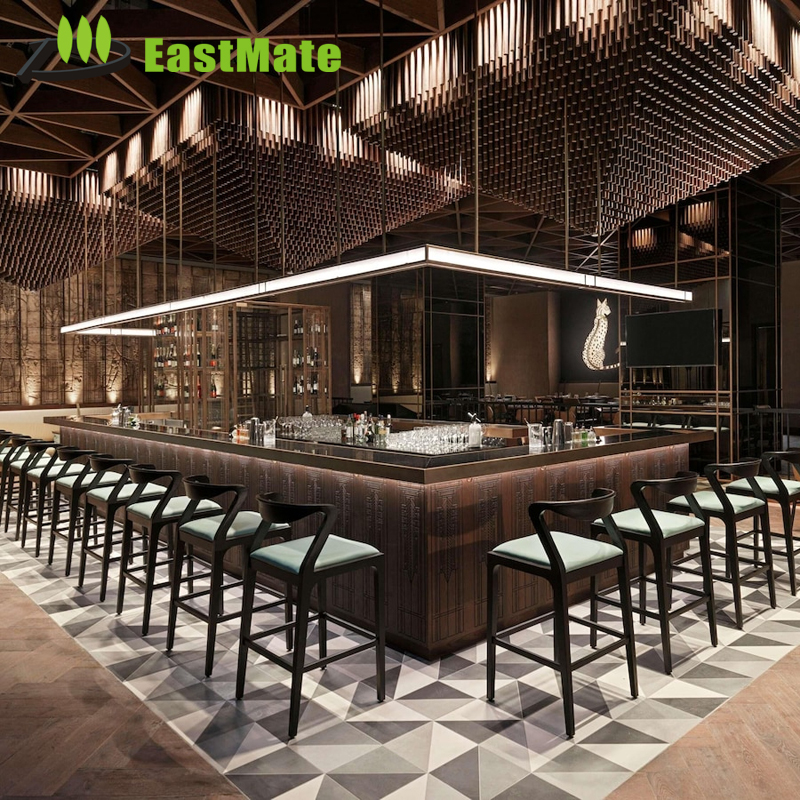
Precision-jointed solid hardwood frame featuring smooth polished lacquer and wear-resistant commercial upholstery designed for luxury hospitality bars.
Product Details →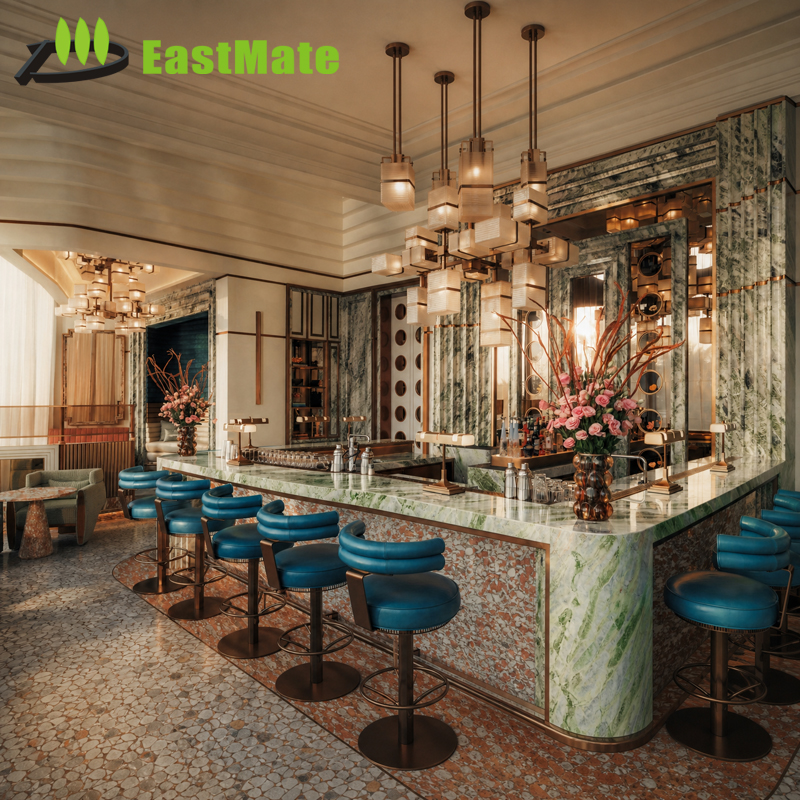
Reinforced steel or solid timber sub-base supporting calibrated high-resilience foam to prevent sagging in bustling cafes, bistros, and hotel bars.
Product Details →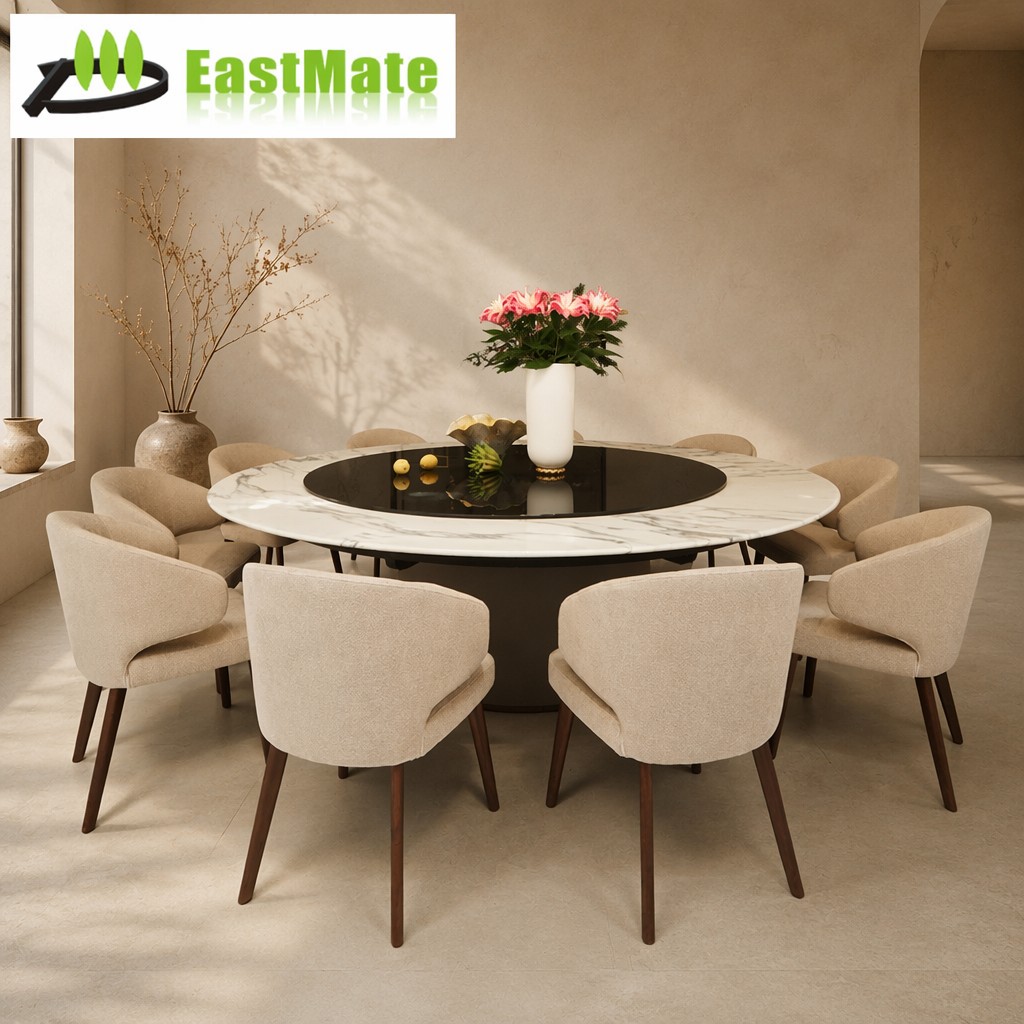
Classic craftsmanship meets commercial longevity; tested to withstand rigorous room service, restaurant traffic, and banquet hospitality use.
Product Details →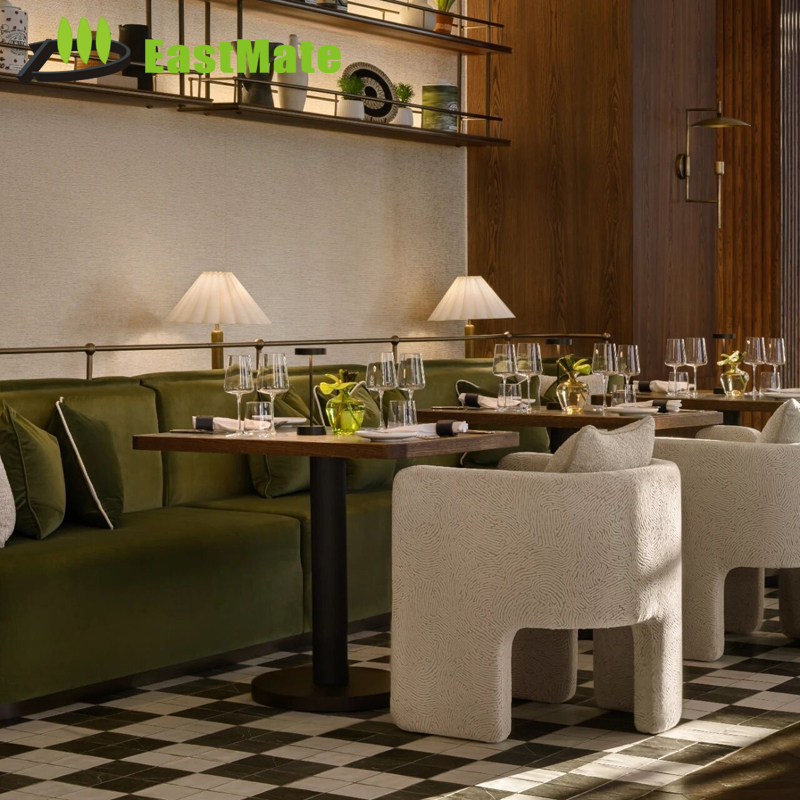
Engineered with high-tensile sintered stone or natural marble mounted on kiln-dried hardwood pedestals with resilient seating configurations.
Product Details →Emerging Trends Shaping Hotel Bed & Casegoods Procurement
A technical analysis of shifts in hospitality procurement, regulatory compliances, and FF&E engineering strategies driven by global property investors and operators.
Life-Cycle Cost (LCC) Over Initial Capex
Global operators are departing from fragile low-cost builds. Specification directors now prioritize durable structural joinery, mortise-and-tenon framing, and impact-resistant edge-banding. A commercial bed system that endures a 7 to 10-year refresh cycle without structural loosening delivers superior ROI compared to domestic-grade units.
Low-Voltage Smart Headboard Integration
Modern luxury hospitality projects demand seamless architecture where beds act as central electrical conduits. Specifiers integrate recessed low-voltage LED drivers, integrated USB-C / PD charging hubs, touchless master switches, and concealed wireless Qi transmitters directly inside upholstered acoustic backdrops.
Strict ESG, Low-VOC & Fire Compliance
Procurement teams serving North America, Europe, and the Middle East strictly reject non-certified sub-materials. Every substrate must meet E1 or CARB P2 formaldehyde limits, FSC-certified timber traceability, and fabrics passing CAL TB117 or BS 5852 Crib 5 flammability protocols without hazardous release.
Structural Developments in Commercial Hospitality Beds
How cutting-edge OEM/ODM manufacturers are re-engineering the mechanics of hotel beds to solve operational, housekeeping, and acoustic challenges.
Floating Cantilever & Recessed Bases
Modern architectural layouts prefer the aesthetic lightness of floating bed frames. We reinforce bed cores with heavy-gauge internal steel chassis and recessed plinths. This design eliminates guest toe-stubbing, speeds up housekeeping vacuuming routines, and accommodates perimeter underglow illumination.
Acoustic Dampening & Noise Isolation
Guest satisfaction scores correlate directly with room silence. Our OEM engineering integrates structural isolation gaskets, acoustic back-panel wall panelling, and non-squeak internal joinery. Bed foundations are engineered to absorb dynamic load impacts without micro-vibrations or audible joint creaks.
Modular Knock-Down (KD) Precision Systems
Shipping large luxury headboards and king-size bed frames across continents introduces severe freight costs and on-site damage risks. We develop precision CNC-machined KD hardware that packs flat into maritime containers and reassembles with zero visible fasteners in less than 20 minutes per room.
End-to-End OEM/ODM Manufacturing Capabilities
Operating from Foshan's premier furniture production cluster, Foshan Hivke Hotel Furniture Co., Ltd. combines fifteen years of manufacturing mastery with certified industrial engineering to bring bespoke FF&E packages to life on schedule and on budget.
Technical Shop Drawings & Rapid Mock-Ups
Our drafting engineers translate architectural renderings into production-ready millwork drawings and build full prototype mock-up rooms within 3 to 4 weeks.
Stringent Multi-Stage Quality Assurance
Raw timber moisture control, five-axis CNC tolerance checking, automated veneer pressing, and comprehensive trial assemblies before packaging.
Global Logistics & Phased Port-to-Site Delivery
Export crating, room-by-room barcode labelling, and systematic shipping schedules designed for rolling hotel renovations and new multi-key openings.
Frequently Asked Questions by Hotel Purchasing Teams
Clear, technical explanations covering manufacturing lead times, mock-up approval cycles, material certifications, and custom FF&E workflows.
Can your factory manufacture luxury hotel beds to custom brand FF&E standards?
Yes. As an authentic OEM/ODM manufacturer, we engineer guestroom suites and custom beds according to your designer's conceptual sketches, architectural drawings, and brand-specific FF&E guidelines (e.g., Marriott, Hilton, IHG, or independent boutique standards). We provide submittal drawings and finish boards prior to production.
What is the typical production timeline for an international hotel order?
Our typical workflow includes: 1 to 2 weeks for shop drawings and material sample submission; 3 to 4 weeks for prototype or mock-up room fabrication; and 30 to 45 days for full mass production, depending on key count, bespoke veneer complexity, and metal fabrication requirements.
Which core materials and finishes are utilized for luxury hotel bed frames?
We utilize commercial-grade, kiln-dried solid hardwoods (ash, oak, beech, walnut) combined with CARB P2 or E1-grade moisture-resistant plywood cores. Surfaces are faced with natural wood veneers, scratch-resistant polyurethanes, sintered stone, or PVD-coated stainless steel trims, paired with high-resilience flame-retardant foams.
How does your factory handle international flammability and emission standards?
All hospitality upholstery fabrics and padding foams can be tailored to meet destination compliance, including British Standard BS 5852 (Crib 5) and US California Technical Bulletin CAL 117. Timber and composite boards are sourced to comply with E1 or CARB Phase 2 low-formaldehyde thresholds.
Has your facility undergone independent third-party audits?
Yes. Foshan Hivke Hotel Furniture Co., Ltd. has passed rigorous onsite verification by SGS Group. The audit validates our 38,690 m² production workshop, workforce count of 249 personnel, quality control procedures, production capacity, and documented tier-1 supplier management systems.
How are goods packaged and labelled to ensure smooth on-site installation?
All items undergo export-standard packaging utilizing high-density EPE foam, corner edge-protectors, heavy-gauge corrugated cartons, and fumigated solid timber crates where required. Every carton is labelled by floor level, room key number, and item SKU to streamline unloading and on-site FF&E distribution.