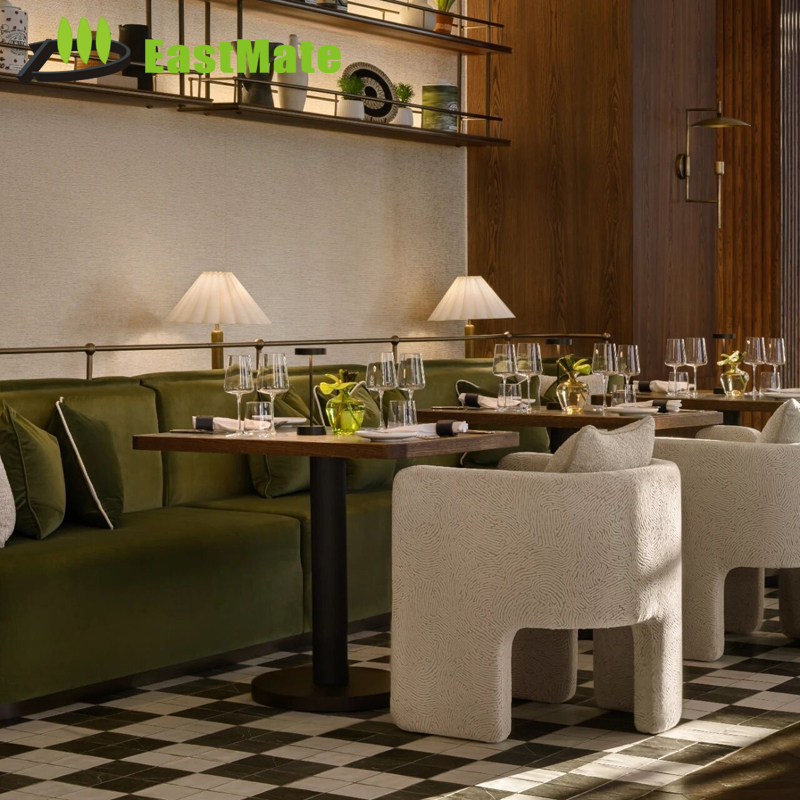
Export Showcase
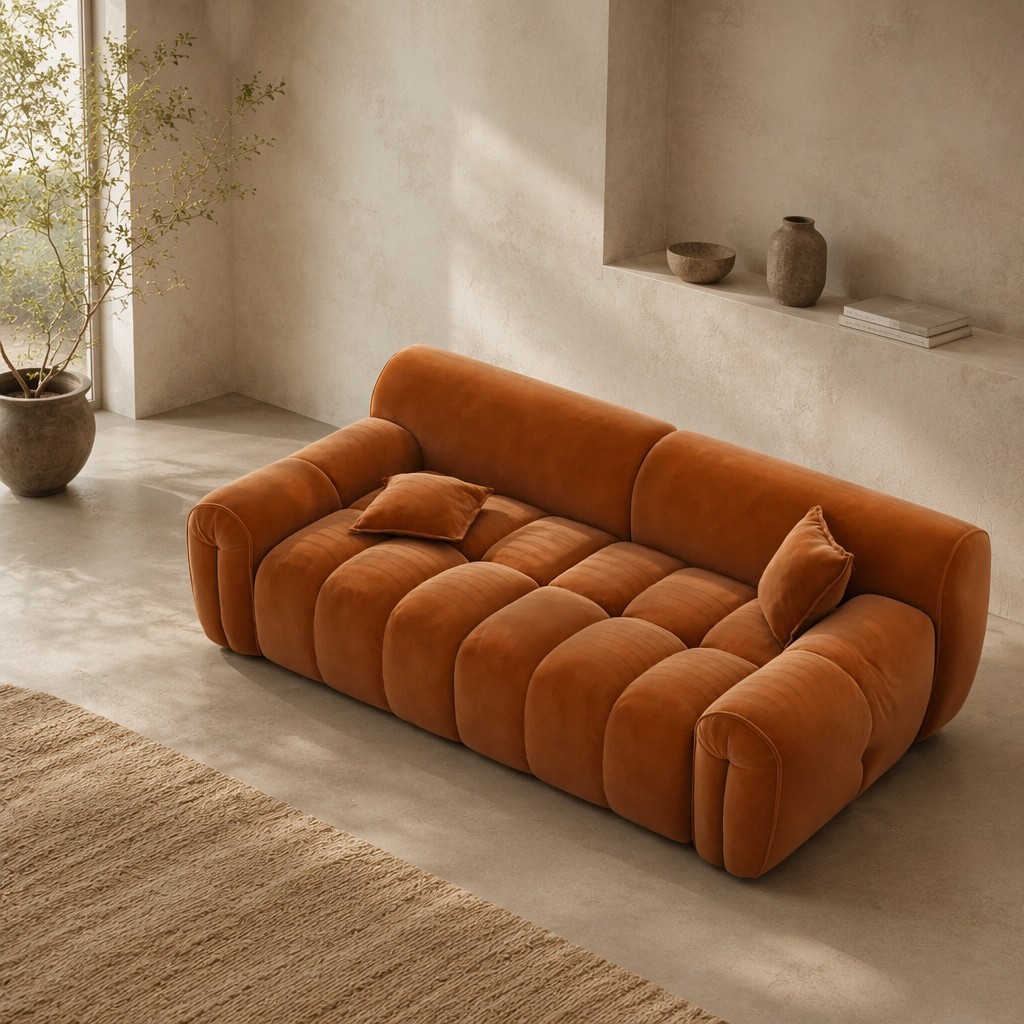
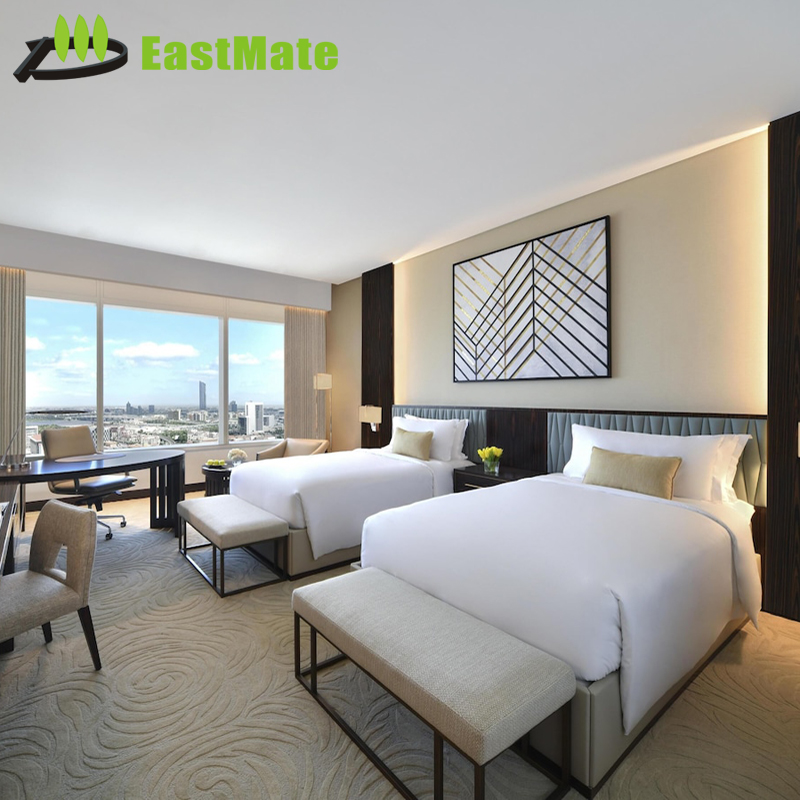
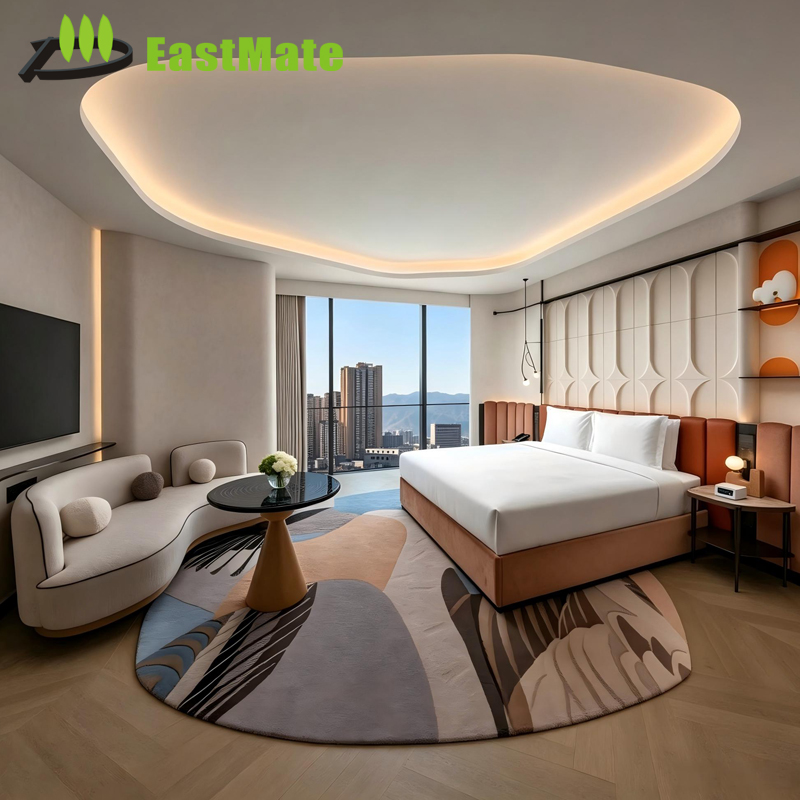
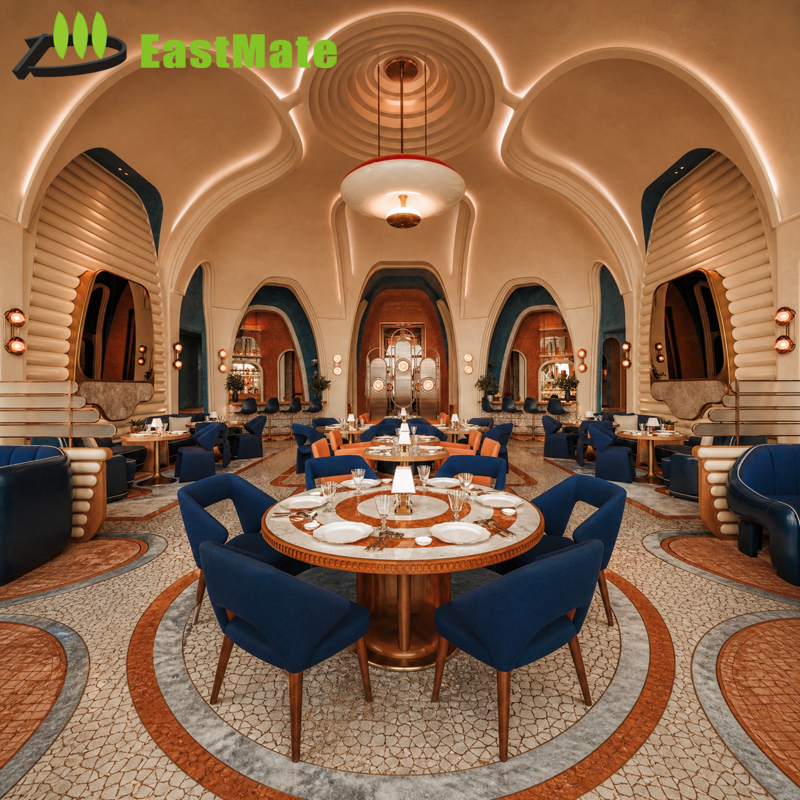
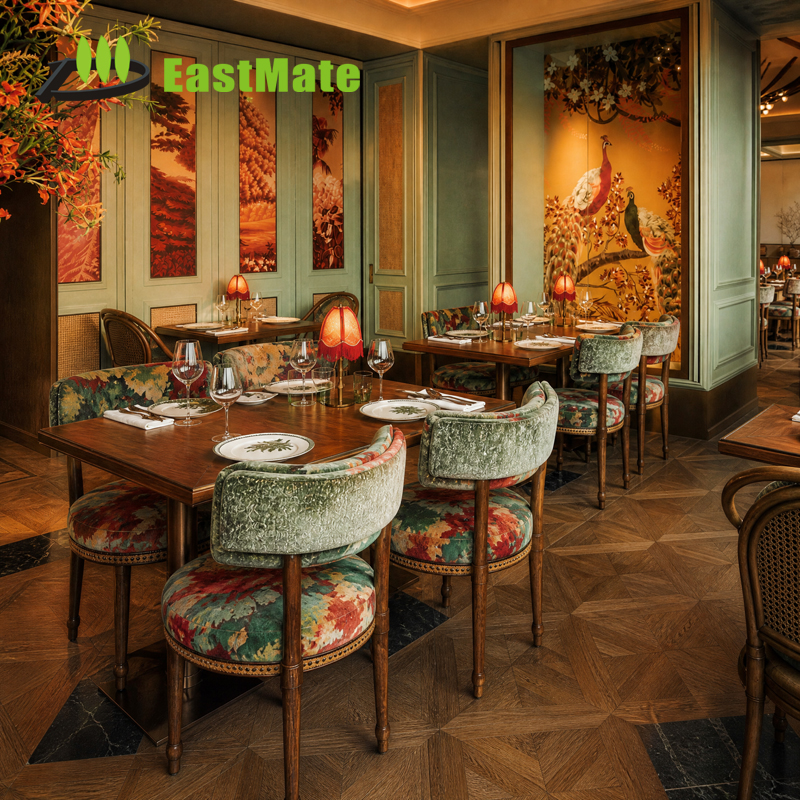
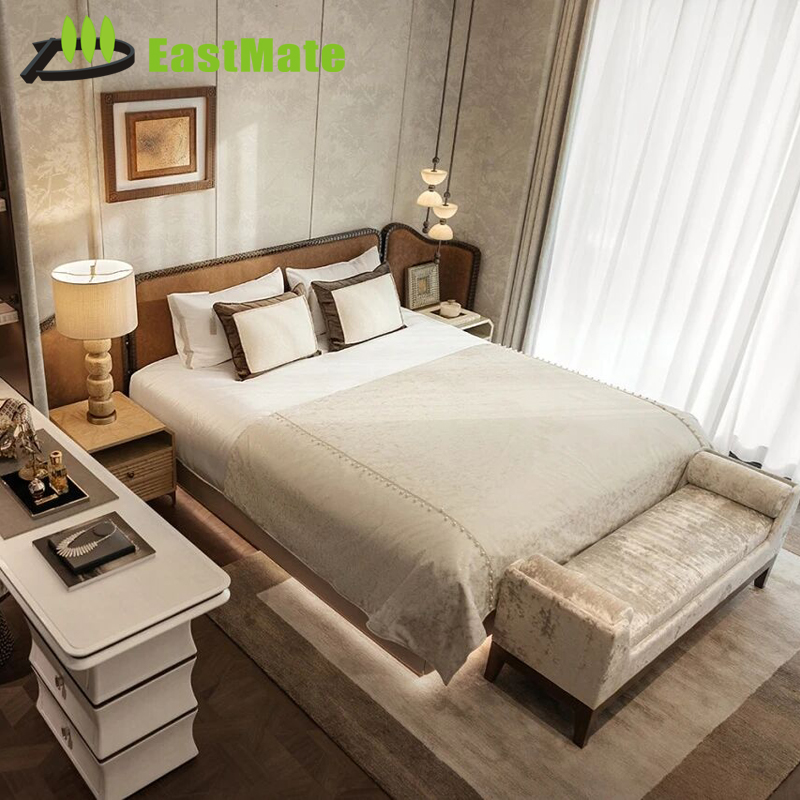
Featured Commercial Hotel Bed Suites & Contract Furniture
From reinforced solid hardwood framing to acoustic upholstered headboards and multi-functional hospitality casegoods, explore our precision-built collections engineered for high-turnover luxury environments.
Enterprise Credentials
Foshan Hivke Hotel Furniture Manufacturing Infrastructure
Situated in the heart of China's world-class furniture capital, Foshan Hivke Hotel Furniture Co., Ltd. operates an integrated 38,690 m² industrial facility engineered to meet high-volume luxury hospitality delivery cycles.
38,690 m²
Onsite SGS-Verified Facility
15+
Years International FF&E Track Record
249
Direct Engineers, Drafters & Artisans
80+
Audited Raw Material Supply Chains
Bespoke Shop Drawings & Rapid Mock-ups
Our in-house project drafting department translates designer schematics into fully dimensioned architectural shop drawings within 7–14 days. We eliminate site friction by detailing concealed wire raceways, MEP cutouts, wall anchor brackets, and exact structural joinery. We fabricate full 1:1 scale mock-up rooms in 3–4 weeks for client physical inspection and brand review before initiating mass production runs.
SGS Onsite Audited & Dual Verification
Clients operate with total institutional confidence. Hivke's production infrastructure, staff metrics, fire suppression protocols, and testing labs have undergone comprehensive on-site factory audits by SGS Group. We adhere to verified ISO 9001 quality management procedures across every processing node—from incoming timber moisture checks to final multi-point packaging inspections.
Rigorous International Code Compliance
Exporting across the United States, UK, EU, UAE, Saudi Arabia, Qatar, and Australia, we engineer wooden hotel beds compliant with regional statutory mandates. We provide low-VOC CARB Phase 2 and EPA TSCA Title VI certified composite core substrates, FSC-certified sustainable timber, BS 5852 / CAL TB 117 fire-retardant foams and textiles, and CE/UL certified integrated lighting harnesses.
Technical Whitepaper
Engineering Commercial Wooden Hotel Beds: Joinery, Deflection & Longevity
Unlike residential furniture, commercial hotel beds must withstand continuous cyclic loading, aggressive housekeeping cleaning protocols, and variable HVAC climate cycling across hundreds of keys.
Structural Frameworks & Wood Species Specification
In contract hospitality procurement, selecting the right wood substrate is a direct risk-management decision. While aesthetic exterior surfaces often showcase quartersawn White Oak, American Black Walnut, Ash, or Teak natural veneers, the concealed internal load-bearing skeletons demand species with superior shear strength and shock resistance. Hivke utilizes kiln-dried imported Russian Birch, European Beech, and Malaysian Solid Rubberwood for primary subframes, maintaining strict equilibrium moisture content (EMC) controls between 8% and 12% to prevent warping, twisting, or joint loosening when exported across varying global climates.
For large-scale panelized elements—such as monolithic headboard wall systems, integrated nightstand ledges, and floating platform aprons—we employ high-density E1-grade marine plywood or moisture-resistant MDF (MR-MDF) overbalanced with matching backer veneers. This balanced composite construction provides dimensional stability that outperforms solid timber panels over large surface areas, effectively eliminating expansion splits and seam cracks caused by shifting hotel air-conditioning loads.
| Substrate / Component | Material Specification | Engineering Benefit | Compliance / Standard |
|---|---|---|---|
| Internal Bed Base Skeleton | Solid Hard Beech / Russian Birch (FAS Grade) | High shock tolerance, shear load rating >850 kg, prevents lateral sway creaks | ASTM D143 Cyclic Load |
| Panelized Wall Headboards | 18mm–25mm E1 Multi-layer Plywood + Natural Veneer | Zero warping across 3m+ spans; superior screw holding for concealed french cleats | CARB P2 / EPA TSCA |
| Floating Bed Platform Base | Recessed Plinth with Heavy Gauge Powder-Coated Steel Box Rail | Eliminates guest toe-stub injuries; allows rapid housekeeping vacuum access | BIFMA X5.5 Commercial |
| Acoustic Upholstered Panels | High-Resilience Cold-Cured Foam (45–55 kg/m³) | STC sound dampening; maintains firmness without sagging after 50,000 compression cycles | CAL TB 117 / BS 5852 |
| Protective Top Coat Finish | Multi-pass Polyurethane (PU) / Water-Based UV Cured Lacquer | High resistance to chemical sanitizers, hot beverages, moisture, and scratch abrasion | ISO 4586 Scratch 3H+ |
Joinery Integrity: Mortise-and-Tenon vs. Knock-Down (KD) Hardware
A primary failure point in budget hotel beds is joint squeaking and corner deflection caused by improper mechanical fasteners. High-tier contract hotel beds manufactured by Hivke feature internal corner brackets fabricated from 3mm cold-rolled steel, double-doweled and mortise-and-tenon solid wood frames reinforced with heavy hardwood corner blocks glued and screwed in three planes. For export efficiency and container volume optimization, beds are designed with heavy-duty German Hafele or Titus eccentric KD connectors, allowing swift on-site installation by general contractors while maintaining the rigid monolithic feel of permanent factory joinery.
Strategic Sourcing
Future Procurement Trends in Wooden Hotel Beds & Casegoods
Hotel asset owners and interior design leaders are shifting procurement criteria. Sustainability benchmarks, smart room automation, and modular lifecycle repairability now govern vendor selection.
1. Decarbonization & Circular FF&E
Global operators such as Marriott, Hilton, and Accor are enacting aggressive Scope 3 emissions quotas. Procurement managers increasingly demand chain-of-custody FSC/PEFC certified timber, bio-based waterborne wood lacquers, and formaldehyde-free adhesives to fulfill LEED v4 and BREEAM building certifications.
2. Integrated Smart IoT Headboards
Modern luxury suites treat the bed backboard as the central nervous system of the guestroom. Factory-installed wireless fast-chargers, low-voltage recessed LED mood strips, motorized drape switches, and magnetic reading lights are now pre-wired with internal flame-retardant conduit channels before export.
3. Acoustic Zoning & Sound Insulation
With urbanization driving higher guest sensitivity to ambient noise, hotel beds increasingly feature wrap-around acoustic wingback headboards. By fusing perforated timber substrate backing with high-density flame-retardant wool blends, beds act as secondary sound absorption baffles within guestrooms.
4. Housekeeping-First Ergonomic Designs
Operational labor costs represent the single highest recurring overhead for hoteliers. Modern platform bed bases incorporate recessed cantilevered plinths, rounded radiused timber corners to eliminate guest shin strikes, and pneumatic mattress-lift assistance mechanisms that allow rapid fitted-sheet changes without straining housekeeping staff.
5. Modular Component Replaceability
Rather than replacing entire bedroom suites after cosmetic damage, asset managers now specify modular sub-assemblies. Hivke engineers snap-on upholstered headboard inserts, replaceable solid wood edge bumpers, and quick-swap nightstand drawer fronts, enabling hotel maintenance engineers to refresh rooms in under 20 minutes.
6. Biophilic & Tactile Organic Finishes
Reflecting guest wellness demands, high-gloss synthetic plastic coatings have been replaced by open-pore, matte biological wood stains that celebrate authentic grain character. Wire-brushed oak, fluted timber profiles, and raw natural textures bring soothing biophilic elements directly into urban guest environments.
Procurement Knowledge Base
Frequently Asked Questions by Hospitality Buyers
Clear, direct commercial answers addressing engineering tolerances, project timelines, container packaging, and factory verification for international procurement consultants.
Can Hivke manufacture custom hotel beds precisely to our designer's ID specs and drawings?
Yes. Over 90% of our production is fully custom OEM/ODM. We accept CAD schematics, 3D renderings, and FF&E schedules from interior design firms. Our engineering department develops comprehensive 1:1 shop drawings specifying all structural joinery, subframe profiles, hardware schedules, and finish formulas for client sign-off prior to prototype cutting.
What is the standard production timeline for a full hotel guestroom package?
A typical timeline proceeds as follows: Technical shop drawings and physical material sample submittals take 1 to 2 weeks. Physical mock-up room fabrication requires 3 to 4 weeks. Following client mock-up approval and finish sign-off, full container mass production typically completes within 30 to 45 days, depending on key count and finish complexity.
How does your factory prevent veneer delamination and timber cracking after export?
All raw lumber undergoes automated vacuum kiln-drying to stabilize moisture content between 8% and 12% before machining. We utilize hot-press hydraulic presses with moisture-resistant D3/D4 polyurethane glues for veneer bonding. Furthermore, we apply matching counter-balancing veneers on all panel backs to eliminate torsional stress and warping across divergent humidity zones.
What fire-retardancy and environmental standards can you certify for US/UK/EU orders?
We supply commercial fabrics and polyurethane foams certified to British Standard BS 5852 (Crib 5), American standard CAL TB 117-2013, and NFPA 260. Our engineered wood boards comply with CARB Phase 2, EPA TSCA Title VI, and European E1/E0 emission limits. Independent lab test certificates can be coordinated with SGS, Intertek, or TÜV upon request.
How are heavy wooden hotel beds and headboards packed to prevent ocean shipping damage?
All items receive five-layer export protection: high-density PE foam corner protectors, shock-absorbent EPE wrap, heavy-duty 5-ply corrugated carton boxes, and reinforced moisture-barrier polybags. Delicate stone, glass tops, or oversized monolithic headboards are crated in fumigated OSB plywood wooden crates. Each package features room-by-room barcode labels for rapid job-site staging.
Can you accommodate phased deliveries for live hotel wing renovations?
Yes. For existing hotel property refurbishments, we regularly coordinate sequenced production runs. Deliveries are packaged and dispatched floor-by-floor or wing-by-wing according to your general contractor's site handover schedule, ensuring your property maintains operational room revenues during ongoing renovations.
Launch Your Hotel Bed FF&E Engineering Review
Submit your CAD drawings, tender BOQ, or project specifications. Our dedicated technical project engineering team will deliver a comprehensive manufacturability review, material schedule, and factory-direct commercial quotation within 24–48 hours.