VIP Lounge
Explore contract-grade hospitality furniture packages built from kiln-dried hardwoods, structural multi-layer birch plywood, premium architectural veneers, and heavy-duty commercial hardware.
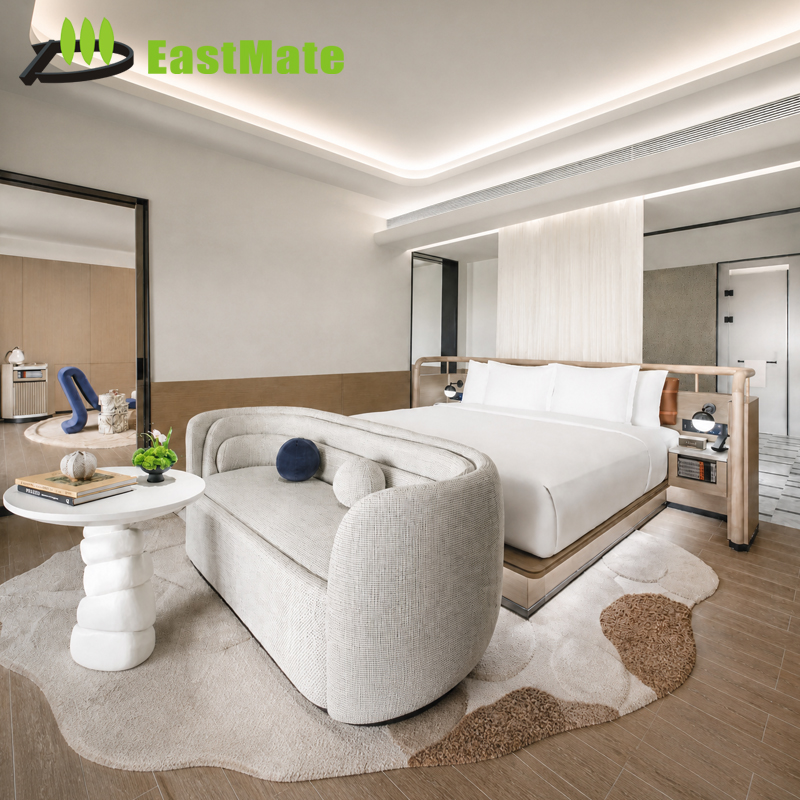
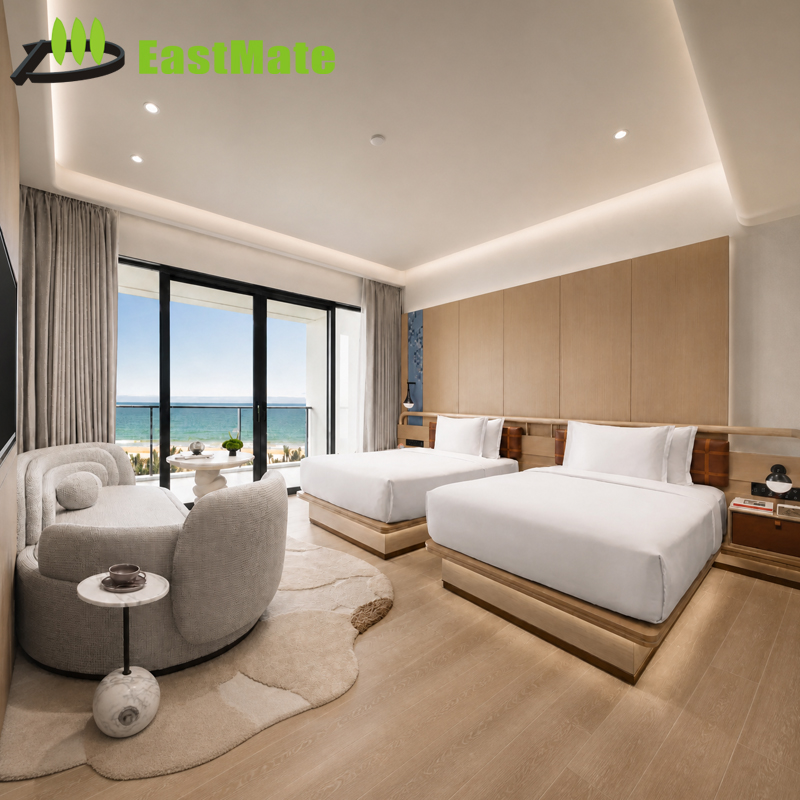
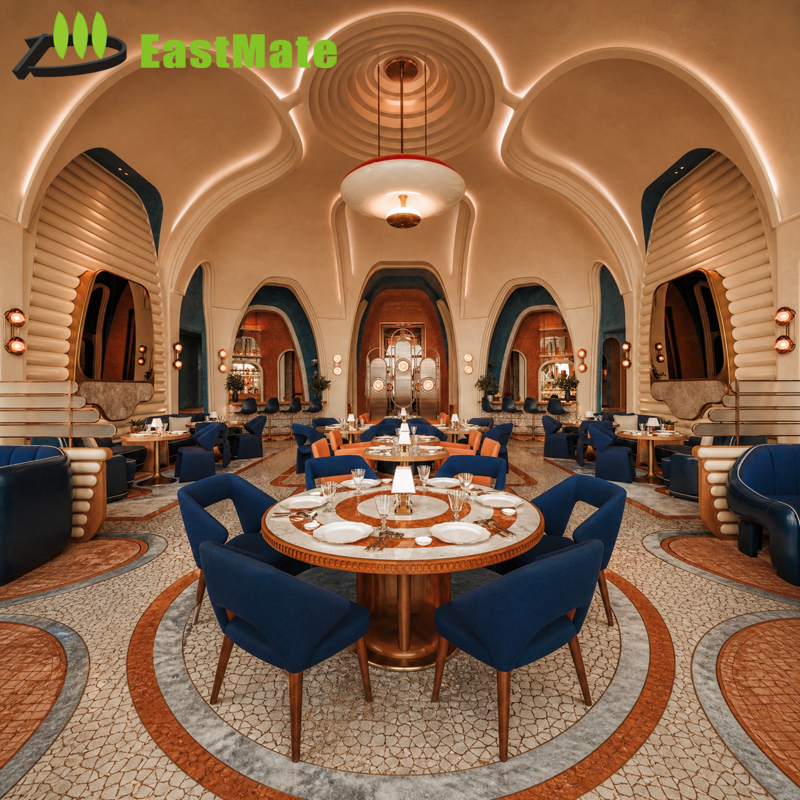
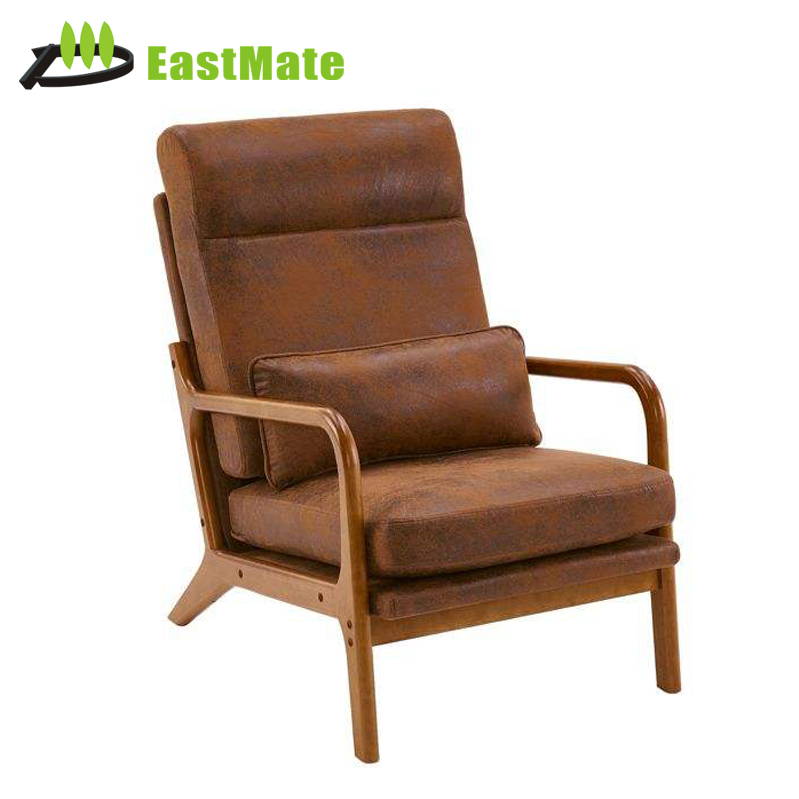
A comprehensive technical blueprint for procurement managers, hotel development operators, project directors, and interior architects specifying custom bedroom suites for high-traffic hospitality environments.
In contemporary luxury hospitality developments, procuring custom OEM hotel bedroom furniture sets represents a critical intersection between aesthetic vision, long-term operational durability, and financial return on investment (ROI). Hotel guestroom casegoods endure severe physical stress far beyond typical residential applications: continuous luggage impacts, chemical abrasion from rigorous daily housekeeping, unpredictable environmental humidity swings, and stringent regional life-safety compliance. As an experienced Foshan-based OEM/ODM manufacturing facility operating a verified 38,690 m² industrial facility, Foshan Hivke Hotel Furniture Co., Ltd. analyzes the architectural engineering paradigms, substrate integrity protocols, and manufacturing controls required to execute flawless casegoods packages across hundreds of hospitality keys.
The structural backbone of any hotel bedroom casegood—including platform bed surrounds, back-lit architectural headboard paneling, integrated luggage benches, executive work desks, and wardrobes—is determined by core board selection. High-humidity coastal resorts in tropical climates (such as the Maldives, Caribbean, or Southeast Asia) and dry, air-conditioned tower hotels across the Middle East present drastic hygroscopic challenges that will instantly warp inferior timber products.
Commercial-grade hotel furniture engineering utilizes E1 or CARB Phase 2 certified multi-layer eucalyptus and birch plywood for load-bearing vertical and horizontal panels. Unlike low-density particle board (chipboard), multi-layer cross-grain laminated plywood offers exceptional screw-holding strength (minimum 1,200 N on face, 900 N on edge) and virtually eliminates moisture-induced thermal expansion. For decorative curved components, laser-profiled elements, and paint-grade surfaces, Moisture-Resistant Medium Density Fiberboard (MR-MDF) treated with melamine urea-formaldehyde resin provides a high-density, uniform core that prevents edge swelling and post-finishing telegraphing.
Solid hardwoods—such as North American FAS-grade White Oak, Black Walnut, European Beech, or Ash—are strictly seasoned in industrial vacuum dry kilns down to an equilibrium moisture content (EMC) of 8% to 12%. Solid timber is strategically reserved for high-impact edge bands, plinth bases, structural chair legs, and heavy-wear framing. Solid wood perimeter lippings (sub-veneer solid timber borders of 10mm to 20mm thickness) are engineered onto case tops to ensure that repeated collisions with guest rolling luggage do not chip the surface veneer.
Understanding the technical differentiation between commercial tiers is vital for FF&E procurement consultants drafting tender specifications. The matrix below illustrates the performance benchmarks implemented in our engineering drawings:
| Component / Criterion | Standard Commercial / 3-Star | Upper Upscale / 4-Star Standard | Luxury 5-Star / Brand Flagship (Hivke Spec) |
|---|---|---|---|
| Primary Carcase Substrate | Standard E2 Particleboard / Hollow core | E1 Grade MR-MDF / Melamine Facing | E1/CARB P2 Multi-Layer Birch/Eucalyptus Plywood |
| Veneer Specification | Paper foil or 0.2mm engineered film | 0.45mm Reconstituted wood veneer | 0.6mm Natural Crown/Quarter Cut FAS Timber Veneer |
| Edge Treatment | 0.8mm – 1.0mm PVC hot-melt tape | 1.5mm ABS impact-resistant edge | Solid Hardwood Lippings (10-15mm) with PUR Adhesive |
| Drawer Slide Hardware | Bottom-mounted single extension slide | Side-mount ball bearing (35kg capacity) | Concealed Undermount Soft-Close (Blum / DTC 100k cycles) |
| Surface Finish & Sheen | Standard NC Lacquer, low scratch rating | Acid-Catalyzed (AC) Enamel | High-Solid Polyurethane (PU) UV-Cured, Zero-VOC 10-15 GU |
| Upholstery Life-Safety | Untreated commercial polyester | CAL TB 117-2013 compliant fabric | BS 5852 Crib 5 & CAL 133 Fire-Resistant CMHR Foam |
The global hospitality market is experiencing substantial transformation driven by digital guest integration, institutional ESG mandates, and compressed construction delivery schedules. Procurement directors must anticipate these shifts when establishing factory supply agreements:
Modern bedroom suites require frictionless tech integration. Nightstands and headboards now incorporate wireless Qi-charging induction modules hidden completely beneath 0.6mm natural stone or timber veneers, paired with integrated 65W USB-C PD conduits and concealed warm-dimming (2400K-2700K) LED architectural light channels with 90+ CRI.
Rising on-site labor costs across North America, Europe, and Australia have shifted procurement toward "Plug-and-Play" modular joinery. Wardrobes, minibar enclosures, and headboard wall claddings are pre-engineered in factory workshops with concealed French cleat hanging systems, allowing two carpenters to install an entire suite in under 4 hours.
Institutional hotel REITs and global operators (Marriott, Hilton, Accor, IHG) enforce strict sustainability disclosures. FF&E procurement contracts now require FSC-certified timber traceability, cradle-to-cradle recyclability, formaldehyde emissions well below E1 thresholds (≤ 0.05 ppm), and solvent-free waterborne finishing systems.
The procurement cycle has shifted from traditional 2D CAD drafting to integrated 3D BIM (Revit) modeling. Our in-house engineering team generates LOD 350 / 400 models that allow architects to detect MEP clashes (such as conduit boxes, plumbing chases, and HVAC registers) before the physical mock-up room is manufactured.
The visual signature of a luxury bedroom set relies on the precision of veneer matching and the chemical integrity of the protective coating. At Hivke's Foshan workshops, architectural veneers undergo meticulous book-matching, slip-matching, or reverse-diamond slip-matching depending on the designer's intent. Sheets are jointed using automated German splicing machines and bonded under high pressure (12–15 MPa) in heated hydraulic press lines using low-emission phenol-resorcinol adhesives.
Finishing is conducted in dust-free, positive-pressure automated spray lines. We apply multi-coat polyurethane (PU) or waterborne acrylic conversion systems that achieve extraordinary mechanical resistance:
Combining industrial-scale production capabilities in the heart of Foshan's furniture manufacturing cluster with deep international hospitality engineering expertise.
Our expansive industrial plant in Lecong Town, Foshan, has been audited on-site by SGS Group. Equipped with multi-axis CNC routers, automated edge banders, vacuum veneer presses, and positive-pressure clean finishing rooms to handle 500+ key orders without production bottlenecks.
Our 249-strong workforce includes a dedicated team of 32 drafting engineers. We translate initial design concept renderings and schematic floor plans into millimeter-accurate shop drawings, complete with hardware schedules, wire-routing chases, and cross-sectional joinery details.
Eliminate project risk before initiating full mass production. We fabricate a complete, 1:1 scale mock-up bedroom suite in 3 to 4 weeks, inviting owners, interior designers, and hotel brand inspectors to test ergonomics, finish fidelity, lighting ambiance, and structural rigidity.
Fully compliant with global contract safety benchmarks. We engineer upholstery with British Standard (BS 5852 Crib 5) or California Bulletin (CAL TB 117-2013) fire-retardant foams and fabrics. Integrated electrical components carry UL, CE, and SASO certifications for worldwide installation.
Minimizing job-site handling confusion is crucial. Every casegood unit is protected with 5-layer heavy corrugated cartons, edge angle guards, high-density EPE foam wrapping, and reinforced wooden crates. Packaging is systematically barcoded and labeled by room number and floor level.
Over 15+ years in high-end contract manufacturing, we have cultivated a robust ecosystem of 80 verified component suppliers. From Italian hardware mechanisms to specialized architectural metals and imported natural marbles, we deliver seamless multi-material integration under one roof.
Critical engineering, logistics, quality control, and warranty answers for purchasing agents, general contractors, and hospitality developers.
Climate adaptation begins with raw substrate stabilization. Solid timbers are kiln-dried to specific equilibrium moisture contents based on the destination: 8%–10% for arid environments like Saudi Arabia, UAE, and Qatar, and 10%–12% for humid coastal zones like Florida or the Maldives. Furthermore, we employ balanced lamination principles where both sides of any structural panel receive identical veneer or backing thickness to eliminate warping forces.
All exposed underside edges and rear panels are fully sealed with hydrophobic polyurethane back-lacquering or balance foil to prevent environmental moisture absorption. For tropical island properties, we upgrade all internal hinges, screws, and drawer slides to 304 or 316-grade stainless steel to prevent salt-air galvanic corrosion.
A standard project schedule flows through four distinct phases:
1. Shop Drawing & Material Submittals (Weeks 1–3): Engineering review, CAD/BIM detailing, and dispatch of timber veneer finish samples, lacquer color chips, marble swatches, and fabric control boards.
2. Mock-up Room (MOU) Prototyping (Weeks 4–7): Full prototype room assembly at our Foshan facility for client review, dimension verification, and adjustments.
3. Mass Production (Weeks 8–14): Upon MOU sign-off, mass cutting, CNC machining, edge profiling, finishing, and upholstery proceed at a throughput of 80–120 keys every 30 days.
4. QC & Staged Shipping (Weeks 15+): Pre-shipment packaging, crate crating, container stuffing, and export documentation handling.
Yes. Over our 15+ year manufacturing history, our engineering team has built guestroom suites, fixed joinery, and public area seating compliant with international hotel brand design criteria. We work directly with brand FF&E design manuals, ensuring compliance with required clearances, heavy-duty drawer weight ratings (exceeding BIFMA X5.5 standards), flame retardancy, and child-safety anti-tip hardware integration.
We maintain comprehensive documentation to provide third-party test reports for formaldehyde emissions (CARB P2 / E1), foam flammability (BS 5852 / CAL 117), and surface scratch resistance to ensure seamless sign-off by brand design directors.
To eliminate natural wood veneer shade variations across hundreds of guestrooms, we source entire wood veneer flitches from the exact same tree log batch. Flitches are categorized and sequenced so that each individual hotel floor receives synchronized grain character and tone.
Our Quality Assurance process operates four mandatory gates: Raw Material Inbound Inspection, White Body Dimension & Moisture Check (prior to finishing), Finish Sheen & Color Spectrophotometer Gate (against the approved client control master), and 100% Pre-Packaging Trial Assembly. Clients and third-party inspection firms (e.g., SGS, Bureau Veritas, TUV) are welcome to inspect units directly on our trial assembly lines.
We configure casegoods architecture according to the client's job-site labor costs and logistics budget. Typically, large architectural headboard panel systems, platform bed bases, and floor-to-ceiling wardrobes are engineered as optimized modular Knock-Down (KD) assemblies utilizing heavy-duty eccentric cam connectors (Hafele Minifix) and pre-drilled dowels. This optimizes shipping container cube utilization by up to 45%.
Conversely, nightstands, minibar sideboards, and lounge seating are predominantly shipped fully assembled with rigid glued and dowelled joints, allowing general contractors to position and commission pieces directly into guestrooms upon container de-stuffing.
All Hivke custom hotel bedroom furniture sets carry a comprehensive 5-year commercial warranty against structural defects, joinery failure, veneer delamination, and hardware breakdown under standard hospitality operating conditions. We provide a 1% spare parts kit (extra drawer slides, handles, hinge sets, edge touch-up pens, and touch-up lacquer kits) with every ocean container shipped.
For large-scale developments (300+ keys), we can dispatch bilingual on-site installation supervisors to guide the local installation contractor, ensuring millwork is installed to factory-specified tolerances.