High-Performance Hospitality Furniture Solutions
Engineered for high-traffic durability, acoustic dampening, and aesthetic consistency. Each casegood, dining unit, and upholstery assembly is fabricated to pass rigorous BIFMA, EN 16139, and BS 5852 standard certifications.
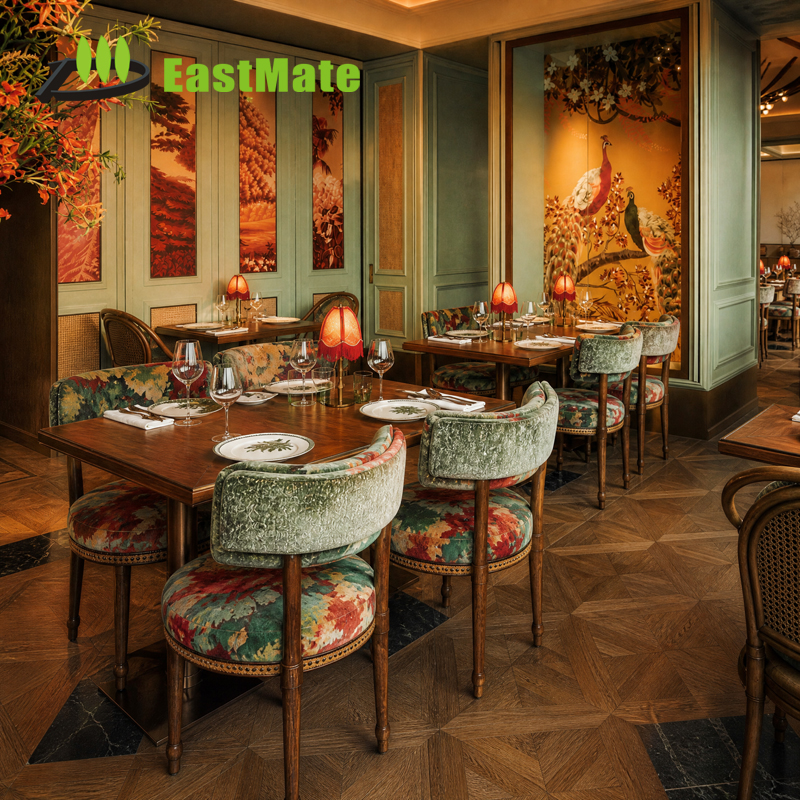
Durable Wood Restaurant Dining Set Square Table
Solid ash framework integrated with high-density flame-retardant foam cushions designed for all-day dining resilience and heavy seat turnover.
- Wood: Kiln-Dried Ash
- Foam: 45D High Resilience
- Finish: Anti-Scratch PU
- Use: Bistro & Buffet
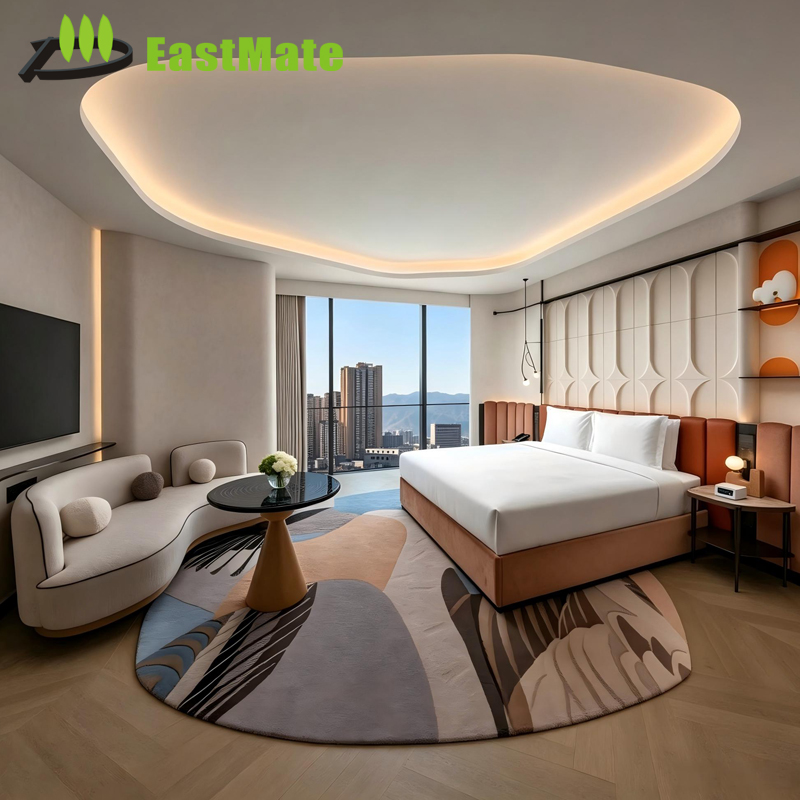
Modern Luxury Hotel Bedroom Furniture Set King Suite
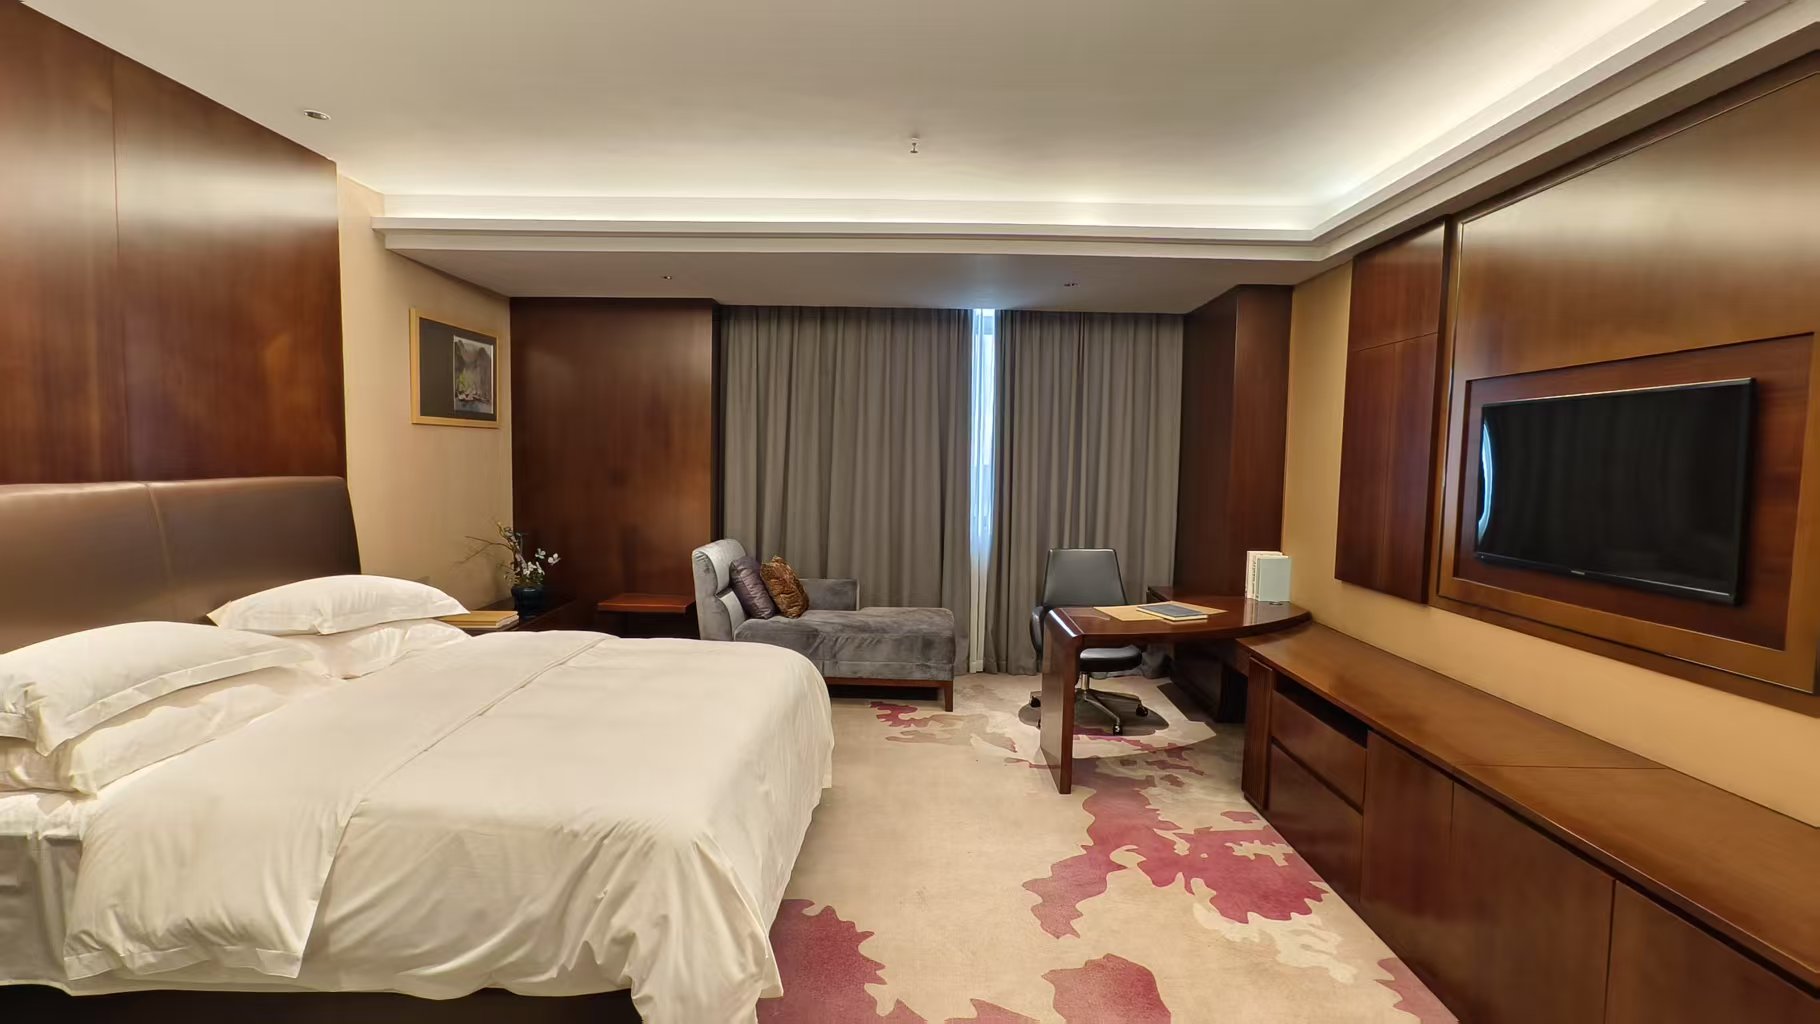
Architectural headboard with acoustically isolated wall paneling, integrated wireless charging nightstands, and E1 grade moisture-resistant wardrobe.
- Core: E1 Plywood/MDF
- Veneer: Natural Walnut
- Hardware: Blum Soft-Close
- Tier: 4-Star / 5-Star
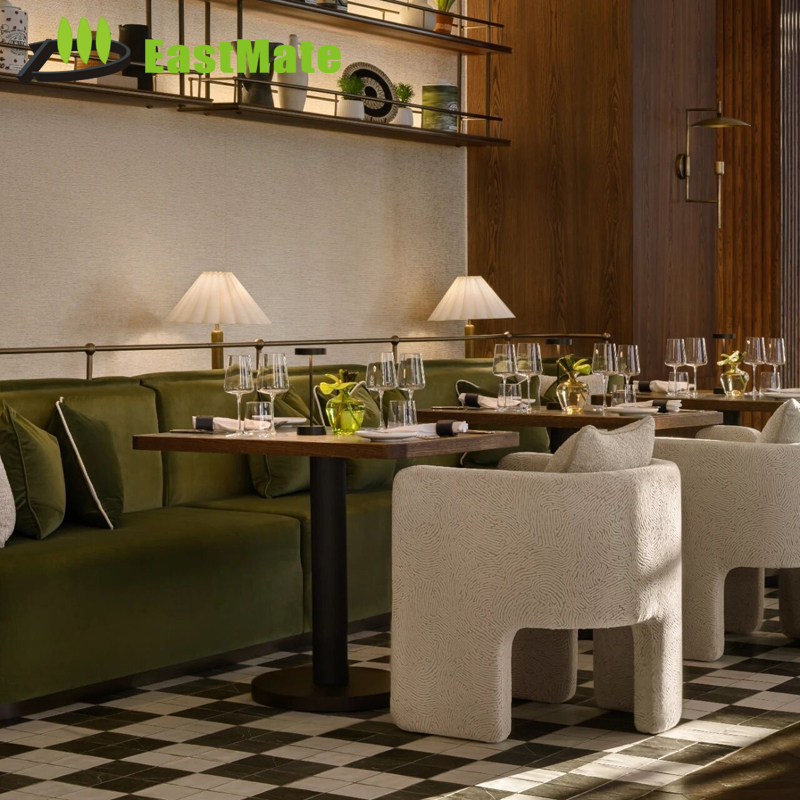
Commercial Solid Wood Dining Sets with Stone Top
Stain-proof engineered quartz and sintered stone tabletop supported by reinforced kiln-dried oak understructures for executive banquet areas.
- Top: Sintered Stone
- Base: Solid White Oak
- Upholstery: Easy-Clean PU
- Load: Heavy Contract
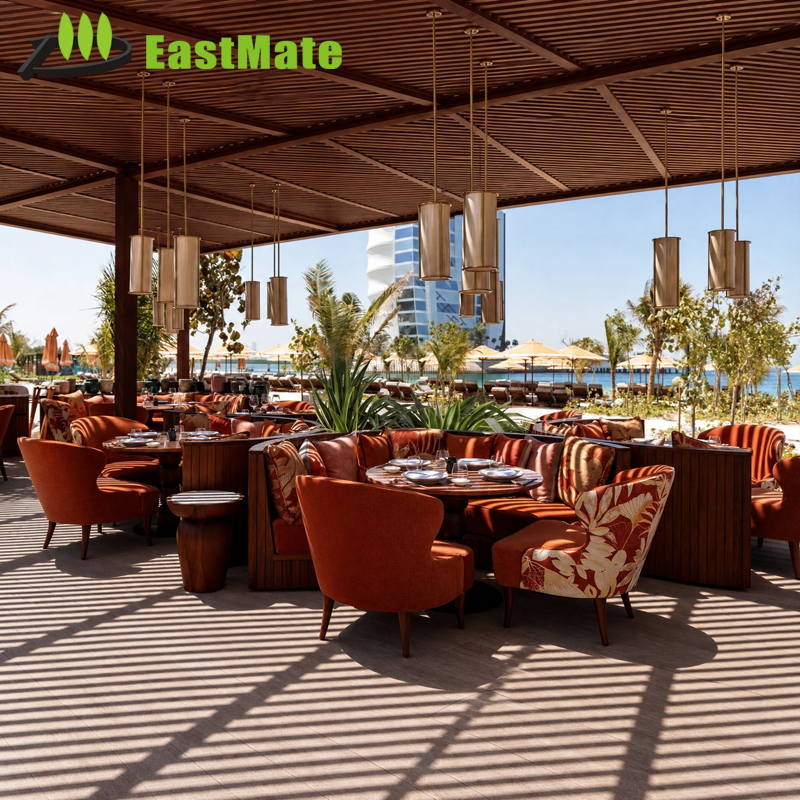
Solid Wood Round Dining Table Set 4-Seat Ensemble
Compact organic profile configured with radiused safety corners, suited for serviced residences, executive suites, and boutique resort verandas.
- Joints: Mortise & Tenon
- Substrate: Rubberwood
- Edge: Beveled 15mm
- Assembly: KD Structural
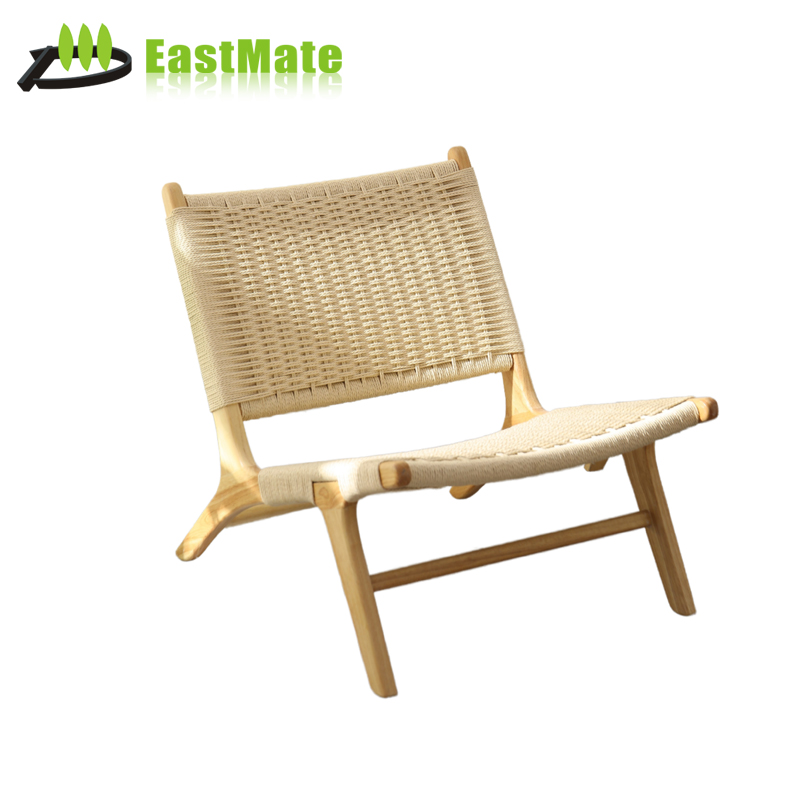
Nordic Reclining Solid Wood Lounge Chair & Table
Ergonomic angle support featuring open-pore polyurethane timber sealants and multi-density foam seating with 50,000-rub Martindale textiles.
- Frame: Steam-Bent Beech
- Fabric: Martindale >50k
- Fire Standard: CAL TB117
- Zone: Suite Lounge
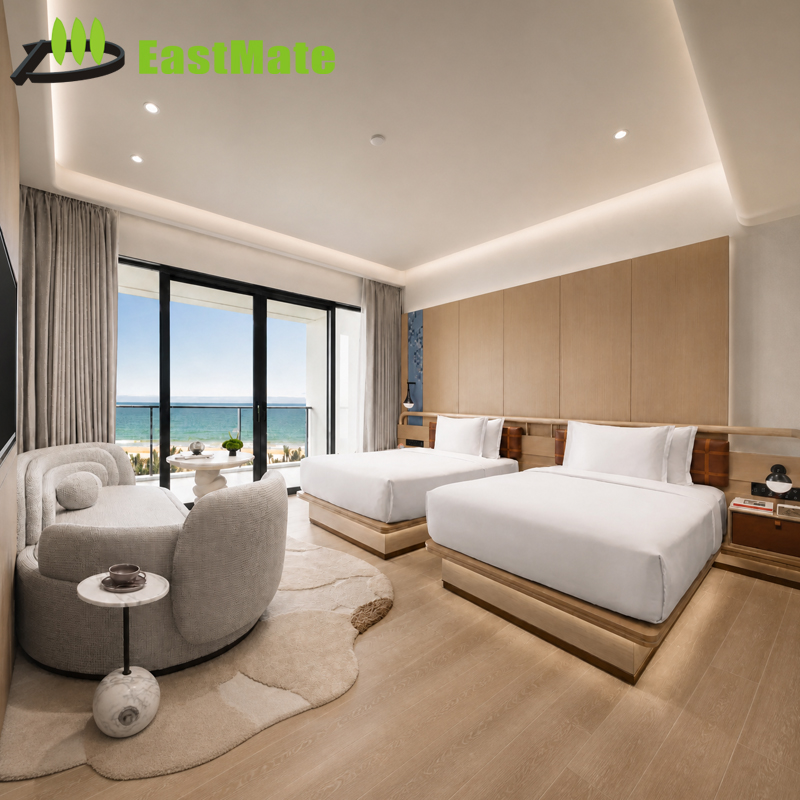
5-Star Luxury Modern Full Room Guestroom Package
Complete turn-key guestroom package including headboard joinery, wall panels, study desk, credenza, luggage rack, and LED architectural vanity.
- Scope: Full Keys Casegoods
- Wiring: CE/UL Pre-Routed
- Plinth: Recessed Stainless
- Custom: Complete OEM/ODM
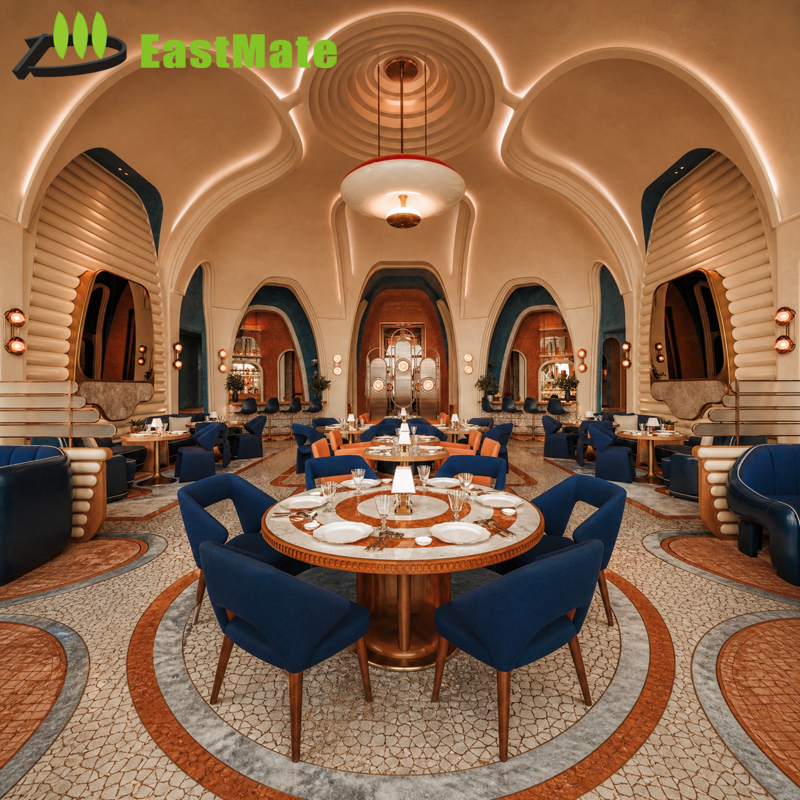
Modern Solid Wood 6-Seat Round Restaurant Dining
Spacious banquet layout with central structural pedestal to maximize leg room; reinforced apron and polyurethane topcoats prevent impact chips.
- Capacity: 6-Seat Commercial
- Pedestal: Cast Core + Wood
- Edge: Shock-Absorbent
- Compliance: EN 15372 Level 2
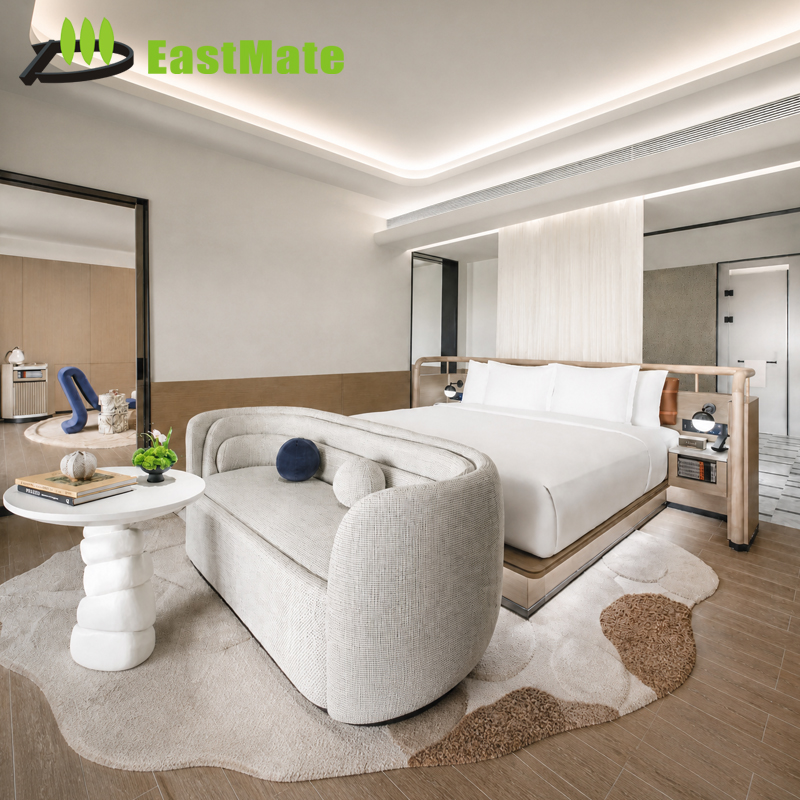
OEM/ODM Engineered Plywood Veneer King Bed Set
Built-to-spec casegoods leveraging CARB P2 compliant marine plywood cores, Quarter-sawn oak veneers, and concealed cable containment conduits.
- Substrate: CARB P2 Plywood
- Veneer: 0.6mm Hardwood
- Tolerances: ±0.5mm Precision
- Export: Sea-Freight Crating
Industrial Capacity & Quality Engineering Audited by SGS
Operating from Foshan, the epicenter of global furniture production, Foshan Hivke Hotel Furniture Co., Ltd. resolves the procurement friction between architectural design vision and large-scale industrial replication.
The Foshan Engineering Advantage
Unlike catalogue traders or broker agencies, our facility in Lecong Town, Foshan, acts as a dedicated production engine. We control raw material acclimation (kiln drying with equilibrium moisture content dialed between 8% and 12% to prevent cross-climate checking or warping), panel sizing via 5-axis CNC cutters, and high-pressure PUR hot-melt edge banding.
Every hospitality procurement schedule benefits from full-scale mock-up room verification before volume line launch. This operational milestone permits hotel owners, brand QA managers, and interior designers to audit edge reveals, wire runs, soft-close resistance, and tactile veneer quality under direct physical inspection.
Emerging Hospitality Furniture Procurement Trends
Procurement directors and FF&E consultants are steering capital expenditure beyond pure per-unit costs toward holistic lifecycle performance, localized material stewardship, and digital fabrication transparency.
Decarbonization & Circular LCA
Hoteliers are standardizing on FSC-certified timbers, E0/CARB P2 formaldehyde emission thresholds, and bio-based waterborne lacquer systems to achieve LEED v4.1 and BREEAM hospitality credits.
Integrated IoT & Invisible Power
Guestroom desks and nightstands now require concealed cable routing channels, Qi-certified inductive wireless charging matrices, flush architectural USB-C PD 65W sockets, and low-voltage indirect LED conduits.
Component-Level Serviceability
To reduce future operational CAPEX, leading operators mandate modular casegoods where high-wear components—such as bedside table tops, luggage rack bumpers, and armrest caps—can be replaced in under 15 minutes.
Multi-Functional Hybrid Zoning
Modern guestroom square footage demands dual-purpose furniture: credenzas that double as executive ergonomic desks, daybeds that transition into sleep surfaces, and compact mobile cocktail-work consoles.
Engineering Standards: Contract vs. Residential Specifications
Understanding why residential-grade furniture invariably fails within 12 months in commercial hotel applications. Our OEM manufacturing methods adhere to stringent heavy-contract hospitality metrics.
| Evaluation Parameter | Residential Retail Standard | Commercial 4/5-Star Contract Standard | Hivke OEM Quality Assurance Protocol |
|---|---|---|---|
| Substrate Integrity | Particle board or low-density fiberboard (LDF) | Moisture-resistant CARB P2 / E1 plywood or High-Density MDF | Cross-laminated calibrated hardwood multi-ply with zero delamination core |
| Veneer & Surface | Paper foil, 0.2mm rotary veneer, or thin paper laminates | 0.6mm slice-cut natural hardwood veneer or 1.0mm HPL | 0.6mm–0.8mm AAA-grade natural veneer with phenolic backing layer |
| Coating & Abrasion | Standard nitrocellulose (NC) lacquer, 1H hardness | Multi-stage Polyurethane (PU) / UV cured, 3H hardness | 5-coat automated UV/PU dust-free finish, heat & alcohol resistant |
| Upholstery Resilience | 15,000 to 25,000 Martindale double-rubs | >50,000 Martindale rubs; stain-repellent finish | 50,000–100,000 rubs with Crypton/Nanotex moisture-barrier backing |
| Fire Retardancy | Variable / non-regulated domestic foams | BS 5852 (Crib 5), CAL TB 117-2013, NFPA 260 | Certified combustion-modified high resilience (CMHR) foam and barrier interliners |
| Hardware & Slides | Stamped friction slides, 10,000 cycle lifespan | Full extension ball-bearing, 50,000 cycle lifespan | DTC / Blum concealed soft-close runners tested to 100,000 open/close cycles |
Systematic Value Engineering (VE)
We eliminate budget overruns without degrading architectural intent. Our engineers identify substrate adjustments, internal veneer balances, and optimized edge profiles that trim 12%–22% in FF&E cost while preserving the specified exterior aesthetic.
- Substrate rationalization based on moisture exposure
- Metal plating substitution to PVD titanium stainless steel
- Nesting optimization to maximize timber sheet yields
Full-Scale Mock-Up Room Prototyping
Before launching mass production for 200 to 1,000+ guestroom keys, we construct 1:1 scale mock-up rooms in our Foshan facility. Clients can inspect joinery reveals, cable routing, stability, and packaging durability on-site or via live video audit.
- Rapid 3–4 week mock-up turnaround
- Full shop-drawing sign-off package
- Destructive stress and drop testing validation
Export Crating & Room-by-Room Logistics
Damage during ocean transit and chaotic on-site sorting inflate soft contractor costs. We employ high-density EPE foam corner guards, 5-ply corrugated outer boxes, reinforced wooden skeleton crates, and clear room-by-room sequencing labels.
- Moisture-absorbing silica desiccants per crate
- Color-coded floor and room grouping systems
- Door-to-site DDP delivery clearance capabilities
Frequently Asked Questions by Purchasing Directors & Specifiers
Actionable answers addressing the technical, financial, and logistical bottlenecks encountered when sourcing bespoke hotel FF&E from China.
How do you guarantee timber dimensional stability across diverse climates?
We balance timber equilibrium moisture content (EMC) in our computerized drying kilns according to the destination market's psychrometric profile (typically 6%–9% for arid Middle Eastern destinations or heated North American interiors, and 10%–13% for tropical coastal regions). Substrates are sealed on all six faces—including concealed underside millwork—to prevent vapor intake and subsequent warping.
Can you manufacture precisely to brand guidelines like Marriott, Hilton, or Accor?
Yes. Our in-house technical detailing division regularly converts Brand FF&E manuals and interior designer tender books into shop drawings. We accommodate mandated requirements such as headboard blocking dimensions, tamper-resistant lighting brackets, commercial drawer glide weight ratings, and approved fire barrier fabrications.
What is the standard production timeline for a 200-key hotel package?
A standard 200-key guestroom manufacturing schedule typically follows this cadence: 1–2 weeks for technical shop drawings and finish board submittals; 3–4 weeks for mock-up room fabrication; and 35–45 calendar days for volume mass production following mock-up approval. Phased container dispatches can be scheduled to match the general contractor's floor handover milestones.
How do you handle fire safety and toxicity compliance for global jurisdictions?
We source certified fire-retardant foams and textiles conforming strictly to BS 5852 (Crib 5) for the UK/Europe, CAL TB 117-2013 and NFPA 260 for North America, and AS/NZS 1530 for Australasia. Flammability certificates, mill test logs, and third-party laboratory verification (SGS/TÜV) are provided with the initial pre-production material dossier.
What quality assurance protocols occur prior to container sealing?
Our internal Quality Assurance department operates a mandatory 5-stage checkpoint system: raw lumber moisture testing, CNC cutting dimension verification, dry-joint trial assembly, finish coat cross-hatch adhesion testing, and final load-bearing inspection. We provide high-definition inspection photo/video reports, and welcome client-appointed third-party inspectors prior to balance release.
Can you coordinate fixed architectural joinery alongside loose furniture?
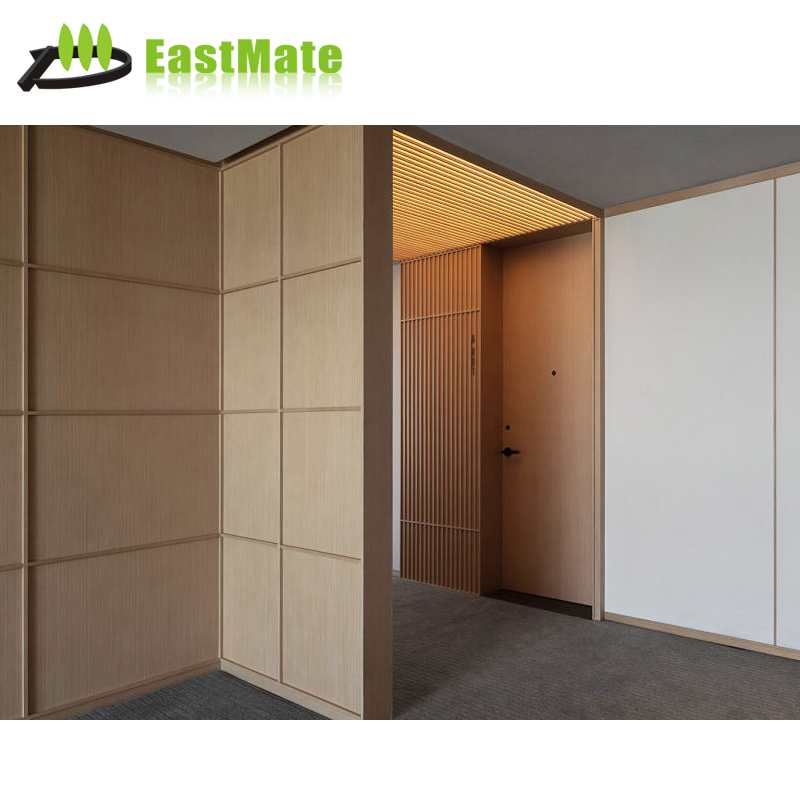
Yes. Providing both loose casegoods/seating and fixed architectural joinery (wall paneling, bathroom vanities, minibar niches, and entry door portals) from a unified production facility ensures absolute color harmony, grain-matching consistency across substrates, and synchronized shipping container logistics.
Request an Engineered Tender Review & Shop-Drawing Audit
Send your bill of quantities (BOQ), architectural renderings, or tender drawings. Our engineering team returns fully dissected shop-drawing estimates, value-engineering options, and freight forecasts within 48 hours.