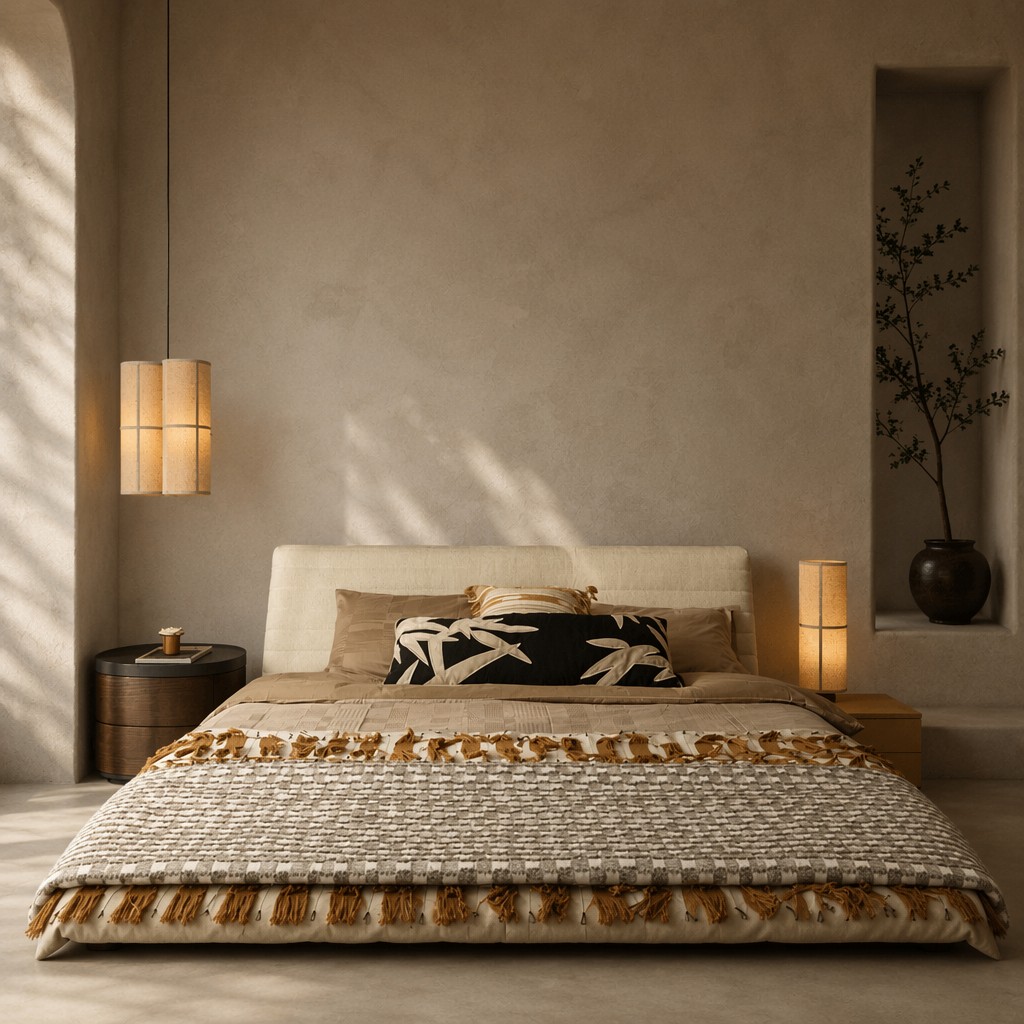
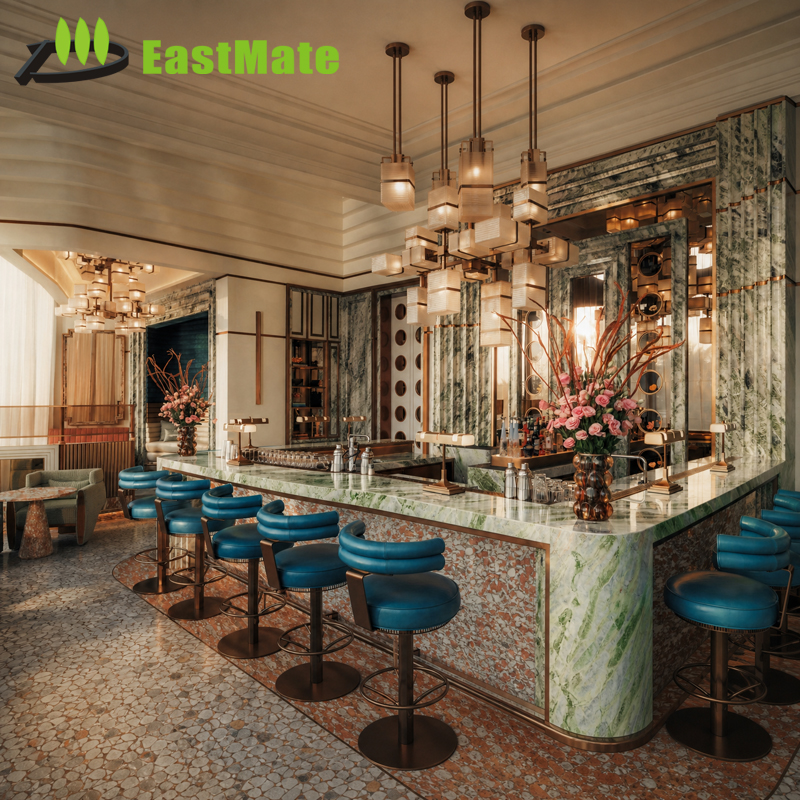
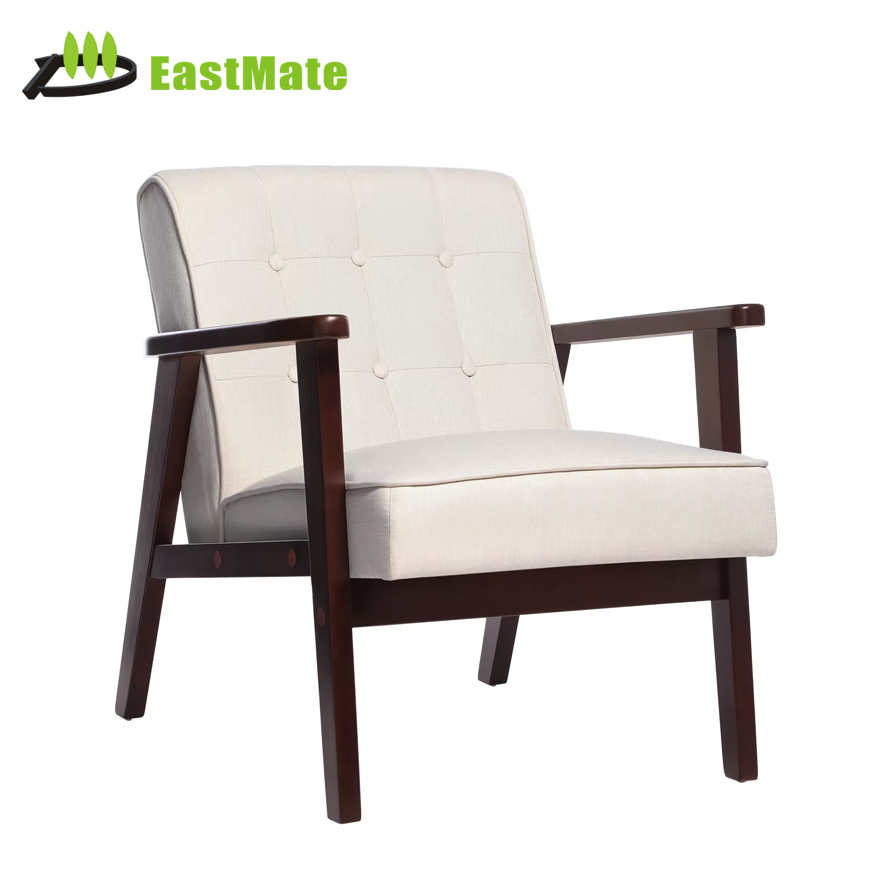
Engineered for high-traffic durability, structural rigidity, and seamless interior integration. Each piece conforms to international commercial testing standards including Martindale rub tests, BIFMA structural integrity, and local flame-retardant protocols.
Headquartered in Lecong, Foshan—the epicenter of global furniture manufacturing—Foshan Hivke Hotel Furniture Co., Ltd. bridges architectural design intent and industrial volume manufacturing through audited factory systems.
Contract hotel furniture diverges sharply from residential cabinetry. Commercial FF&E must endure severe environmental stresses, continuous operational loading, and rigorous housekeeping cycles while preserving aesthetic perfection across hundreds of guest keys.
Operating under strict ISO 9001 quality management systems, Hivke deploys an end-to-end technical control system. Before serial production commences, our engineering department converts schematic design drawings into full-scale structural shop drawings (1:1 joint detailing, thermal expansion gap calculations, cable conduit integration, and wall anchorage loads).
The Mock-Up Room (MUR) Imperative: We build complete pre-production prototypes and mock-up suites to test veneer book-matching, finish sheen consistency, structural deflection, and ergonomic clearances prior to mass release, mitigating client CapEx exposure.
Whether navigating high-humidity coastal resort specifications in the Maldives or stringent Class-A flame-retardant standards in North America and Western Europe, our production lines adhere strictly to client-designated standards including CARB Phase 2, E1-grade boards, and BS 5852 Crib 5 upholstery standards.
| Audit Parameter | Foshan Hivke Standards | Standard Factory Benchmark |
|---|---|---|
| Factory Audit Verification | SGS Onsite Verified & Documented | Self-Declared / Unaudited |
| Shop Drawing Engineering | In-house CAD/SolidWorks with CNC Linking | Outsourced Drafting or 2D sketches |
| Formaldehyde Standards | E1 / E0 / CARB Phase 2 compliant | Non-compliant E2/Standard boards |
| Hardware & Mechanics | DTC / Hafele / Blum (Cycle-Tested) | Unbranded domestic mechanisms |
| Packaging Standard | 5-layer export cartons + corner honeycomb + wood crates | Single layer corrugated wrap |
| Onsite Mock-up Protocol | 100% full-scale assembly prior to batch cutting | Direct production from schematics |
Insights into how international hotel operators, REITs, procurement agents, and architectural practices are restructuring supply chains to mitigate inflation, enhance ESG compliance, and shorten opening timelines.
Global labor shortages at construction sites have accelerated the demand for plug-and-play architectural joinery. Hospitality owners increasingly require wall paneling, headboard backings, and vanity units to be pre-machined with clip-lock French cleat mounting systems.
Scope 3 emission tracking under corporate ESG mandates is shifting supplier selection criteria. Procurement directors now prioritize suppliers capable of demonstrating chain of custody for every timber and chemical constituent.
Moving away from naive initial purchase price comparisons, Tier-1 hospitality groups focus on 7-to-10-year total cost of ownership (TCO). Value engineering now prioritizes edge durability and field-repairability.
Modern contract furniture merges artisanal woodworking with industrial metallurgy, composite chemistry, and seamless smart-room connectivity.
Critical answers for hospitality developers, procurement consultants, and interior architects managing complex overseas millwork and FF&E manufacturing.
We batch-procure natural wood veneers from uniform log flitches. Our veneer workshop conducts sequence matching (slip, book, or balance match) under standardized 5000K daylight inspection lamps. Both loose guestroom furniture and architectural wall paneling undergo unified finishing line passes to ensure absolute consistency in sheen, undertone, and UV resistance across all hotel zones.
We engineer custom builds to satisfy region-specific compliance regimes: BS 5852 (Crib 5) for the UK and Middle Eastern markets, CAL 117-2013 and NFPA 260 for the United States, and IMO FTP Code Part 8 for cruise ships and maritime hospitality. We supply independent SGS, TÜV, or Intertek batch testing certificates with every delivery.
A standard 200-key timeline is structured into clear risk-mitigated phases: Shop drawing development and material board approvals take 2 to 3 weeks; Mock-Up Room (MUR) fabrication takes 3 to 4 weeks; following MUR sign-off, full serial mass manufacturing runs 35 to 45 days. Phased containerized dispatch is customized to align with site crane and elevator availability schedules.
All timber components are kiln-dried to equilibrium moisture contents (8%–12% tailored to project destination climate). Packaging incorporates 5-layer heavy-gauge export corrugated cartons, thick high-density EPE foam profiles, corner guards, waterproof polyethylene wrapping, and continuous container desiccants to prevent container-rain moisture damage during ocean transit.
Submit your architectural drawings, interior schedule of finishes, or project Bill of Quantities (BOQ). Our senior hospitality estimating team will deliver comprehensive shop drawing analysis, material optimization suggestions, and a factory-direct commercial proposal within 48 business hours.