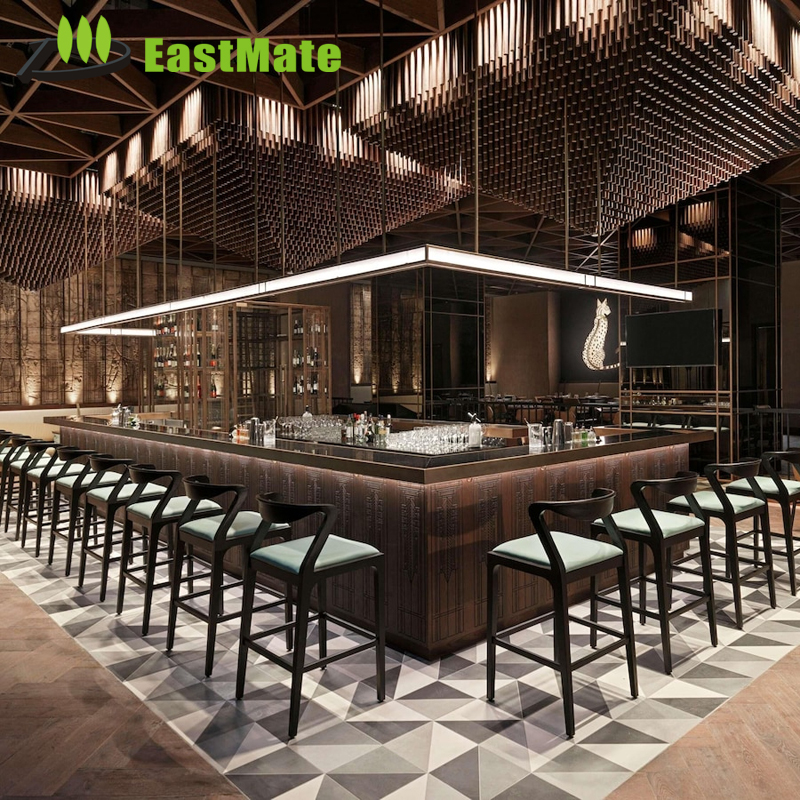
Lounge & Bar FF&E
Manufactured to rigid European safety directives and international hotel-brand FF&E guidelines, each suite configuration harmonizes natural timber veneers, E1/CARB P2 structural cores, commercial-grade hardware, and fire-rated contract upholstery.
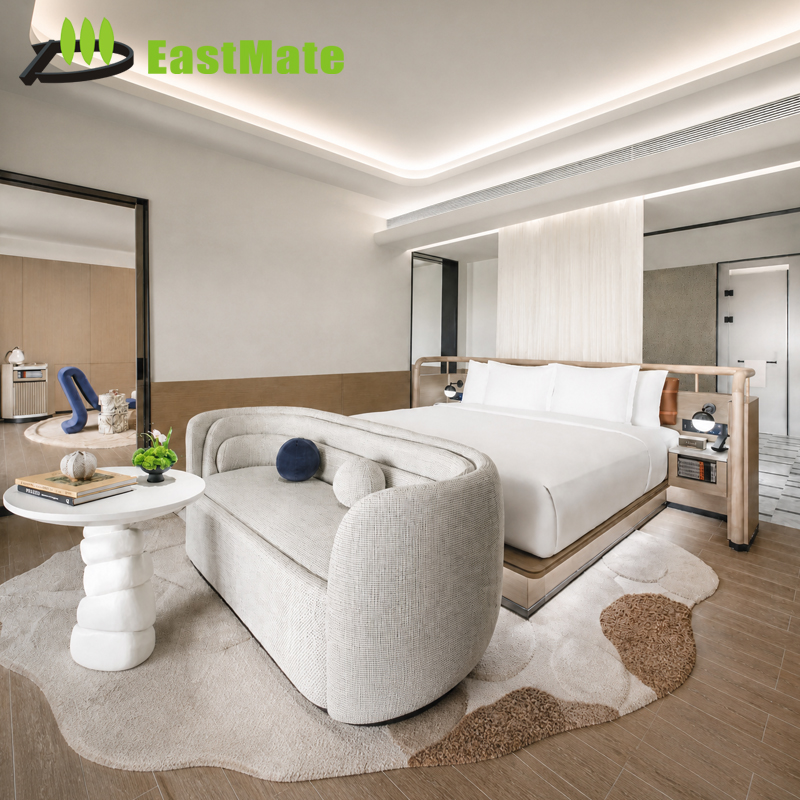
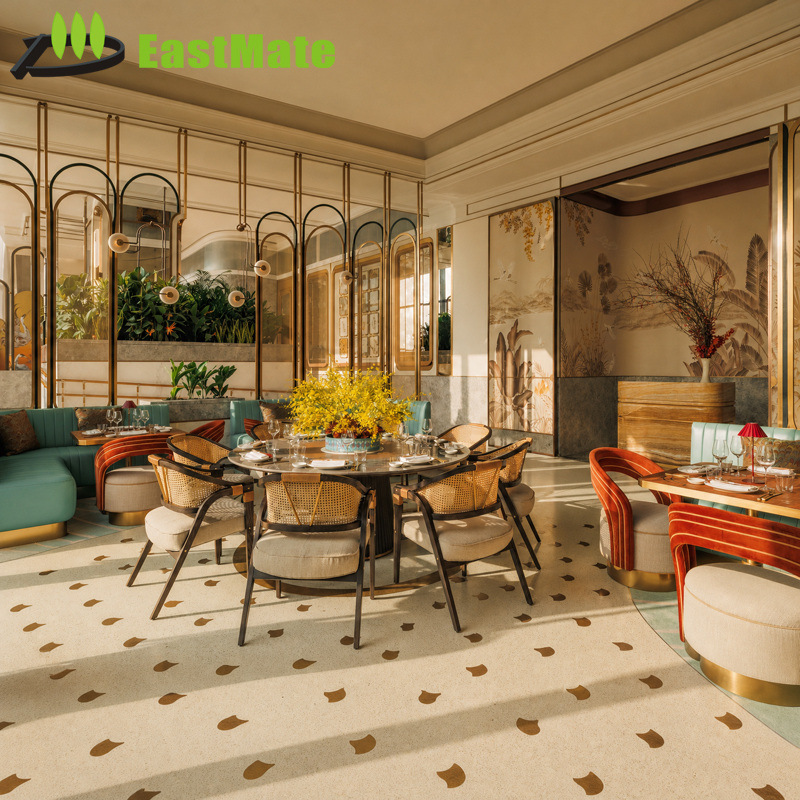
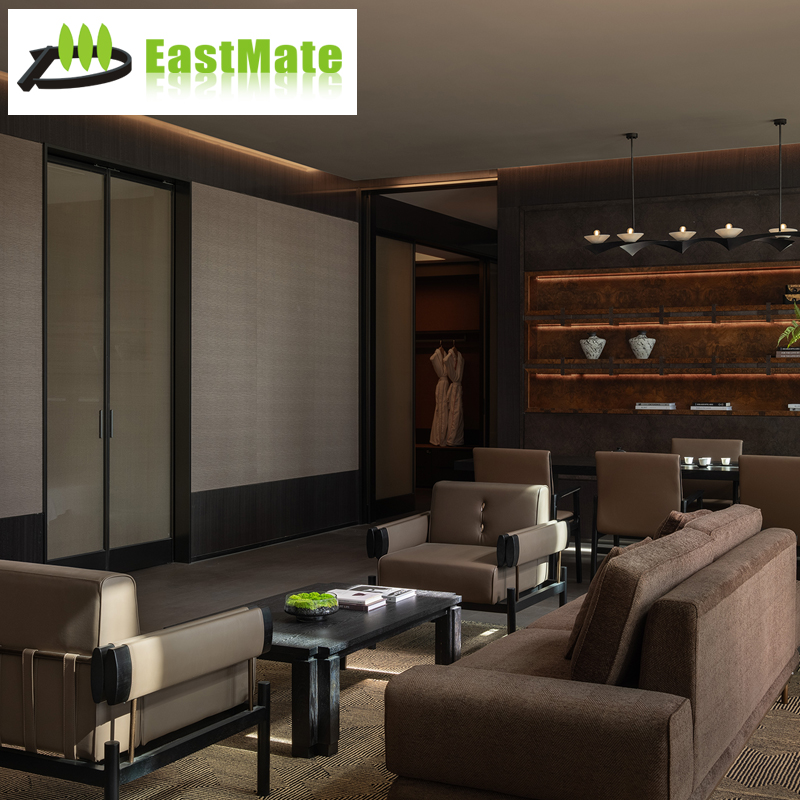
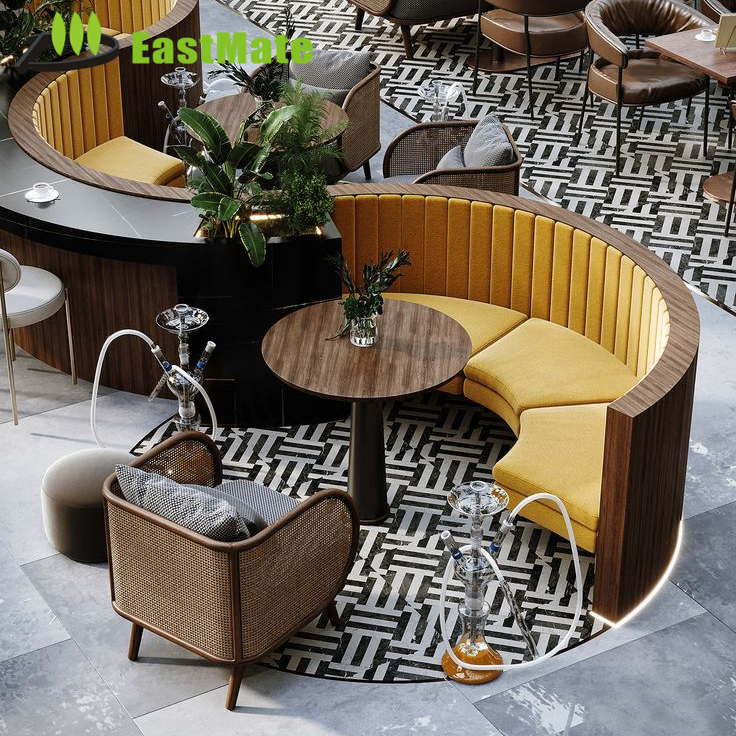
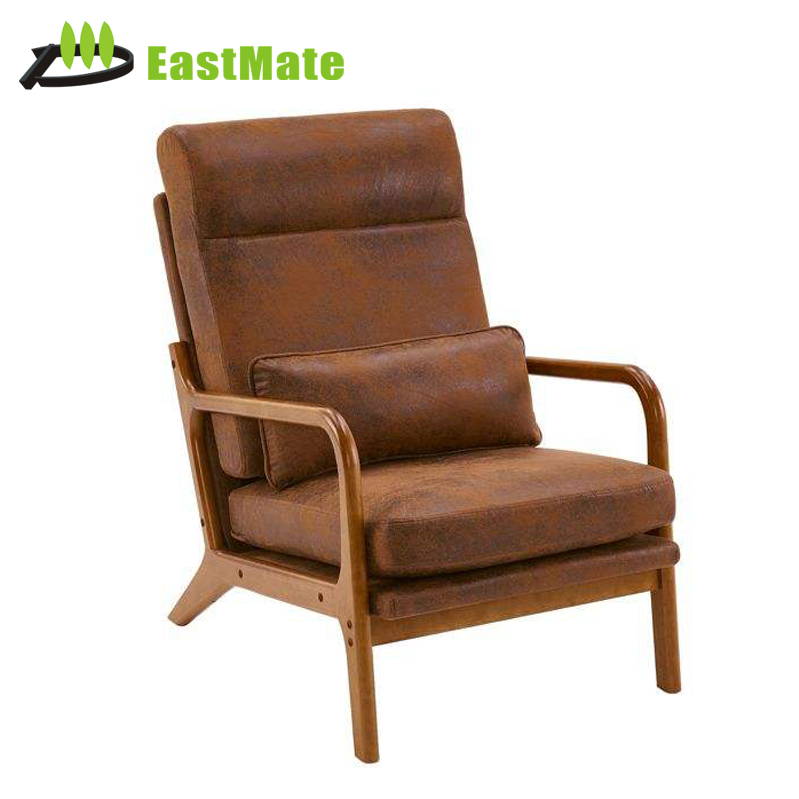
In modern contract hospitality procurement across the European Union, United Kingdom, and the Middle East, a "CE Certified Hotel Bedroom Suite" represents an umbrella compliance framework. It safeguards physical structural stability, electrical low-voltage safety for smart components, and low-VOC emissions under stringent European Harmonized Standards.
Contemporary bedroom headboard panels feature embedded reading lamps, inductive wireless charging pads, international multi-gang sockets, and LED linear coves. Each electrical element integrated into our casegoods holds individual CE marking under the Low Voltage Directive (LVD 2014/35/EU) and Electromagnetic Compatibility Directive (EMC 2014/30/EU), fully isolated via flame-retardant conduit channels.
Commercial hotel guestrooms sustain relentless cyclic loading far exceeding domestic tolerances. Our desks, luggage benches, nightstands, and bed plinths undergo cyclic static weight deflection, drop impact tests, and edge-shearing resistance in compliance with EN 15372 (Contract Non-Domestic Tables) Level 2 & Level 3, as well as EN 16139 Level 2 severe-use standards for lounge seating.
Interior fire propagation mitigation is compulsory for hospitality life safety. All upholstery assemblies, from headboard fluting to desk chairs, adhere strictly to British Standard BS 5852 (Crib 5), EN 1021-1/2, or US California Technical Bulletin 117-2013. Substrates conform to E1 and CARB Phase 2 formaldehyde limits (EN 717-1 emission chamber method ≤ 0.05 ppm).
Direct comparison of core components, testing standards, and millwork methodologies deployed across 4-star vs 5-star luxury hospitality schemes.
| Casegood Component | Structural Substrate | Surface Veneer & Finish | Safety / Structural Standard | CE & Environmental Status |
|---|---|---|---|---|
| Integrated Headboard Wall Panel | 18mm E1 Marine Grade Plywood + FR Backer | 0.6mm American Walnut / Quarter Cut Oak + 5-Coat PU Lacquer | EN 13501-1 Class B-s1, d0 / BS 5852 Crib 5 | CE LVD Certified Sockets |
| Floating Bed Base & Platform | Solid Russian Larch Internal Frame + Plywood Slats | High-Density FR Foam + Soil-Repellent Crypton Textile | Static Load ≥ 500kg / EN 1725 Bed Safety | FSC 100% Timber |
| Nightstands with Wireless Charging | Solid Ash Trim + High-Moisture MDF Core | Anti-Fingerprint Sintered Stone Inset Top (12mm) | EN 15372 Level 2 / Drop Ball Impact Test ≥ 1.2m | CE / Qi Certified Inductive Coil |
| Wardrobe & Minibar Credenza | Plywood Carcass + Aluminum Honeycomb Sliding Doors | Open-Pore Matte Veneer + Stainless Steel PVD Satin Accents | 100,000 Cycle Hinge & Soft-Close Runner Durability | CARB P2 & E1 Compliant |
| Executive Hospitality Desk & Vanity | E1 High-Density Moisture Resistant Core (HMR) | Solid Timber Hardwood Edging (5mm) + UV Cured Topcoat | EN 15372 Heavy Commercial / Alcohol & Heat Tested | CE Integrated Cable Spine |
| Lounge Armchair & Daybed | Kiln-Dried White Birch / Red Oak (MC 8% - 12%) | CMHR 45kg/m³ Foam Core + 100k Martindale Rub Fabric | EN 16139 Level 2 Extreme Contract Standard | OEKO-TEX Class 1 Textile |
As global hotel operators prioritize sustainability, agile brand rollouts, and accelerated return-on-investment, procurement dynamics are pivoting toward pre-engineered offsite assembly and circular lifecycle parameters.
Developers are eliminating wet trade delays by shifting from on-site joinery carpentry to pre-hung, factory-machined interlocking wall cleat systems (French cleat systems). Headboard wall surrounds, integrated entry wardrobes, and minibar niches arrive on site 100% finished with pre-channeled conduit pathways, slashing on-site room installation schedules by 40%.
Global brands like Marriott, Hilton, and Accor are integrating Environmental Product Declarations (EPD) into procurement RFPs. Modern bedroom suite designs now demand disassemblable components: replaceable fabric covers, detachable solid timber wear edges, and solvent-free bio-based adhesives that permit refurbishment rather than landfilling during scheduled PIPs (Property Improvement Plans).
Visible charging plugs and bulky power hubs are becoming obsolete. Next-generation guestroom suites embed sub-surface inductive resonance chargers directly below timber veneer desks, integrate low-voltage capacitive touch sensors into solid timber nightstand tops, and utilize acoustic fluted wood paneling with NRC (Noise Reduction Coefficient) ratings ≥ 0.65 to improve sleep hygiene.
Due to acidic cleaning chemical vulnerabilities and water-ring staining on traditional Calacatta or Carrara marble, 5-star properties are transitioning to 6mm to 12mm sintered stone surfaces. Sintered stone delivers heat resistance up to 1200°C, zero water absorption (0.02%), scratch hardness rating ≥ Mohs 7, and identical veining aesthetics without maintenance liabilities.
Post-pandemic housekeeping protocol demands upholstery fabrics treated with non-leaching zinc pyrithione or silver-ion antimicrobial barriers. These textiles withstand bleach sanitation wipe-downs without dye degradation, achieving Martindale wear resistance cycles in excess of 100,000 double rubs for heavy-traffic suite sofas and luggage benches.
To insulate projects from logistical bottlenecks, international developers partner directly with verified large-scale manufacturers centered in specialized clusters like Lecong, Foshan. Concentrated regional supply chains allow custom metal casting, stone cutting, veneer pressing, and testing to occur within a 20km radius, reducing production lead times from months to 30-45 days.
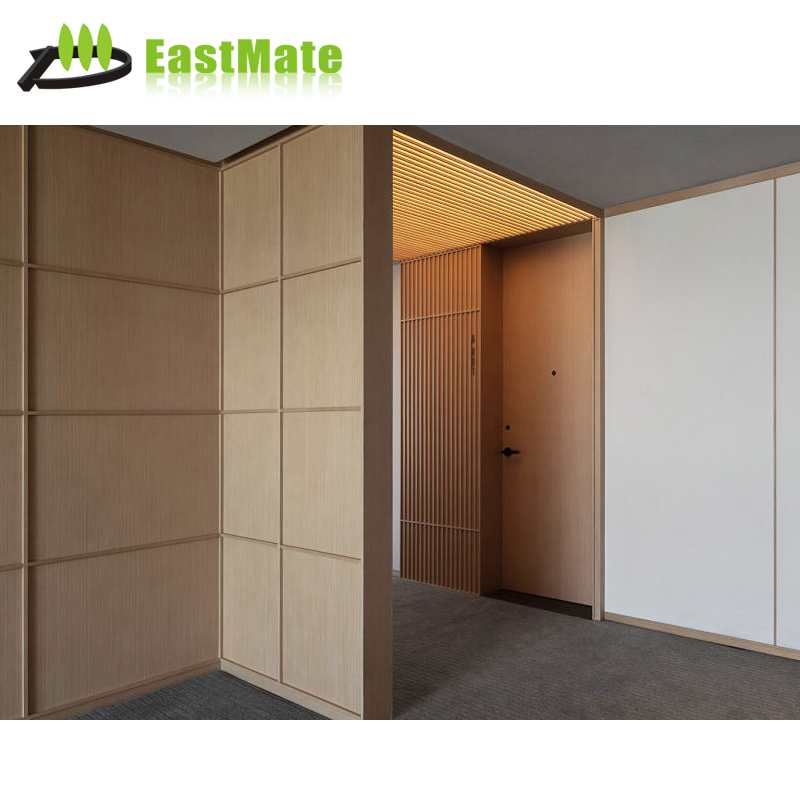
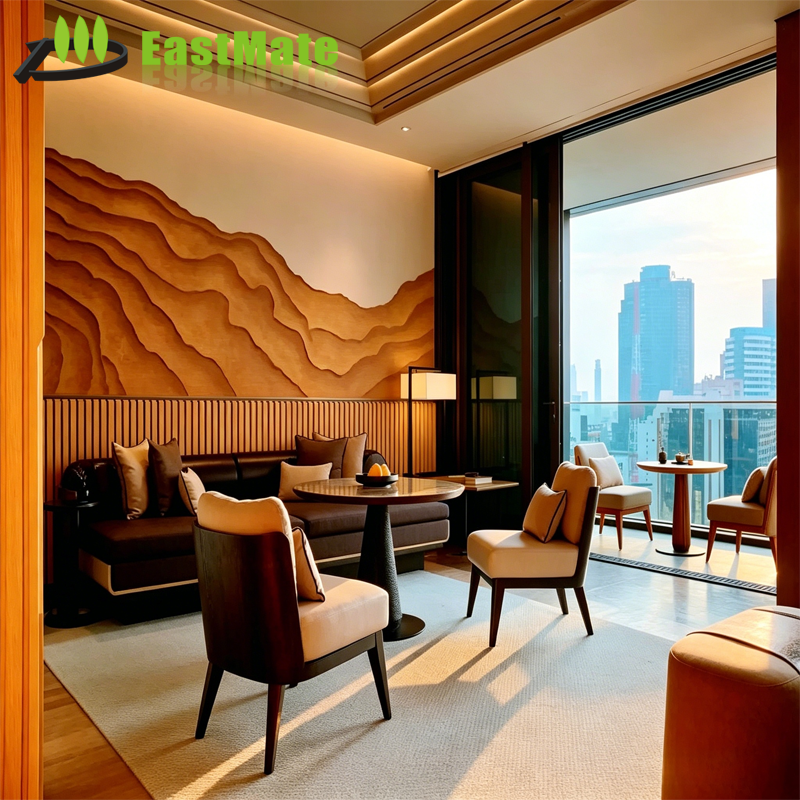
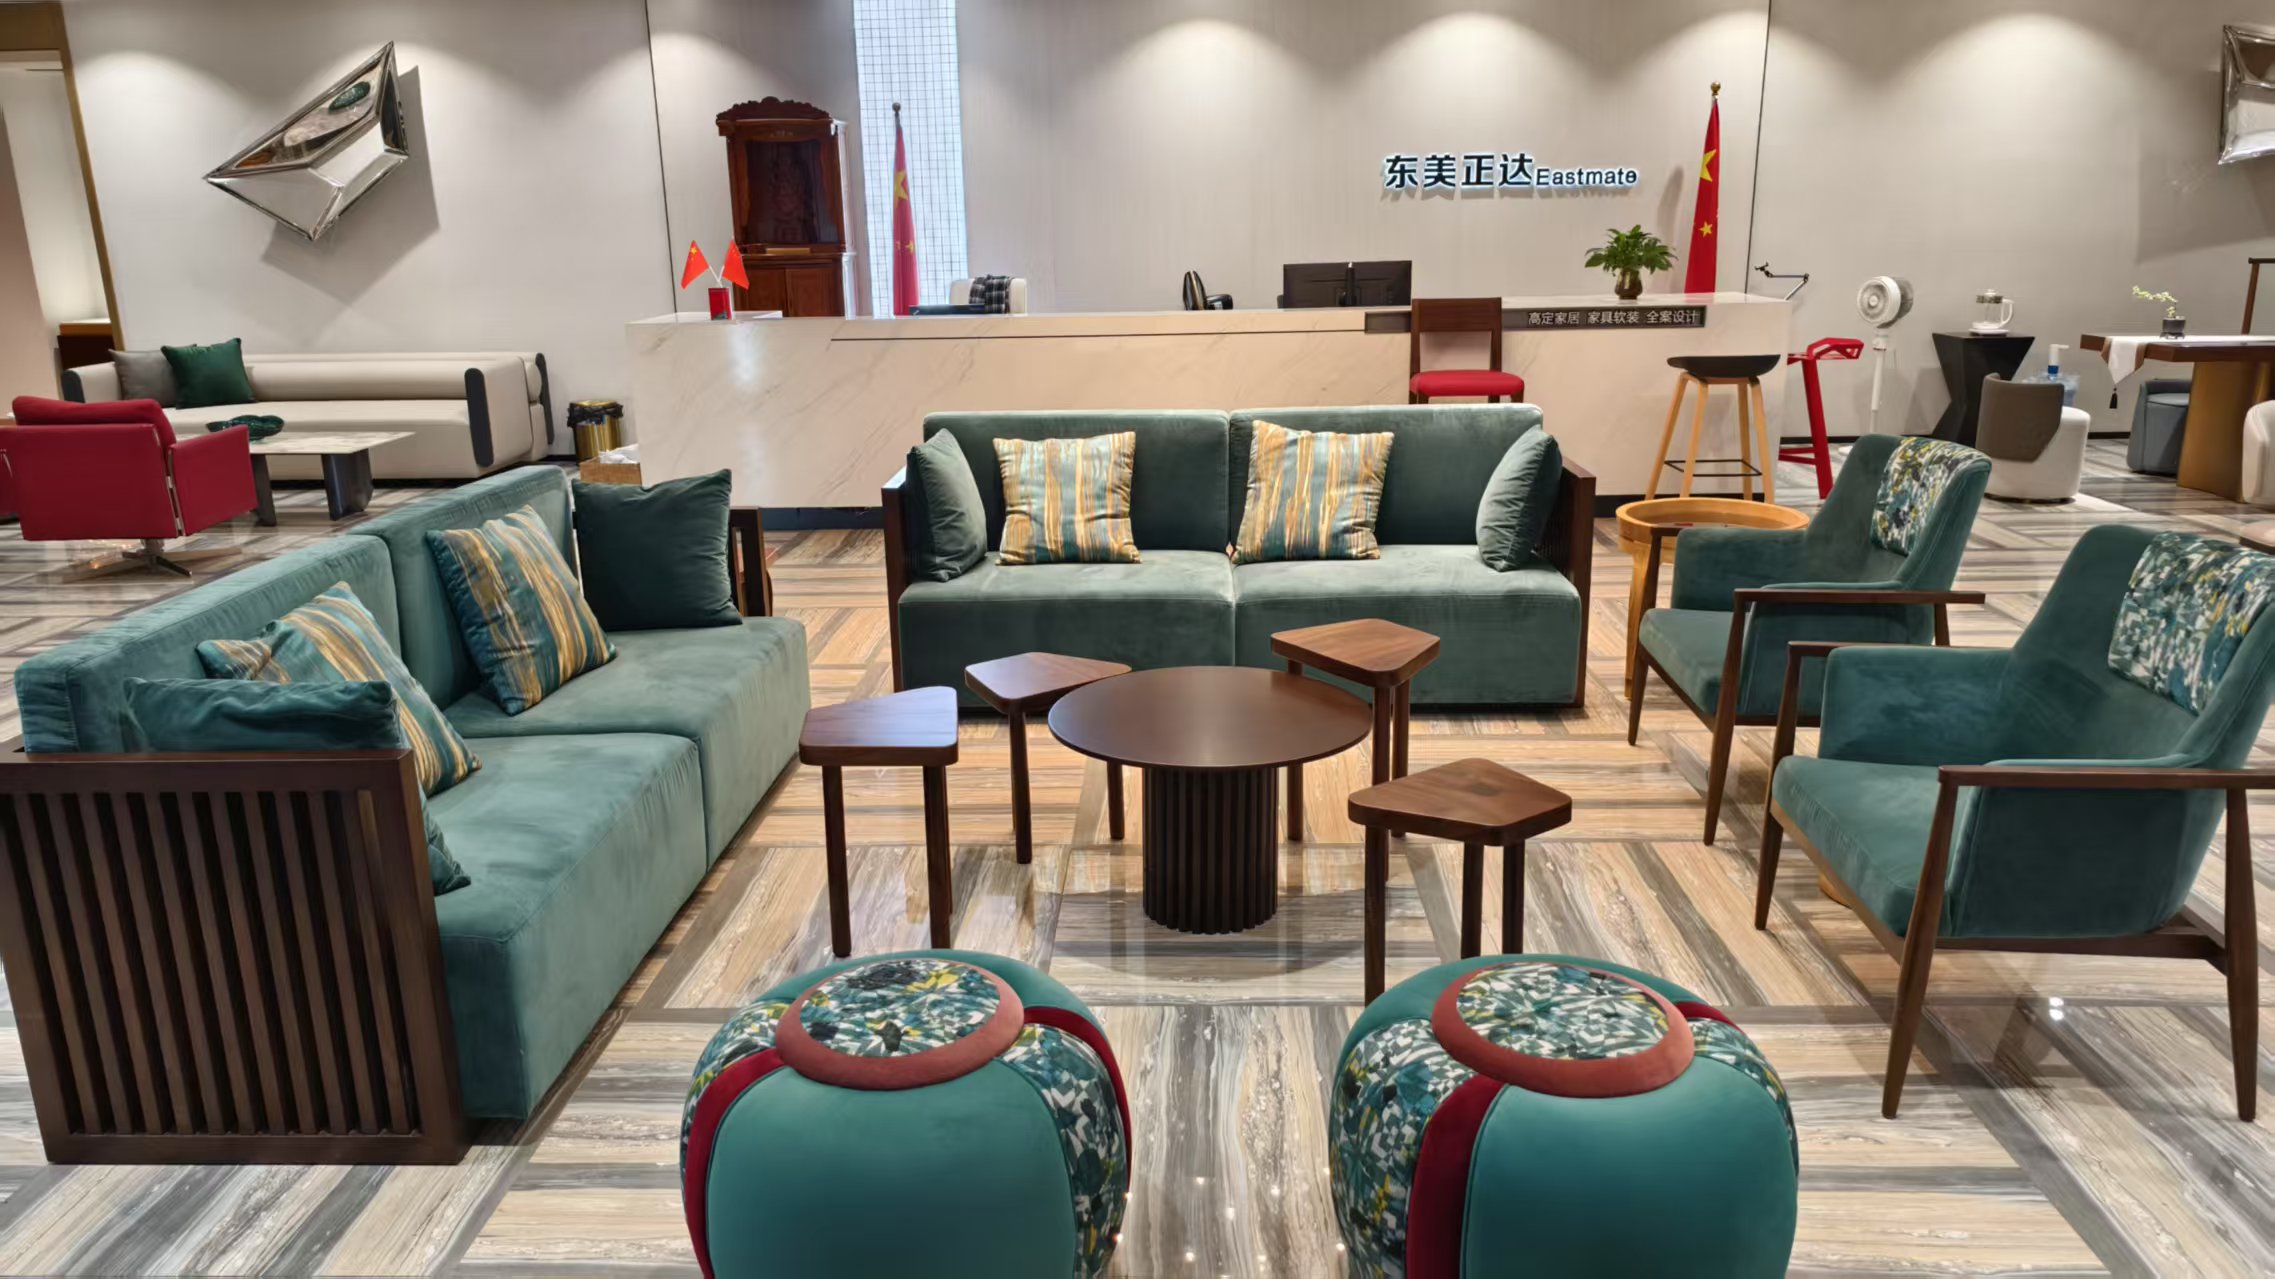
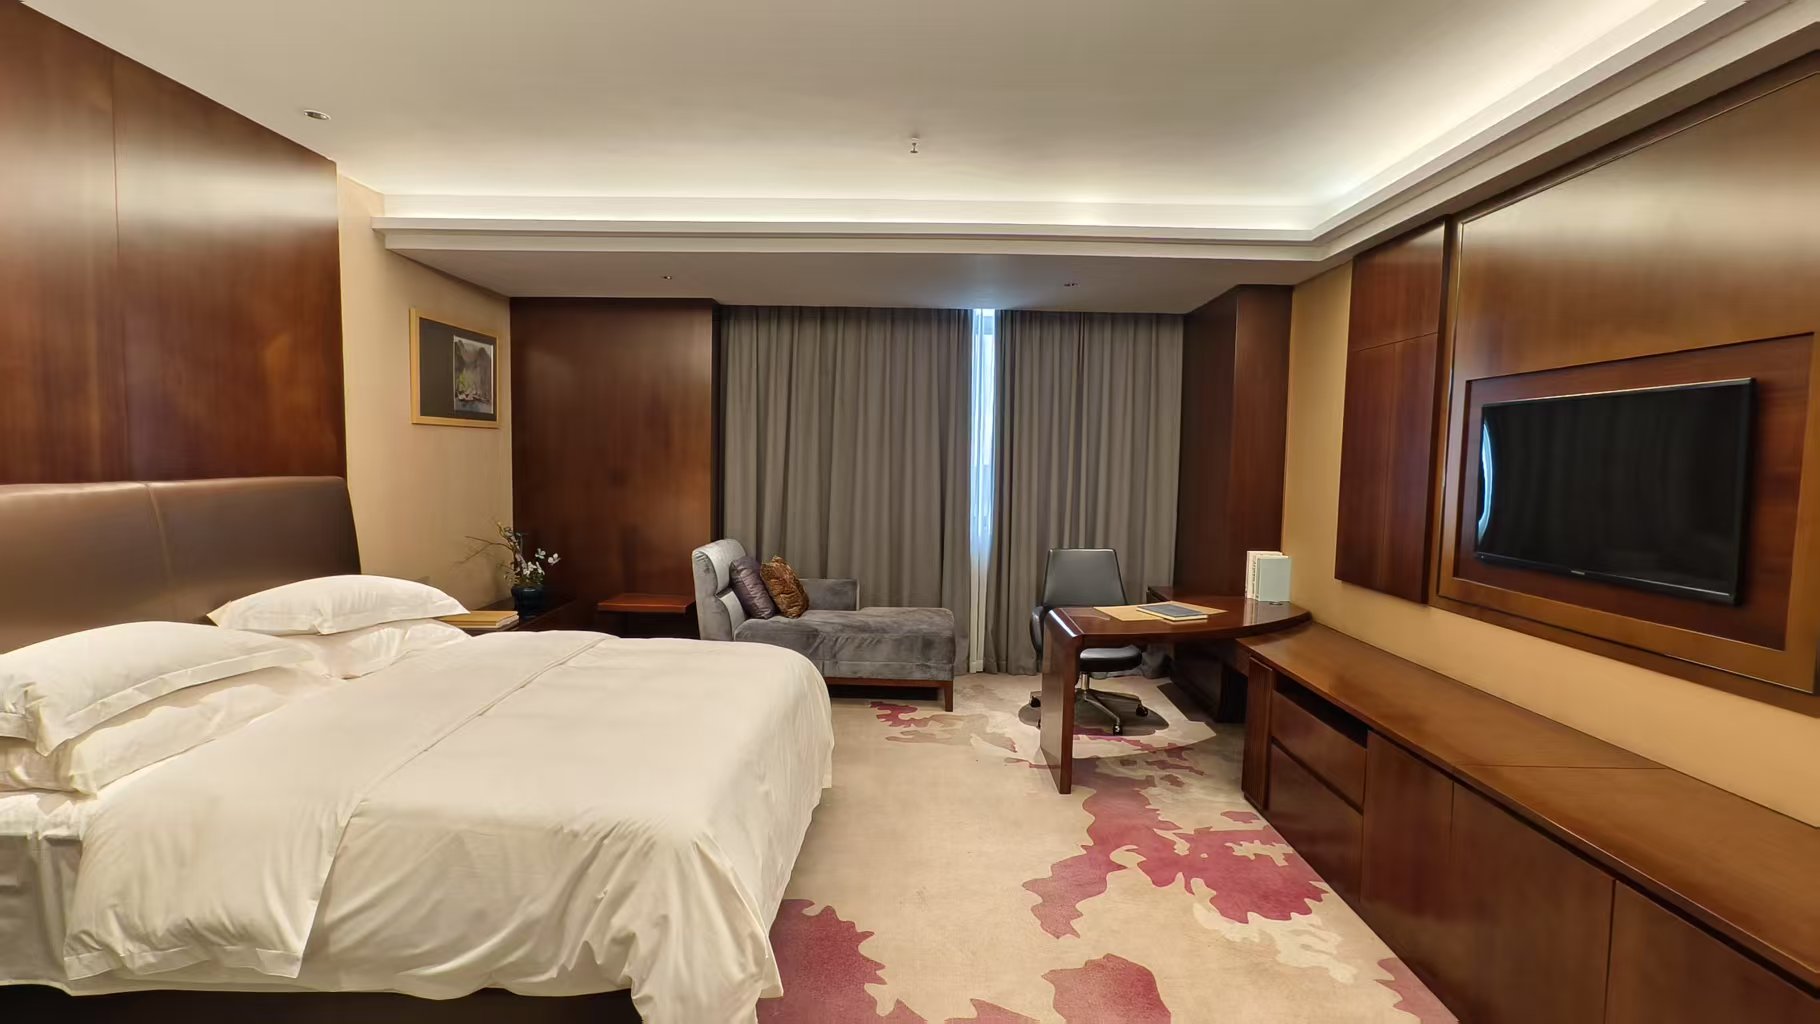
Headquartered in Lecong, Foshan—the epicenter of global furniture craftsmanship—Foshan Hivke Hotel Furniture Co., Ltd. operates as a tier-1 custom OEM/ODM hospitality furniture manufacturer. Spanning a third-party SGS-verified manufacturing footprint of 38,690 m² powered by 249 dedicated staff members, we bridge the gap between architectural conceptualization and industrial realization.
Unlike trading entities or catalogue resellers, our engineering departments take raw designer CAD/Revit files and translate them into millwork shop drawings down to 0.5mm tolerances. Our direct oversight over 80 assessed tier-1 raw material suppliers ensures uncompromising control over timber moisture content, hardware longevity, and finish luster across multi-thousand key portfolio rollouts.
A structured, stage-gate process engineered to mitigate dimensional variances, structural deficiencies, and shipping delays across multi-phase hospitality projects.
Our 28-member engineering drafting office converts ID schematics into comprehensive 2D/3D fabrication submittals with joint callouts, hardware schedules, and integrated service pathways within 7-10 business days.
Express courier submittal of physical sample submittal boxes: certified natural timber veneer flitches, custom liquid-metal coats, PVD metal swatches, stone samples, and BS 5852 flammability test coupons.
Construction of a physical prototype guestroom suite in our Foshan facility. Clients, procurement agents, and hotel brand QA directors conduct on-site or high-definition live video trial inspections.
State-of-the-art multi-axis CNC routing, precision edge banding with polyurethane (PUR) moisture-proof glues, dustless UV finish application, and continuous quality control checkpoints across every station.
Rigorous pre-assembly dry fitting, load deflection checking, gloss level sheen measurement (GU meter), and moisture content verification (maintained between 8% to 12% to prevent tropical swelling or arid cracking).
Heavy-duty 5-layer corrugated cartons, expanded polyethylene (EPE) corner shock bumpers, vacuum wrap, and solid timber ISPM 15 heat-treated export crates engineered for ocean container transits.
FOB, CIF, or DDP direct-to-site shipping coordination through major ports (Nansha, Yantian, Shekou) with phased dispatch plans timed to line up with general contractor floor handovers.
Numbered room-by-room hardware packs, detailed English installation manuals, step-by-step CAD exploded diagrams, and senior factory installation supervisors available on-site for international jobs.
Authoritative technical guidance for hospitality procurement executives, commercial interior designers, quantity surveyors, and project directors.
CE compliance for hospitality bedroom suites encompasses both physical furniture safety and integrated electrical assemblies. For the furniture itself, we manufacture and test our products to comply with harmonized European standards, including EN 15372 (strength, durability, and safety for non-domestic tables), EN 16139 (strength and safety for contract seating), and EN 1725 (stability and safety for domestic and commercial beds). For bedroom suites that incorporate lighting, USB/wireless charging stations, or motorized elements, each integrated electrical component carries individual CE marking conforming to the Low Voltage Directive (LVD 2014/35/EU) and Electromagnetic Compatibility Directive (EMC 2014/30/EU). We supply full Declarations of Conformity (DoC) and test reports from accredited testing bodies (such as SGS or TÜV) with every project documentation packet.
Moisture content discrepancies are the leading cause of veneer delamination, joint splitting, and panel warpage when furniture moves between continents. At Foshan Hivke, all kiln-dried solid hardwoods and composite substrates are conditioned inside climate-stabilized storage facilities. We maintain an equilibrium moisture content of 8% to 10% for arid destinations (such as the Middle East or inland North America) and 10% to 12% for humid or tropical climates (such as Southeast Asia, the Caribbean, or coastal Europe). Timber moisture levels are digitally tested and logged at the raw material intake, after CNC machining, and immediately before export packaging.
Yes. Over our 15+ years of dedicated hospitality manufacturing, we have engineered and produced casegoods and joinery packages matching the strict design and technical guidelines of major global hotel operators. We routinely review brand-specific FF&E design books, coordinate with nominated procurement agencies, and prepare complete mock-up submittals to ensure joinery profiles, edge-banding radii, hidden hardware brands (such as Blum, DTC, or Hafele), and electrical cutouts match brand criteria down to the millimeter.
We work with international flammability protocols tailored to the project destination. For the UK and Commonwealth regions, our contract foam and fabrics pass BS 5852 (Crib 5 test for seating and headboards) and BS 7176. For the North American market, our materials adhere to California Technical Bulletin 117-2013 (CAL 117) and NFPA 260. For architectural wall panels and fixed wooden joinery, we treat substrates with flame-retardant coatings meeting EN 13501-1 Class B-s1, d0 standards to curb flame spread and prevent toxic smoke generation.
Our standard production cycle is 30 to 45 business days starting from the formal sign-off of shop drawings and approved material finish samples. Prior to mass production, a physical 1:1 scale prototype mock-up room is built within 3 to 4 weeks for stakeholder inspection. In urgent phased renovation programs, we can stage manufacturing outputs by floor wings, dispatching sequenced containers to match the general contractor's handover timeline.
Transoceanic shipping exposes high-grade furniture to salt air, condensation, and temperature swings. We utilize a multi-layered barrier method: each furniture item is wrapped in non-scratch protective foam film, sealed in heavy-duty polyethylene moisture-barrier sheeting containing industrial desiccant silica packs, reinforced with 20mm edge and corner impact protectors, and packed into 5-ply double-wall export cartons. For delicate stone surfaces, mirrors, and long architectural panels, we build fumigated (ISPM 15 compliant) timber crating that locks the pieces in place during transit.
Foshan Hivke Hotel Furniture Co., Ltd. has undergone comprehensive on-site facility audits by SGS Group, verifying our plant scale (38,690 m²), workforce (249 full-time personnel), operational equipment, environmental control measures, and internal ISO 9001 quality management systems. Our suppliers for timber, veneers, paints, and adhesives undergo an 80-point audit matrix to maintain compliance with FSC forestry regulations and CARB P2 / E1 emissions.
We provide a comprehensive 3-to-5 year commercial contract warranty against structural joint failure, timber delamination, and hardware mechanical defects under normal commercial usage. In the rare event of transit damage or a manufacturing non-conformance, our project engineers furnish immediate replacement components via express air freight or credit the cost into the project reserve, minimizing punch-list friction during soft openings.
Send our senior engineering team your FF&E schedule, concept drawings, or architectural design deck. We will review joinery detailing, prepare value-engineered budget options, and supply free material sample packs for your next hospitality opening or renovation.